Steel Silo Laser Cutting Process | Manxing EPC Silo Solutions
Steel Silo Laser Cutting Process: Precision Engineering for Bulk Storage Construction
Laser cutting is a CNC-based thermal process that uses a focused high-power density beam to sever steel plates with kerf widths as narrow as 0.2 mm, achieving dimensional tolerances of ±0.1 mm. For steel silo fabrication, this technology delivers burr-free edges on wall panels, roof components, hopper cones, and stiffener rings, eliminating secondary machining and accelerating EPC project timelines by up to 40% compared to plasma or flame cutting.
1. Fundamentals of Laser Cutting Technology for Steel Silos
Figure 1Figure 2Figure 3
1.1 Fiber Laser vs. CO₂ Laser Systems
Fiber laser sources operating at 1064 nm wavelength have become the standard for silo steel cutting. A 6 kW fiber laser cuts mild carbon steel (Q235B) up to 20 mm thickness at speeds of 3.5 m/min, while a 12 kW unit handles 30 mm plates at 1.8 m/min. CO₂ lasers, though capable of smoother edge finishes on thick sections, consume 3× more electrical power and require mirror alignment maintenance, making fiber systems the preferred choice for high-volume silo component production.
1.2 Beam Delivery and Focus Optics
The cutting head uses a collimated beam focused through a 125 mm or 200 mm focal length lens to a spot diameter of 0.1–0.3 mm. Assist gas selection determines edge quality: oxygen cutting produces an oxidized edge suitable for welded silo seams, while nitrogen cutting yields a bright, oxide-free surface ideal for galvanized or painted components. Nozzle standoff distance is maintained at 0.5–1.5 mm via capacitive height sensing with a repeatability of ±0.05 mm.
1.3 CNC Motion Platforms
Gantry-style CNC tables with 6 m × 20 m cutting areas accommodate full-width silo wall panels in single passes. Servo-driven axes achieve positioning accuracy of ±0.03 mm and acceleration rates of 1.5 g, enabling intricate contour cutting for manhole flanges, ladder brackets, and bolt-hole patterns without repositioning the plate.
2. Material Selection and Preparation
2.1 Steel Grades for Silo Fabrication
Hot-rolled carbon steel plates (Q235B, Q345B) in thicknesses of 2–36 mm constitute the primary material. For grain silos requiring corrosion resistance, S355J2+N structural steel or DX51D+Z galvanized sheets (Z275 coating, 275 g/m² zinc mass) are specified. Laser cutting compatibility requires surface rust scale below Sa 2.5 cleanliness; oil films exceeding 2 g/m² cause inconsistent kerf penetration and dross adhesion.
2.2 Plate Flatness and Loading
Incoming plates must exhibit flatness deviation below 3 mm/m. Automated vacuum suction tables with 256 independent zones hold 12 m × 3 m sheets flat within ±0.3 mm during cutting. Pallet changers enable continuous operation: while one plate is being cut, the operator loads the next, reducing idle time to under 45 seconds per cycle.
2.3 Surface Pre-Treatment
Shot blasting to Sa 2.5 (ISO 8501-1) removes mill scale and provides an anchor profile of 40–80 µm for subsequent coating adhesion. For galvanized sheets, a laser-specific anti-spatter coating (8–12 µm dry film) prevents zinc vapor from contaminating the protective lens, extending consumable life by 60%.
3. Cutting Parameters and Quality Control
3.1 Parameter Optimization by Thickness
For a 6 mm Q235B wall panel, optimal settings are 4 kW power, 6.0 m/min speed, 1.5 bar nitrogen pressure, and 0.3 mm focal position below the surface. A 16 mm stiffener ring requires 8 kW, 2.2 m/min, 8 bar oxygen pressure, and 4 mm focal depth. Deviation beyond ±10% of these values results in dross heights exceeding 0.5 mm, requiring manual grinding.
3.2 Edge Quality Metrics
Per ISO 9013, laser-cut edges for silo components must achieve roughness Ra ≤ 12 µm in quality class 2. Squareness tolerance (u) must remain under 0.15 mm for plates up to 20 mm thick. Automated optical inspection systems using 5 MP line-scan cameras measure kerf width, perpendicularity, and dross presence at 300 mm/s scan speed, rejecting non-conforming parts before they enter the welding bay.
3.3 Thermal Distortion Management
Heat input during cutting induces residual stresses that cause bowing in panels wider than 2 m. Nesting algorithms sequence cuts from the center outward, distributing thermal load symmetrically. Micro-joints (0.3 mm uncut bridges at 500 mm intervals) hold nested parts in place until final separation, preventing individual pieces from shifting and maintaining positional accuracy within ±0.2 mm.
Pro Tip: For silo wall panels exceeding 10 m in length, program a 2 mm lead-in and 3 mm lead-out at each cut start/stop point. This prevents the characteristic "striation mark" at the initiation zone, ensuring uniform edge quality across the full panel length and reducing post-cut grinding time by 70%.
4. Post-Cutting Processing and Edge Quality
4.1 Deburring and Edge Rounding
Automated rotary brush deburring stations process cut panels at 2 m/min, removing micro-burrs up to 0.3 mm height and creating a 0.2–0.5 mm edge radius. This step is critical for silo wall panels that will be field-bolted, as sharp edges damage gasket seals and create stress concentration points under wind loading.
4.2 Dimensional Verification
Coordinate measuring machines (CMMs) with 3D laser scanners verify critical dimensions: bolt-hole pitch (±0.5 mm), flange flatness (±1.0 mm over 1 m), and overall panel length (±2.0 mm for 12 m panels). Statistical process control charts track CpK values; a CpK ≥ 1.33 indicates the cutting process is capable and stable for production runs exceeding 200 panels.
4.3 Surface Protection After Cutting
Freshly cut edges oxidize within 48 hours in humid environments. Immediate application of a 20 µm wash primer (two-component epoxy) on cut edges prevents flash rust before the panel enters the main coating line. For galvanized components, zinc-rich paint (80 µm DFT, 75% zinc content by weight) restores corrosion protection at thermally affected zones.
5. Integration with Silo Manufacturing Workflow
5.1 Nesting and Material Yield
Advanced nesting software (e.g., ProNest, SigmaNEST) achieves material utilization rates of 92–96% for silo wall panel layouts. For a 50,000-ton grain silo requiring 850 tons of steel, optimized nesting saves 40–60 tons of plate compared to manual layout, representing a cost reduction of $30,000–$45,000 at current steel prices.
5.2 Automated Part Sorting
Robotic pick-and-place systems with vacuum end-effectors sort cut parts into kit sequences matching the assembly order. Each part is laser-marked with a QR code containing project ID, panel number, and welding procedure specification, enabling full traceability from raw plate to erected silo.
5.3 Welding Preparation
Laser-cut edges with nitrogen assist gas require no groove preparation for butt joints up to 12 mm thickness. For thicker stiffener-to-wall connections, a 60° V-groove is laser-cut directly at the specified angle, eliminating separate beveling operations. Fit-up gaps controlled within ±0.3 mm ensure consistent weld penetration and reduce filler metal consumption by 15%.
6. Quality Standards and Inspection Protocols
6.1 Applicable Standards
Silo laser cutting operations comply with EN 1090-2 (Execution of steel structures), ISO 9013 (Thermal cutting classification), and AWS D1.1 welding pre-qualification requirements. For food-grade silos, FDA 21 CFR 177.2600 and EC 1935/2004 mandate that cut edges be free of burrs and sharp projections that could harbor bacteria.
6.2 In-Process Monitoring
Plasma sensors in the cutting head monitor back-reflected light intensity; a 15% drop signals lens contamination or nozzle wear, triggering automatic replacement. Power meters at the fiber output verify laser power stability within ±1% over 8-hour shifts, ensuring consistent kerf width across production batches.
6.3 Documentation and Traceability
Each cutting program generates a digital log recording power, speed, gas pressure, and focus position at 100 ms intervals. These records are archived for 10 years, supporting warranty claims and regulatory audits. Material certificates (EN 10204 Type 3.1) are linked to each plate heat number via the QR marking system.
Case Study: 100,000-Ton Soybean Silo Project
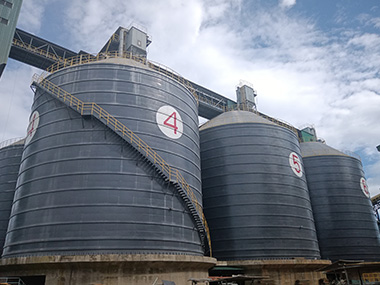
A South American grain terminal required twelve 100,000-ton capacity soybean silos, each 42 m diameter × 38 m height, fabricated from 4–25 mm Q345B plates totaling 2,400 tons. The EPC contractor deployed two 12 kW fiber laser cutting systems with 8 m × 24 m cutting tables. Nesting optimization achieved 94.7% material yield, saving 127 tons of steel ($95,000). Cutting cycle time per silo averaged 18 days versus 32 days with plasma cutting. Edge roughness averaged Ra 8.5 µm, eliminating the need for edge milling on all 14,600 panels. The project was completed 45 days ahead of schedule, with zero rework on dimensional non-conformances.
Frequently Asked Questions
Q1: What is the maximum steel plate thickness that laser cutting can handle for silo components?