Pressure Relief Valve Sizing for Pneumatic Conveying Silos: A Complete Engineering Guide
Proper pressure relief valve sizing for pneumatic conveying silos prevents catastrophic overpressure during bulk material filling. The relief valve must discharge at least the maximum pneumatic inlet gas flow rate, and the set pressure must remain below the silo's maximum allowable working pressure (MAWP) with appropriate accumulation margins. This article provides the engineering methodology, calculation steps, and practical considerations for correct relief valve specification.
1. Why Pressure Relief Is Critical for Pneumatic Conveying Silos
Figure 1Figure 2Figure 3
1.1 Overpressure Scenarios in Pneumatic Filling
Pneumatic conveying delivers material to silos using compressed air or nitrogen at typical pressures of 0.2–0.6 MPa. If the silo's vent filter becomes blinded or blocked, incoming gas accumulates faster than it escapes. Pressure can rise from normal operating levels (0–10 kPa gauge) to the silo's structural limit (typically 25–50 kPa for bolted steel silos, up to 100 kPa for welded designs) within seconds. A blocked discharge rotary valve or a malfunctioning level indicator triggering overfilling compounds this risk by reducing available vapor space.
1.2 Consequences of Inadequate Relief
Undersized or absent relief devices lead to silo roof blowout, wall panel buckling, or catastrophic shell failure. Industry incident data indicate that overpressure events in storage silos occur primarily during pneumatic filling operations, with repair costs ranging from $15,000 for panel replacement to over $500,000 for full structural rebuilds. Regulatory standards (EN 14491, NFPA 68, ATEX Directive 2014/34/EU) mandate explosion and overpressure protection on all enclosed silos receiving pneumatically conveyed materials.
2. Key Parameters for Relief Valve Sizing
2.1 Required Relief Flow Rate
The minimum relief capacity must equal or exceed the maximum volumetric gas flow entering the silo during conveying. For a pneumatic compressor delivering 10 m³/min FAD (free air delivery) at 0.5 MPa gauge, the expanded volume at silo pressure (approximately atmospheric plus back-pressure) is roughly 60 m³/min. This value forms the baseline for valve sizing. Always use the compressor's maximum rated flow, not the average conveying rate, and account for potential nitrogen inerting systems that may add supplementary gas volume.
2.2 Set Pressure and Accumulation
The relief valve set pressure should be set at or below the silo MAWP. For typical bolted carbon steel silos, MAWP ranges from 20 to 25 kPa gauge. Allowable accumulation is typically 10% above MAWP for single relief device installations (per ASME Section VIII and EN 14491). This means a silo rated at 25 kPa MAWP can tolerate up to 27.5 kPa before the valve must be fully open and discharging. The valve's full-open pressure must not exceed the silo's hydrostatic test pressure or structural yield limit.
2.3 Two-Phase Flow Considerations
During overpressure events, the discharge stream often contains entrained solid particles (two-phase flow). Pure gas-flow orifice calculations underestimate required area by 30–60% when significant dust loading is present. For silos storing fine powders (d₅₀ < 100 μm) at high filling rates, apply a two-phase flow correction factor (K_dust) of 0.5–0.7 to the discharge coefficient, or use the DIERS methodology for reactive or dust-laden systems. Particle concentrations exceeding 200 g/m³ in the vent stream necessitate dedicated two-phase sizing per EN 14491 Annex C.
3. Sizing Methodology: Step-by-Step Calculation
3.1 Step 1 – Determine Maximum Inlet Gas Flow
Obtain the compressor or blower performance curve. Identify the maximum free air delivery (Q_air) at the highest operating pressure. Convert to actual volumetric flow at relief conditions using the ideal gas law:
Use the standard compressible flow orifice equation for gas relief:
A = (Q_relief × √(M / (Z × T))) / (C × K_d × P_set × K_b)
Where: A = orifice area (mm²), M = molecular weight (28.97 for air), Z = compressibility factor (~1.0 at low pressure), T = temperature (K), C = coefficient of discharge (0.6–0.7 for spring-loaded valves), K_d = effective discharge coefficient, P_set = set pressure (kPa abs), Kb = back-pressure correction factor. For the example above with air at 20°C, P_set = 126.3 kPa abs, C × K_d = 0.42: A ≈ 1,850 mm² corresponds to a DN 80 (3-inch) relief valve minimum.
3.3 Step 3 – Verify Discharge Line Capacity
The discharge piping from the relief valve outlet must not create back-pressure exceeding the valve's rated capacity. For spring-loaded valves, built-up back-pressure should remain below 10% of set pressure to prevent chatter and capacity reduction. Keep discharge lines short (≤ 3 m), avoid elbows where possible, and size the outlet pipe at least one pipe size larger than the valve outlet. For silos located indoors, route discharge to exterior safe areas with a minimum 3 m clearance from personnel access points.
🔧 Engineering Tip: Always size the relief valve for the maximum possible gas inflow, not the steady-state conveying rate. A standby compressor switchover, simultaneous filling of two silos from one blower, or nitrogen purge activation can all increase instantaneous gas flow by 40–100% above normal operating conditions. Include a 15–20% safety margin on calculated orifice area to accommodate filter blinding degradation over time.
4. Common Sizing Mistakes and How to Avoid Them
4.1 Undersizing for Two-Phase Flow
Applying pure-gas equations to dust-laden vent streams is the most frequent error. When the silo contains fine cement, fly ash, or flour (particle size < 50 μm), the vent stream during relief can carry 500–2,000 g/m³ of solids. This increases the effective density of the discharge mixture by 2–5×, requiring proportionally larger orifice areas. Use EN 14491 dust explosion vent sizing equations (St_class correction) or apply the DIERS two-phase flow methodology with appropriate K_dust reduction factors.
4.2 Ignoring Temperature Effects
Hot material discharge (e.g., cement at 80–120°C, asphalt at 160°C) heats the silo headspace gas, increasing its volume and pressure. A silo receiving 100°C material with a headspace temperature of 60°C requires approximately 19% more relief capacity than the same silo at ambient temperature (Charles' Law: V₂ = V₁ × T₂/T₁). Specify the relief valve for the maximum anticipated headspace temperature, not ambient conditions.
4.3 Improper Valve Selection
Conventional safety valves designed for steam or clean gas service are unsuitable for dusty silo applications. Specify dust-service relief valves with soft-seated discs, anti-stick coatings, and large internal passages. Rupture panels (explosion vents) are preferred for low-pressure silos storing combustible dusts, as they do not reclose and allow full discharge without spring fatigue. For non-combustible materials, spring-loaded relief valves with position indication switches provide reusable protection with visual status confirmation.
5. Integration with Silo Design and EPC Project Delivery
5.1 Coordination with Silo Structural Design
The relief valve's set pressure must be coordinated with the silo designer's MAWP calculation. For bolted steel silos, the MAWP is governed by bolt shear capacity and panel seam strength, typically 20–25 kPa. For welded concrete silos, MAWP can reach 50–100 kPa depending on wall reinforcement. The EPC contractor must confirm MAWP before specifying the relief valve set pressure, as an over-set valve provides no protection, while an under-set valve causes nuisance discharges during normal filling.
5.2 Instrumentation and Monitoring Integration
Modern silo systems integrate relief valve status with the plant DCS/PLC. Position switches on spring-loaded valves signal open/closed state. Pressure transmitters in the headspace provide real-time overpressure alarms (typically set at 80% of relief valve set pressure) and automatic shutdown of the pneumatic conveying blower. This layered protection approach—alarm at 80%, blower trip at 90%, relief at 100%—reduces the frequency of relief valve actuation and extends service life.
6. Example Case Study: Cement Silo Relief Valve Sizing
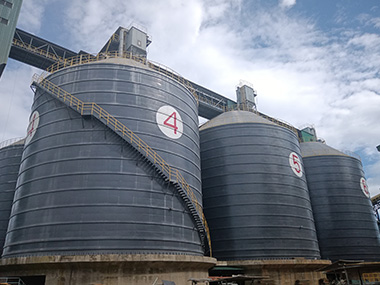
Project Parameters: 5,000-ton bolted steel cement silo, 18 m diameter × 22 m height. Pneumatic conveying via rotary screw blower, 15 m³/min FAD at 0.35 MPa gauge. Cement temperature at inlet: 90°C. Headspace design temperature: 55°C. Silo MAWP: 25 kPa gauge. Vent filter area: 25 m² with reverse-air cleaning.
Calculation: Q_relief = 15 × (0.4513 / 0.1013) = 66.8 m³/min at atmospheric conditions. Corrected for 55°C (328 K) vs. standard 20°C (293 K): Q_corrected = 66.8 × (328/293) = 75.0 m³/min. Two-phase flow factor (K_dust = 0.6 for cement, d₅₀ = 30 μm). Required orifice area: A = (75,000 L/min × √(28.97 / (1.0 × 328))) / (