


Silo Price Factors: What Actually Drives the Cost of Industrial Bulk Storage
Silo pricing isn't a simple per-tonne calculation. The two biggest cost drivers are structural steel weight (which scales with diameter, height, and stored material density) and ancillary systems (dust collection, aeration, explosion venting, and level instrumentation). A 3,000-tonne cement silo can cost anywhere from $180,000 to $450,000 depending on these variables. Here's what moves the needle.
1. Silo Capacity and Dimensions — The Math That Sets Your Baseline
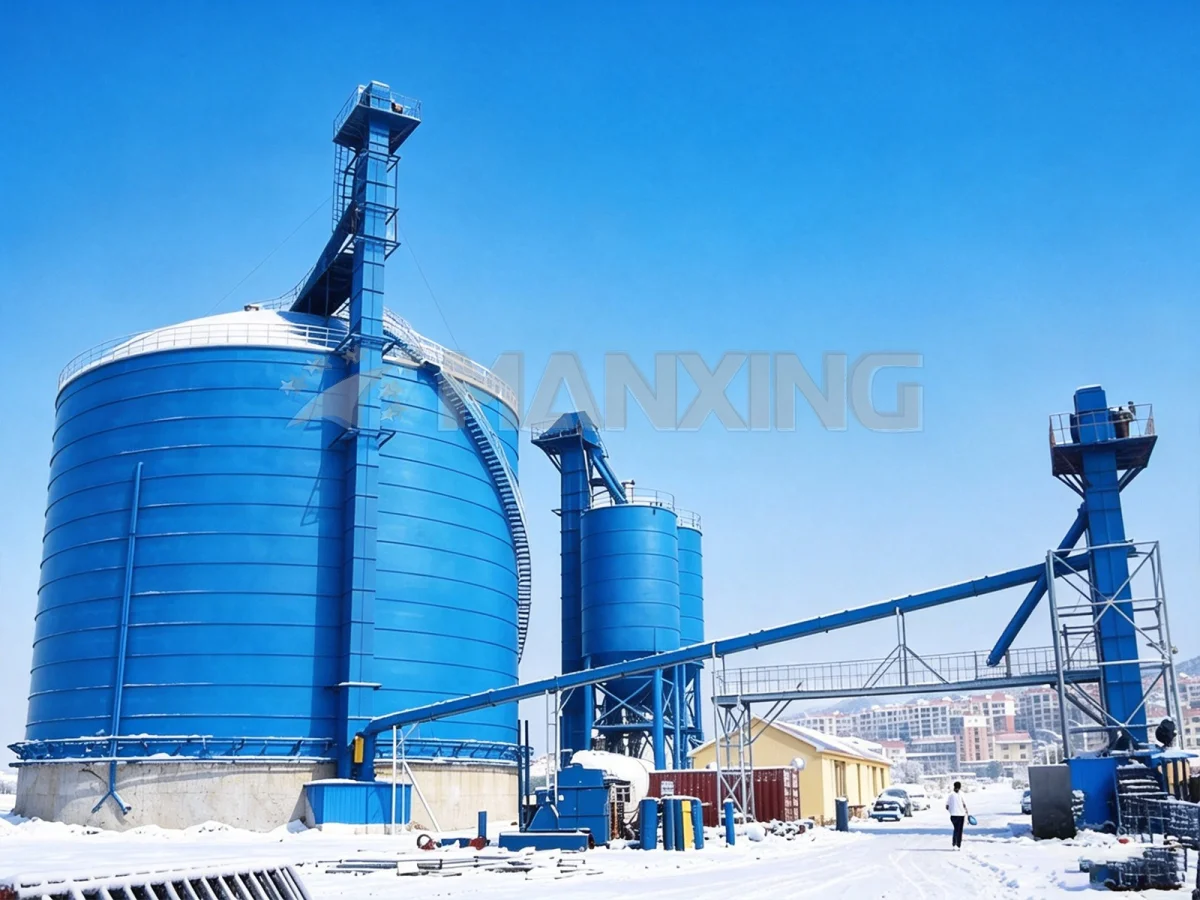
Capacity is the starting point, but it's not the whole story. Two silos holding the same tonnage can have wildly different steel weights — and therefore wildly different prices — based on their diameter-to-height ratio.
Diameter vs. Height Trade-offs
A 2,000-tonne cement silo at 12m diameter × 28m height uses roughly 18 tonnes of structural steel. Stretch that to 16m diameter × 18m height for the same capacity, and you're looking at 24 tonnes of steel. The wider silo needs thicker walls to resist hoop tension from the stored material. That's an extra 6 tonnes of steel at roughly $1,800–$2,200 per tonne fabricated, erected, and painted. Add $12,000–$14,000 to the bill before you've even talked about the foundation.
But here's the catch: the taller, narrower silo needs a deeper, heavier foundation because the load is concentrated on a smaller footprint. In soft soil conditions — say, a coastal site in Vietnam with a bearing capacity of 80 kPa — that taller silo might need pile foundations adding $25,000–$40,000. The wider silo spreads the load and might get away with a simple mat foundation. So the "cheaper" steel option isn't always cheaper overall.
Wall Thickness Calculations
Wall thickness isn't arbitrary. It's calculated per EN 1993-4-1 (Eurocode 3: Design of steel structures — Silos) or ASME BTH-1 for bottom tension calculations. For a cement silo, you're typically looking at 6mm shell plate at the top, stepping up to 10mm or 12mm at the bottom where hoop tension peaks. For abrasive materials like clinker or slag, add 2–3mm as a wear allowance — or specify a replaceable liner system.
I've seen projects where the client insisted on uniform 8mm walls to "save money." The silo lasted four years before the bottom rings needed patching. The repair cost more than the original steel upgrade would have.
Foundation Load Requirements
A fully loaded 5,000-tonne coal silo exerts a vertical load of roughly 45–50 MN on the foundation. That's 4,500–5,000 tonnes of force spread across a ring beam or circular mat. The foundation design per EN 1997 (Eurocode 7: Geotechnical design) depends entirely on your geotechnical report. I've worked on sites where the report was six months old and the water table had risen 2m since drilling. The foundation had to be redesigned on-site. That's a $15,000–$30,000 change order nobody budgeted for.
2. Material Selection — Steel Grade, Coating, and Abrasion Reality
The steel grade you specify affects both material cost and fabrication cost. Higher-strength steel lets you use thinner plates, but it's harder to weld and requires more stringent quality control.
Carbon Steel vs. Stainless Steel
For most bulk solids — cement, fly ash, coal, sand — carbon steel (S355JR or equivalent per EN 10025) is the standard. It runs about $800–$1,100 per tonne for the raw plate. Stainless steel (304 or 316) runs $3,500–$5,500 per tonne. You don't need stainless for cement. You do need it for certain chemical powders, alumina in some purity-sensitive applications, or food-grade materials. If your process engineer says "stainless," ask why. Sometimes it's justified. Sometimes it's a spec that's been copied from a previous project without thinking.
Internal Coatings and Liners
A two-coat epoxy system (150–200 microns DFT) adds $15–$25 per square metre of internal surface. For a 3,000-tonne cement silo with roughly 400m² of internal area, that's $6,000–$10,000. It's cheap insurance against material adhesion and corrosion. For abrasive materials, I'd rather specify a wear liner — either a 6mm Hardox 450 plate or a ceramic-lined chute system. Hardox runs about $2,800–$3,500 per tonne, but it'll outlast mild steel by a factor of 5–8 in high-wear zones.
Abrasion-Resistant Options
Clinker is brutal. It's hard, it's hot (sometimes 150°C straight from the cooler), and it's sharp. I remember a project in Malaysia where the client used standard carbon steel for a clinker silo cone. Eighteen months later, the cone was paper-thin in the flow channel. We had to shut down for a week and weld in a new cone section. The downtime cost them more than the entire silo. Now I specify a minimum 10mm cone with a replaceable 6mm Hardox liner for any clinker application. It adds $8,000–$12,000 to the silo price. It's the cheapest insurance you'll ever buy.
3. Stored Material Properties — Density, Flow Behavior, and Hazard Class
What you're storing matters as much as how much you're storing. Material density, particle size, moisture content, and flow characteristics all feed into the structural and mechanical design.
Bulk Density and Angle of Repose
Cement has a bulk density of roughly 1.1–1.3 t/m³. Coal is 0.8–1.0 t/m³. Slag is 1.2–1.5 t/m³. That density directly determines the silo volume you need for a given tonnage. But the angle of repose matters too — it affects the cone geometry and the effective capacity. A material with a 40° angle of repose needs a steeper cone than one with a 25° angle. Steeper cone means more steel, more fabrication complexity, and a higher center of gravity (which affects seismic design).
Flow Patterns: Mass Flow vs. Funnel Flow
Mass flow silos — where all material moves during discharge — require a steep, smooth cone (typically 60–70° from horizontal) with a low-friction surface. Funnel flow silos use a shallower cone (45–55°) and are cheaper to build. For materials that degrade with time in the dead storage zone (some chemical powders, certain grades of fly ash), mass flow is non-negotiable. The cost difference is roughly 15–20% more steel in the cone section plus a more sophisticated outlet arrangement.
Dust Explosion Risk and Venting
Coal, fly ash, and many chemical powders are combustible dusts. If your material has a Kst value above 100 bar·m/s (per ISO 21873 or EN 14491), you need explosion venting or suppression. A single explosion vent panel for a large silo costs $2,000–$5,000. A full suppression system with chemical agents and detection hardware runs $15,000–$40,000. This isn't optional — it's a safety requirement under ISO 15012 and most national regulations. I've seen plants skip it to save money. I've also seen what happens when a dust cloud ignites in an unvented silo. You don't want to be that plant.
4. Site Conditions and Climate — Wind, Seismic, and Temperature
The same silo design that works in inland China needs significant modification for a coastal site in the Philippines or a seismic zone in Turkey. Environmental loads are often the governing design case.
Wind Load Zones
Wind load per EN 1991-1-4 (Eurocode 1: Actions on structures) is a function of basic wind velocity, terrain category, and the silo's height and shape. A silo in a typhoon-prone region (basic wind velocity 45 m/s or higher) needs thicker shell plates, more robust stiffeners, and a heavier roof structure than the same silo in a sheltered inland location (25 m/s). The difference in steel weight can be 20–30%. For a 3,000-tonne silo, that's an extra 4–6 tonnes of steel. At $2,000 per tonne all-in, you're looking at $8,000–$12,000 more.
Seismic Design Categories
Seismic design per EN 1998-4 (Eurocode 8: Structures in seismic regions) adds lateral load cases that often govern the shell-to-base connection and the ring beam design. In high seismic zones (ground acceleration > 0.25g), you need anchor bolts, a reinforced concrete ring beam, and sometimes seismic isolation bearings. The anchor bolt cage alone for a 5,000-tonne silo can cost $5,000–$10,000. The ring beam adds another $15,000–$30,000 to the foundation cost. It's not glamorous, but it's what keeps the silo standing when the ground moves.
Temperature Extremes and Thermal Cycling
In northern China, winter temperatures hit -30°C. In the Middle East, summer surface temperatures on a steel silo roof can exceed 70°C. Thermal cycling causes fatigue at welded joints, especially at the shell-to-cone junction. For extreme cold, you need impact-tested steel (e.g., S355J2 per EN 10025, tested at -20°C). That's a 10–15% premium over standard S355JR. For extreme heat, you need a reflective roof coating and possibly insulation if the material is temperature-sensitive. A 50mm mineral wool insulation layer on the roof adds $3,000–$6,000.
5. Ancillary Systems — The Hidden 30–40% of Your Budget
The silo shell is maybe 60–70% of the total installed cost. The rest is the stuff that makes it actually work: aeration, dust collection, level monitoring, and structural accessories.
Aeration and Fluidization
Aeration systems for cement or fly ash silos typically use fluidizing panels or air pads in the cone section. A basic aeration system for a 3,000-tonne cement silo — including blower, piping, and fluidizing media — costs $8,000–$15,000. For difficult materials (fine fly ash, high-moisture content), you might need a more aggressive system with multiple aeration zones and a larger blower. That pushes to $20,000–$30,000. Skip it, and you'll spend that money ten times over in manual poking, air lance rentals, and lost production.
Dust Collection and Filtration
A silo filter receiver (baghouse) for a 3,000-tonne cement silo during pneumatic filling needs a filtration area of roughly 40–60m². A standard pulse-jet baghouse with differential pressure monitoring costs $12,000–$25,000. If the material is toxic or the emissions limit is strict (say, 10 mg/m³ per local regulations), you need HEPA-grade filtration and possibly a secondary stage. That doubles the price. The filter is the lungs of your silo. Don't cheap out on it.
Level Monitoring and Automation
A basic rotary paddle level indicator costs $300–$600. A continuous radar level transmitter costs $1,500–$3,500. For a plant with inventory management and automated filling sequences, you want continuous measurement plus high-level and overfill alarms. A full instrumentation package — radar level, temperature sensors, pressure transmitters, and a local PLC — runs $8,000–$20,000. It's not just about knowing how full the silo is. It's about preventing overfilling, which is the single most common cause of silo structural failure.
6. Fabrication, Transport, and Installation — Where Projects Go Off the Rails
The silo design is only half the battle. How it's built, shipped, and erected can make or break your budget.
Shop Fabrication vs. Field Assembly
Shop-welded panels (typically 2.4m wide × 8–12m long) are fabricated in a controlled environment with consistent quality. Field-welded silos are built plate by plate on-site. Shop fabrication costs more per tonne ($2,200–$2,800 vs. $1,800–$2,200 for field welding), but the quality is better, the schedule is shorter, and you avoid weather delays. For a 3,000-tonne silo, shop fabrication might add $15,000–$25,000 to the steel cost but save 3–4 weeks on the schedule. In most markets, that schedule savings is worth more than the premium.
Transport Logistics and Module Sizes
A 12m diameter silo shell won't fit on a standard flatbed truck. You either ship it in panels (which means more field welding) or you use specialized wide-load transport with escort vehicles. Wide-load transport for a 4.5m-wide panel can cost $3,000–$8,000 per truckload depending on distance and route restrictions. I've had projects in Indonesia where the only access road to the site was a 3.5m-wide village road. We had to redesign the panel sizes to fit. That added two weeks to the fabrication schedule and $12,000 in redesign costs. Check your access routes before you finalize the design.
Erection Sequence and Crane Access
A 30m-tall silo needs a crane with at least 40m boom length. In urban or congested plant sites, crane access is often the limiting factor. I've seen projects where the only available crane position required a 200-tonne mobile crane instead of the planned 100-tonne unit. The daily rental difference is $2,000–$4,000. Over a 10-day erection period, that's $20,000–$40,000 in unexpected costs. Always do a crane study before you price the erection. Always.
Case Study: 5,000-Tonne Fly Ash Silo — Cement Plant, Shandong Province
A cement plant in Shandong needed a 5,000-tonne fly ash silo for a new grinding circuit. The initial budget was $280,000 based on a generic quote from a supplier who didn't ask about the material properties or site conditions.
Here's what we found during the detailed engineering phase: the fly ash had a bulk density of 0.75 t/m³ (lower than expected), requiring a larger silo volume. The site was in a seismic zone with 0.15g design acceleration. The client wanted mass flow for consistent quality. And the local emissions limit required a baghouse with <10 mg/m³ outlet concentration.
The final scope included a 16m diameter × 32m height shop-welded steel silo with S355J2 material (for -20°C impact resistance), a 65° mass flow cone with internal epoxy coating, a 60m² pulse-jet baghouse, full aeration system, radar level instrumentation, explosion venting per EN 14491, and a reinforced concrete ring beam foundation with 24 × M30 anchor bolts.
Final installed cost: $385,000. The client was initially sticker-shocked until we walked them through the line-item comparison. The generic quote didn't include the seismic ring beam ($28,000), the upgraded baghouse ($18,000), the aeration system ($14,000), or the explosion venting ($6,500). Add those to the generic quote and you're at $332,500 — and that's without the seismic design, which would have required a complete redesign after the building permit review. The "expensive" quote was actually the realistic one.
Frequently Asked Questions
Q: What's the typical cost per tonne of storage capacity for a welded steel silo?
For a standard cement or fly ash silo in a non-seismic, moderate-wind region, expect $40–$80 per tonne of capacity for the silo shell and basic accessories. Add $15–$30 per tonne for the foundation, and $10–$25 per tonne for the filter receiver and aeration system. A 3,000-tonne silo with full ancillary systems typically runs $180,000–$350,000 installed. For abrasive or hazardous materials, or for sites with extreme environmental loads, the range shifts to $250,000–$500,000.
Q: Does bolted construction cost more than welded?
Yes, typically 15–25% more for the silo shell itself. Bolted silos use thicker plates and more steel because you can't achieve the same material efficiency with bolted joints as you can with continuous welds. However, bolted silos are faster to erect (no field welding, no welding inspection, no weather delays) and easier to disassemble or relocate. For temporary installations or sites with restricted hot-work permits, the premium is often worth it. For permanent installations in cement or steel plants, welded is almost always the better value.
Q: How much does the foundation typically add to the total project cost?
The foundation usually represents 15–25% of the total installed cost. For a 3,000-tonne silo on good soil (bearing capacity > 150 kPa), expect $25,000–$45,000 for a reinforced concrete mat or ring beam foundation. On poor soil or in high seismic zones, that can jump to $50,000–$100,000 with pile foundations or deep ring beams. The geotechnical investigation ($3,000–$8,000) is the cheapest insurance you'll buy — it tells you which end of that range you're in.
Get a Detailed Silo Cost Estimate for Your Project
Every silo project is different. Material properties, site conditions, capacity requirements, and local regulations all affect the final price. At Manxing, we provide detailed, line-item cost estimates based on your specific parameters — not generic per-tonne numbers that leave out half the scope.
Tell us what you're storing, how much, and where. We'll give you a realistic number with no surprises.
Request a Project Quote