


Common Installation Mistakes That Kill Industrial Silos — and How We Stop Them
Most silo failures don't start with a dramatic collapse. They start with a 2 mm anchor bolt offset, a skipped weld pass, or a dust collector piped backwards. After 15 years of EPC silo contracting across 30+ countries, I can tell you this: the mistakes that cost you aren't the ones in the design office. They're the ones made at 6am on a Tuesday, in the rain, by a crew that's three days behind schedule. Here's what actually goes wrong — and what we do about it.
1. Foundation and Anchor Bolt Errors
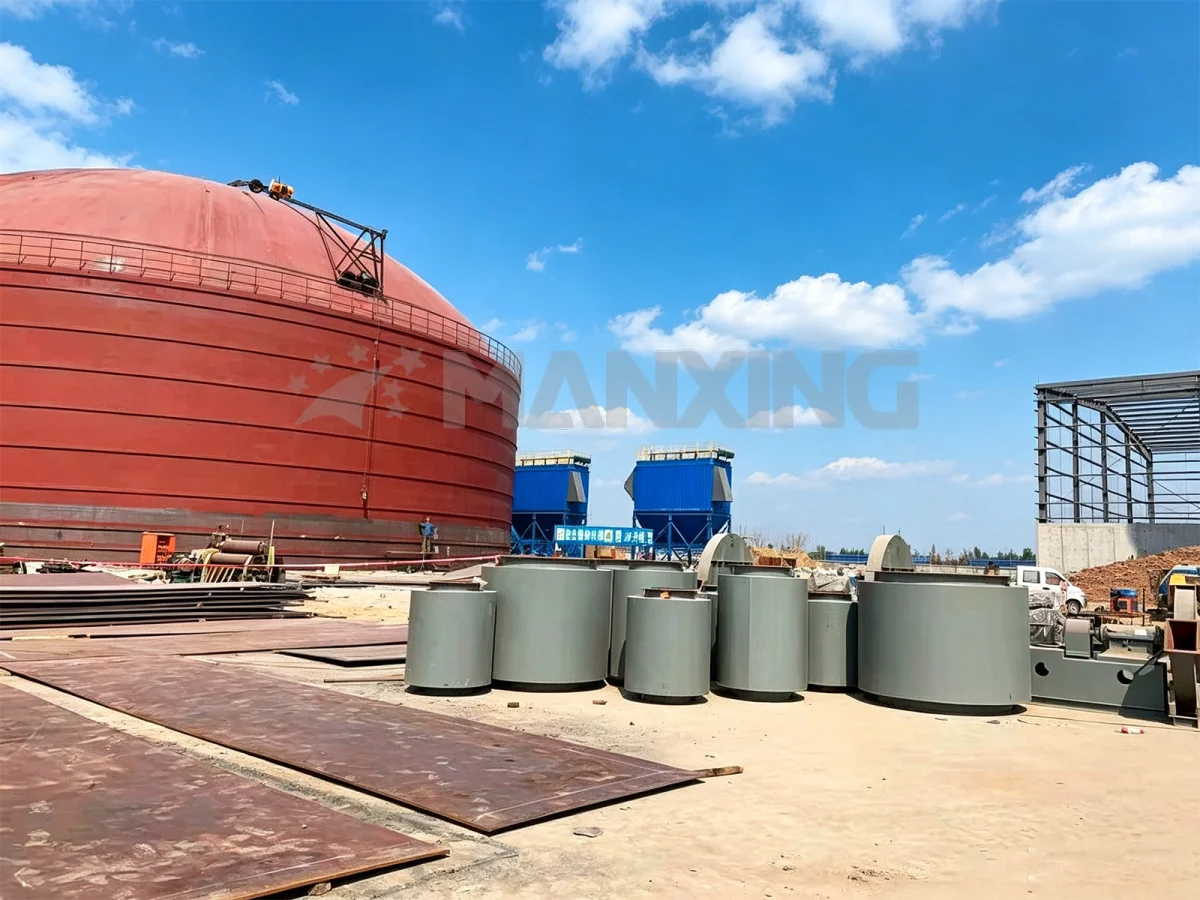
The silo doesn't care how pretty your shell plates look if the foundation is wrong. This is where projects go sideways before the first panel even arrives.
1.1 Anchor Bolt Position Tolerance Drift
We specify anchor bolt positional tolerance at ±3 mm from theoretical center. That's not arbitrary — it's the clearance between the bolt and the base plate hole. Go beyond 5 mm and you're either reaming holes in the field (which weakens the connection) or forcing bolts into position, which pre-loads them in ways the structural calc never accounted for.
I remember a project in Vietnam where the civil contractor had placed 14 anchor bolts with offsets between 8 and 12 mm. The erection crew tried to "persuade" them with a hydraulic jack. We caught it during the pre-erection survey and stopped work. The fix meant chipping out 14 bolt pockets, re-grouting with Sikadur-42, and a 10-day delay. The plant manager wasn't happy. But a silo that can't handle its own seismic load because the anchors are pre-stressed? That's a different kind of unhappy.
Under EN 1090-2, anchor bolt assemblies for steel structures require positional verification before any structural steel erection begins. We check every single bolt with a total station — not a tape measure, not a string line. If the civil contractor's survey doesn't match ours within 3 mm, we don't proceed. Full stop.
1.2 Grouting Gaps Under Base Plates
The base plate sits on a grout pad. That grout pad has to carry the full compressive load of the silo — for a 5,000-tonne cement silo, we're talking about bearing pressures around 180 kPa at the shell perimeter. If the grout isn't properly mixed, poured, or cured, you get voids. Voids mean point loading. Point loading means the base plate deflects. Deflection means the first shell course goes out of round.
We use non-shrink epoxy grout with a minimum compressive strength of 70 MPa at 28 days. The pour temperature has to stay above 10°C — we've had to heat the foundation with propane salamanders in a project in Inner Mongolia where the ambient temperature was -15°C in November. The crew complained. The grout cured properly. That's the trade-off.
2. Shell Plate Assembly and Welding Defects
The shell is the pressure boundary. It's also the structural element that resists wind, seismic, and the internal pressure from pneumatic filling. Every weld matters. Every bolt matters. And the field conditions are never as clean as the shop.
2.1 Vertical Weld Misalignment and Lack of Fusion
Vertical seams on a welded silo carry hoop tension. For a 3,000-tonne clinker silo with a 12 m diameter, the hoop tension at the bottom shell course runs about 1,200 kN/m. That vertical weld better be full penetration, full stop.
The most common field mistake? Welding in wind speeds above 3 m/s without proper shielding gas coverage. The gas shield gets blown away, you get porosity, and the weld looks fine on the surface but has a 3 mm lack-of-fusion defect running down the center. We've seen radiographic testing reject 40% of vertical welds on a single project because the erection contractor didn't set up wind breaks. The rework cost more than the original welding.
Our welding procedure specifications (WPS) follow EN ISO 15614-1 and require 100% ultrasonic testing on all full-penetration vertical seams. If the wind exceeds 3 m/s, welding stops. No exceptions. I don't care if the schedule is tight.
2.2 Bolted Shell Joint Torque Errors
For bolted silos — and we build a lot of them for fly ash and alumina — the bolt torque is everything. A typical M20 Grade 10.9 bolt in a flanged joint needs a final torque of 470 Nm. Under-torque it by 15% and the joint slips under load. Over-torque it by 20% and you yield the bolt.
We use calibrated hydraulic torque wrenches, and every bolt gets marked after torquing. The pattern matters too — star pattern, three passes, final torque on the third pass. I've seen crews do a single-pass circular pattern because it's faster. The flange leaks. Material leaks. The plant shuts down. The math on a quarterly bolt-torque check takes our crew four hours. It added seven years to one silo's service life in Shandong. The math works.
3. Conical Roof and Structural Steel Installation
The roof isn't just weather protection. On a cement or coal silo, it supports the filling conveyor, the dust collector, the pressure relief valves, and sometimes a man-load of 500 kg/m² for maintenance access. Get the roof wrong and you're not just leaking rain — you're risking a dust explosion vent that doesn't vent.
3.1 Roof Beam Alignment and Support Column Plumbness
Roof beams on a large silo span 15 to 25 meters. The support columns need to be plumb within 1:500 — that's 20 mm over a 10 m column height. Sounds generous until you realize that a 30 mm out-of-plumb column shifts the roof beam reaction point, which changes the bending moment in the beam by 12%. That's the difference between a beam that works and one that deflects 40 mm under snow load.
We check column plumb with a theodolite before any roof beams go up. If a column is out, we shim the base — we don't try to pull it straight with a crane. Pulling a 30-tonne column with a 25-tonne crane is how people get hurt.
3.2 Pressure Relief Valve Sizing and Orientation
Here's one that kills people. The pressure relief valve on a cement silo has to handle the maximum pneumatic conveying rate. For a typical silo filling system running at 0.5 bar gauge with a 150 mm diameter fill line, the relief valve needs a minimum effective area of 0.15 m². Install a valve that's too small, or orient it so the discharge points at the adjacent silo, and you've got a problem.
EN 14491 requires that pressure relief devices on dust-handling equipment be sized for the worst-case scenario — usually a blocked discharge combined with continued conveying. We size for KSt values up to 200 bar·m/s for cement and up to 300 bar·m/s for coal dust. The relief valve goes on the roof center, discharge vertical, with a flame-quenching mesh. Not on the side. Not pointing at the operator platform. Center. Vertical. Every time.
4. Conveying and Aeration System Integration
The silo is just a tank. The conveying and aeration systems are what make it work. And this is where the mechanical contractor and the silo contractor often stop talking to each other — with expensive consequences.
4.1 Aeration Airflow and Pad Placement
For a fly ash silo, aeration pads typically require 0.8 to 1.2 Nm³/min per m² of aeration area. The pads need to cover 10-15% of the silo floor area, arranged in zones that can be independently controlled. Install the pads too close to the center and the material channels to the side. Too close to the wall and you get dead zones where the ash compacts and never discharges.
We had a project in India where the mechanical subcontractor installed aeration pads based on the general arrangement drawing but didn't account for the actual slope of the cone floor. The pads were supposed to sit on a 55° cone, but the civil crew had poured it at 48°. The pads didn't sit flat, the air gaps were uneven, and the discharge rate dropped from 200 t/h to 80 t/h. The fix meant chipping the cone and re-casting sections. Three weeks of downtime.
4.2 Pneumatic Conveying Line Routing and Support
Conveying lines from the blower station to the silo inlet experience pressure cycles every time a batch runs. A typical dense-phase system operates at 2.5 to 3.5 bar gauge. The pipe supports need to handle both the static load and the dynamic load from pressure pulses. We specify supports every 3 meters for 150 mm diameter pipe, with flexible gaskets at every flange connection.
The mistake we see most often? Rigid pipe supports welded directly to the silo shell. The silo expands and contracts with temperature — a 20 m tall steel shell in a desert climate can grow 12 mm from winter to summer. A rigid pipe support doesn't move. Something gives. Usually it's the pipe flange, and then you've got cement dust leaking at 3 bar pressure. We use sliding supports with PTFE pads on all shell-mounted pipe brackets. The pipe moves. The shell moves. They don't fight each other.
5. Dust Collection and Venting Misalignment
Dust collectors on silos aren't optional. They're the difference between a plant that meets ISO 15012 dust exposure limits and one that gets shut down by the environmental regulator. But the installation is where things fall apart.
5.1 Dust Collector Inlet and Outlet Piping
The dust collector inlet connects to the silo vent. The clean air outlet goes to the atmosphere (or back to the plant). The dust discharge goes back into the silo. Get any of these backwards and you've got a problem.
The most common error: connecting the dust collector outlet to the silo inlet. It sounds obvious, but when you've got a crew working from a 2D P&ID at night, with pipes that all look the same, it happens. The dust collector blows filtered air back into the silo, the silo pressurizes, the relief valve opens, and you're venting material to atmosphere. We color-code all pipes during fabrication — yellow for dirty air, blue for clean air, green for material discharge. The crew can't mix them up even if they're working in the dark.
5.2 Baghouse Pulse Valve Timing and Compressed Air Quality
The pulse-jet cleaning system on a baghouse needs dry, oil-free compressed air at 5.5 to 6.5 bar gauge. The pulse duration is typically 100-200 ms, with a cycle time of 30-120 seconds depending on dust loading. Install the compressed air supply without a dryer and the moisture combines with cement dust to form a concrete-like cake on the filter bags. Differential pressure climbs from 800 Pa to 2,500 Pa in two weeks. The bags are ruined.
We specify a refrigerated air dryer with a pressure dewpoint of 3°C and a 10-micron pre-filter before the baghouse manifold. The pulse valve timing is set during commissioning based on the actual differential pressure — not from a table in a manual. Every silo application is different.
6. Commissioning Oversights
Commissioning is where you find out if the installation was done right. And it's where the pressure to hand over the keys leads to shortcuts that come back six months later.
6.1 Load Testing and Settlement Monitoring
Before we hand over a silo, we fill it to 100% capacity and hold it for 72 hours. We monitor foundation settlement at 8 points around the perimeter with precision leveling equipment — accuracy of ±0.3 mm. Total settlement should not exceed 25 mm for a raft foundation on medium-dense sand. Differential settlement — the difference between the highest and lowest point — should not exceed 1:500.
On a project in Egypt, we measured 35 mm of differential settlement during the load test. The silo was tilting. We stopped the fill, investigated, and found a soft pocket under one section of the raft that the geotechnical survey had missed. The fix meant pressure grouting under the foundation and re-leveling. It added three weeks to the schedule. But a 5,000-tonne silo that's tilting 1:200 is a silo that's going to have problems for its entire life.
6.2 Instrument Calibration and Interlock Verification
Level indicators, high-level alarms, pressure switches, temperature sensors — every instrument gets calibrated before commissioning. The interlocks get tested with actual signals, not just a multimeter on the terminals. We simulate a high-level condition by jumping the level switch and verify that the filling system shuts down within 2 seconds. We simulate a high-pressure condition and verify the relief valve opens. We simulate a dust collector failure and verify the silo isolation valve closes.
Skip this step and you're relying on the operator to notice a problem before the silo does. Operators are good. But they're not as fast as a pressure switch.
A contractor had completed erection of a 3,000-tonne coal silo but skipped the anchor bolt torque verification during a rushed night shift. During the first fill cycle, the base plate shifted 4 mm at three bolt locations, causing a gap that allowed coal dust to escape at the shell-to-base junction. The plant noticed dust emissions on day three of operation. We were called in to investigate. The fix meant unloading the silo (3,000 tonnes of coal, 14 days of discharge), re-torquing all 96 anchor bolts to 470 Nm with a calibrated hydraulic wrench, and re-grouting the base plate with SikaGrout-212. Total cost of the rework: $47,000. Total cost of doing it right the first time: about $2,000 in labor and equipment. The lesson? A $2,000 check during installation prevents a $47,000 repair during operation.
FAQ
Q: What's the most common installation mistake you see on industrial silos?
Anchor bolt positional errors and base plate grouting defects. They're invisible once the silo is erected, but they're the root cause of more structural problems than anything else. We've stopped work on-site more than 20 times in the last decade because the foundation wasn't ready. Every single time, the client thanked us later.
Q: How long does it typically take to commission a large industrial silo?
For a 3,000 to 5,000-tonne silo with full mechanical, electrical, and instrumentation systems, commissioning takes 14 to 21 days. That includes load testing, instrument calibration, interlock verification, and a 72-hour continuous operation trial. Rushing commissioning to meet a deadline is how you miss the problem that costs you six months of downtime later.
Q: What standards govern industrial silo installation?
The primary standards are EN 1090-2 for steel structure execution, EN 1993-4-1 for silo and tank design, EN 14491 for dust explosion protection, and ISO 15012 for dust exposure limits. In China, we also follow GB 50077 for silo structural design and GB 50205 for steel structure installation quality acceptance. Every project gets a standards compliance matrix before construction begins — no ambiguity about which code applies.
Manxing provides full EPC silo contracting — from foundation design through commissioning — for cement, clinker, fly ash, coal, slag, and aggregate plants worldwide. We've delivered silo projects across 30+ countries with a track record of on-time, on-budget handovers. Our field teams don't just install silos — we verify every bolt, every weld, and every instrument before we hand over the keys.
Contact Manxing today for a project consultation →