


Silo Roof and Hopper Installation: A Field Engineer's Guide
Silo roof and hopper installation is where precision meets heavy lifting — and where most long-term problems begin. Install them wrong and you'll spend years chasing water ingress, bolt loosening, and material hang-up. This guide covers the installation sequence, bolt torque specifications, sealing methods, and quality control checkpoints that keep a silo tight and flowing for 20+ years in cement, fly ash, coal, and other bulk solids applications.
Roof Structure Types and Selection Criteria
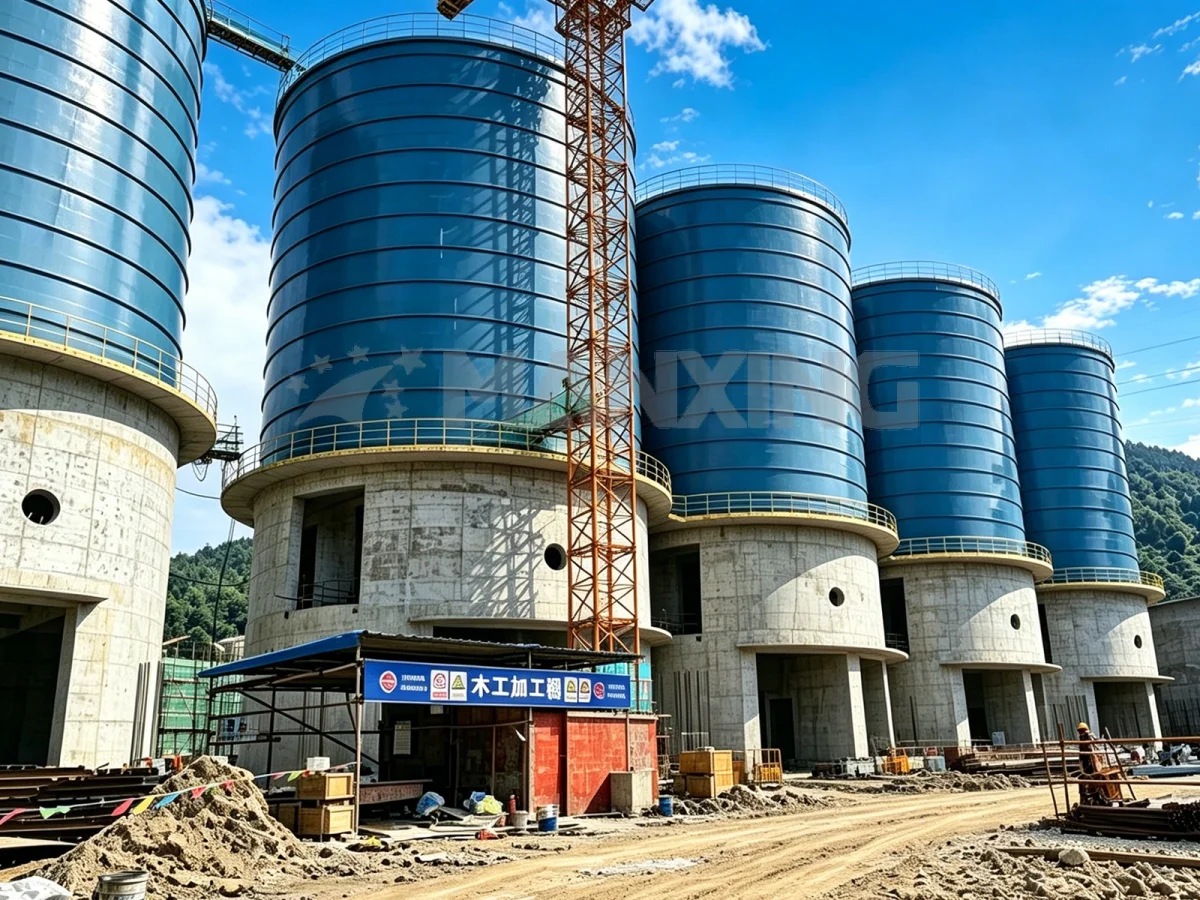
The roof isn't just a lid. It's a structural element that handles wind uplift, snow loads, dust collector weight, and sometimes a full maintenance crew standing on it. Pick the wrong configuration and you'll fight leaks, ponding water, or fatigue cracks within the first two years.
Conical vs. Domed vs. Flat Roof Designs
Conical roofs — typically sloping at 15° to 30° from center — are the workhorse of industrial silos. They shed water naturally, distribute load evenly to the shell, and are relatively straightforward to erect with bolted segments. For silos under 25m diameter, a 20° cone with a central apex ring is the sweet spot. We've installed hundreds of these on cement and clinker silos across Southeast Asia and they perform well if the sealing details are done right.
Domed (spherical) roofs handle negative pressure better — critical if you're running a dust collector that pulls 4,000 Pa or more. The curved profile resists buckling under vacuum, which flat roofs simply can't do without heavy stiffening ribs. But domed roofs are harder to fabricate and more expensive. You're looking at 15–25% more steel tonnage compared to a simple cone of the same diameter.
Flat roofs exist, mostly on very large diameter silos (40m+) where the roof doubles as a platform for baghouses and air slides. I'm not a fan unless the client specifically needs that walking surface. They pond water, they need meticulous slope design, and the membrane waterproofing has a shorter service life than you'd think — often 8–12 years before re-coating is needed.
When Each Configuration Makes Sense
For a 3,000-tonne cement silo with a dust collector mounted on top, go conical with a central apex plate rated for the equipment load. For a coal silo in a cyclone-prone area, domed handles the wind loads better. For a 50m-diameter fly ash silo with multiple air slide landings, flat with internal drainage channels is probably unavoidable.
The decision isn't purely structural. It affects how you sequence installation. A conical roof can be built from the top down while the shell is still being raised. A flat roof often goes on last, after all mechanical equipment is inside. That sequencing difference changes your crane schedule by a week or more.
Roof Panel Installation — Sequence, Bolt Torque, and Sealing
This is where I've seen the most failures. Not catastrophic collapses — those are rare. The slow, expensive kind: water seeping through bolt holes, gasket squeeze-out that creates leak paths, panels that shift because someone tightened bolts in the wrong order.
Panel Placement Order and Alignment
Roof panels are numbered. Follow the numbering. I know that sounds obvious, but I've watched crews on a site in Indonesia start at the "easy" side and work around, only to find the last panel is 40mm too narrow to fit. The fix? Cutting a custom panel on-site with a plasma cutter in 35°C heat, while the crane sits idle at $2,400/day.
Start from the reference panel marked on the drawing — usually aligned with the main access hatch or the gravity centerline. Work symmetrically outward. Alternate sides if you're placing panels from a central support ring. This keeps the load balanced and prevents the apex structure from drifting off-center.
For bolted roof systems, each panel typically connects to the top shell ring with M20 or M24 high-strength bolts (grade 8.8 or 10.9 per EN 14399). Panel-to-panel seams use the same bolt size but in double-shear configurations. The bolt spacing is usually 150–250mm center-to-center along the seam. Don't guess — the spacing is calculated based on the gasket compression requirements and wind uplift forces.
Bolt Torque Specifications and Verification
Here's the thing about bolt torque: the spec on the drawing isn't arbitrary. For a roof panel bolted connection using M20 grade 10.9 bolts with a neoprene gasket, the typical torque is 250–300 Nm. Under-torque and the gasket won't compress enough to seal. Over-torque and you crush the gasket, strip the thread, or distort the panel flange.
We torque in three passes: 50% of final value on the first pass, 80% on the second, 100% on the third. And we work in a star pattern — opposite bolts first, then fill in. This seats the gasket evenly. I've seen crews go around in a circle, which pulls the panel to one side and creates a gap on the opposite edge. That gap becomes a leak path that no amount of field sealant will fix permanently.
Torque wrenches need calibration. On a project in Vietnam, our crew discovered that two of their three wrenches were reading 15% low. They'd been "torquing" to 300 Nm when the actual value was 255 Nm. We had to re-torque 1,200 bolts. Four days of work that shouldn't have happened.
Gasket and Sealant Application
The gasket material matters more than most people think. For cement and fly ash silos, we use EPDM rubber — 3mm thick, 25mm wide, Shore A hardness 60–70. It handles the temperature swings (from -10°C at night to 60°C sun-baked steel) without cracking. Neoprene works too, but it stiffens faster in UV exposure.
Apply the gasket dry. No adhesive, no primer. Lay it in a continuous loop around each bolt hole, then run the seam gasket in a straight line with a 25mm overlap at joints. When you tighten the bolts, the gasket compresses to about 60% of its original thickness. That's your seal.
For the roof-to-wall junction, we add a secondary seal — a polysulfide or polyurethane applied over the bolted joint after torque verification. It's a belt-and-suspenders approach. The gasket handles the static seal; the sealant handles any micro-movement from thermal expansion or wind vibration.
Hopper Geometry, Fabrication, and Lifting
The hopper is where the material lives when it's not flowing. It's also where bridging, rat-holing, and dead stock happen if the geometry is wrong. Getting the hopper installed correctly means getting the slope angles, outlet position, and surface finish right — before it's 20 meters in the air.
Hopper Types: Conical, Pyramid, and Offset
Conical hoppers are symmetric, easy to fabricate, and work well for free-flowing materials like dry cement or fly ash. The slope angle — measured from horizontal — needs to be at least 10° above the material's angle of repose. For cement, that's typically 60–65° from horizontal. For sticky slag or wet fly ash, you might need 70° or steeper.
Pyramidal hoppers (four-sided) are cheaper to fabricate from flat plates but create corner dead zones where material sits and degrades. I've seen 80 tonnes of cement harden in the corners of a pyramidal hopper because the corner angle was only 45° from horizontal. The material just sat there for six months until someone had to go in with a jackhammer.
Offset hoppers — where the outlet is not centered — are used when the discharge conveyor runs along one side of the silo. They're harder to design because the asymmetric flow pattern creates uneven wall pressures. You need a steeper slope on the short side (the side closest to the outlet) to prevent bridging. We typically run 65° on the short side and 55° on the long side for offset cement hoppers.
Welding Standards and Inspection
Hopper welds are structural and they're also the flow surface. A weld bead that protrudes 2mm into the hopper interior can catch material and start a rat-hole. We specify full-penetration welds for the main seams (per EN 1090 Execution Class 2 for most industrial silos) and grind them flush on the interior face.
All hopper welds get 100% visual inspection and 10% ultrasonic testing (UT) on the main seams. For coal or explosive dust applications, we bump that to 20% UT per EN 14399 and add a magnetic particle inspection on the ground-welded seams. A single crack in a coal hopper weld can create a hot spot that ignites dust. That's not a hypothetical — it's happened.
The hopper-to-shell connection is the highest-stress joint in the entire silo. The hopper ring (usually a rolled angle or box section) carries the full weight of the stored material plus the hopper's own weight. For a 5,000-tonne clinker silo, that connection point sees a vertical load of roughly 65 MN. The weld here is full-penetration, ground flush, and 100% UT inspected. No exceptions.
Lifting and Positioning Large Hopper Assemblies
Small hoppers (under 50 tonnes) go up with a single crane lift. Large hoppers — the kind you see on 10,000-tonne cement silos — can weigh 120 tonnes or more. These are usually assembled on the ground inside the silo foundation and lifted as a single unit using a gantry crane or multiple crawler cranes.
I remember a project in Malaysia where we lifted a 140-tonne conical hopper using a 600-tonne crawler crane. The hopper had been assembled on a temporary steel frame at ground level, all welds completed and inspected. The lift took four hours. The rigging was four-point, using 50-tonne capacity slings at 45° angles. The hopper had to clear the top shell ring by 300mm to seat properly. We used four chain pulls (2-tonne capacity each) to guide it into position while the crane held it steady. The crew communicated via radio — one signal person, no hand signals at that height.
The critical detail: the hopper must be level within 5mm across its diameter before the final welds go in. If it's tilted, the material flow will be asymmetric and you'll get persistent rat-holing on the high side. We check level with a digital inclinometer on four points around the hopper ring, 90° apart.
Weatherproofing, Drainage, and Corrosion Protection
A silo roof that leaks is a silo that destroys its own contents. Cement hydrates. Fly ash clumps. Coal oxidizes and generates heat. Water ingress is the enemy, and it finds every gap you leave.
Roof-to-Wall Junction Sealing
The top of the shell wall is where the roof meets the cylinder. This junction sees the most movement — thermal expansion of the shell (a 30m-tall steel shell can grow 15mm vertically on a hot day), wind-induced sway, and settlement. The seal here has to accommodate movement without tearing.
We use a flexible flashing — typically a 1.5mm thick EPDM strip, 300mm wide — bolted to both the shell and the roof panel. The strip is installed with a 50mm "loop" or slack section that allows movement. The bolts are spaced at 150mm centers with EPDM washers under each head. Over the flashing, we apply a polysulfide sealant bead, 10mm wide, tooled to a smooth profile so water runs off rather than pooling.
The roof overhang — the distance the roof panel extends past the shell wall — should be at least 100mm. Less than that and water runs down the shell exterior, eventually finding its way through bolt holes or lap joints. I've seen 50mm overhangs that looked fine on paper but leaked within the first monsoon season.
Drainage Design and Overflow Prevention
Roof drainage is simple in concept: water hits the roof, flows to the edge, drips off. But on large flat or low-slope roofs, the volume of water is significant. A 30m-diameter roof in a 100mm/hour rainstorm sheds roughly 70 cubic meters of hour. That's a lot of water hitting the ground at once.
We install roof gutters on silos with flat or low-slope roofs (under 15°). The gutter is a continuous channel around the roof perimeter, sloped at 1% to a downspout. The downspout discharges to ground level, away from the foundation. For conical roofs, we rely on the overhang and let water drip — but we add a drip edge (a 20mm lip bent downward on the roof panel edge) to prevent water from tracking back under the panel.
Overflow is a real risk if the downspout gets blocked — by debris, ice, or a bird nest. We install a secondary overflow scupper (a 100mm x 100mm opening in the roof edge, 50mm above the gutter) that directs water away from the shell if the primary drain fails. It's a small detail that prevents a lot of damage.
Coating Systems for Harsh Environments
The roof and hopper exterior need coating protection, especially in coastal or chemical plant environments. For most industrial silos, we specify a three-coat system: zinc-rich primer (75μm DFT), epoxy intermediate coat (125μm DFT), and polyurethane topcoat (50μm DFT). Total dry film thickness: 250μm. This system lasts 15–20 years in a C3 corrosivity environment (per ISO 12944).
For coal silos or silos in high-humidity areas, we bump the total DFT to 320μm and use a micaceous iron oxide (MIO) epoxy as the intermediate coat. The MIO flakes create a barrier effect that slows moisture penetration. It costs about 20% more than standard epoxy but extends the recoating interval by 5–7 years.
The hopper interior coating depends on the material. For abrasive materials like clinker or slag, we often leave the hopper bare (mild steel, blasted to Sa 2.5 per ISO 8501) and rely on the natural wear pattern. For corrosive materials like gypsum or certain chemical powders, we apply a 300μm epoxy phenolic coating that resists both chemical attack and abrasion.
Quality Control and Safety During Installation
Installation quality isn't something you check at the end. It's built into every step — bolt by bolt, weld by weld, panel by panel. And safety isn't a separate topic; it's woven into the same sequence. A rushed crew is a sloppy crew, and a sloppy crew is a dangerous crew.
Dimensional Tolerance Checks
We check dimensions at four stages: before installation (panel and hopper fit-up on the ground), during installation (panel alignment and bolt torque), after installation (overall geometry and level), and after loading (settlement and deformation monitoring).
The key tolerances: roof panel alignment within ±3mm of the theoretical position, bolt torque within ±10% of the specified value, hopper level within ±5mm across the diameter, and shell verticality within H/1000 (where H is the silo height). For a 30m-tall silo, that's 30mm maximum deviation from plumb.
We use a total station for dimensional checks — not a tape measure and a level. The accuracy is 1mm at 50m distance, which is what you need to catch a panel that's 5mm out of position before the next one goes on. Once three panels are bolted, a misalignment compounds and you're fighting it for the rest of the roof.
Fall Protection and Working at Height
Roof installation means working at height — typically 25–45m above ground. Fall protection isn't optional and it isn't negotiable. We use a combination of perimeter safety cables (installed on the top shell ring before roof panels go up), personal fall arrest systems (harnesses with 2m lanyards), and temporary guardrails on the leading edge of the roof as it's being built.
The safety cables are steel wire rope, 12mm diameter, tensioned to 1.5kN, with intermediate supports every 6m. They're rated for two simultaneous falls (per EN 355). Each worker clips on before stepping onto the roof structure and stays clipped until they're back on the ground or on a certified platform.
On a project in the Philippines, we had a typhoon warning with 48 hours' notice. The crew had completed 60% of the roof panels. We secured every loose panel with additional clamps, lowered all tools and small equipment to ground level, and evacuated the roof. The typhoon hit with 120km/h winds. Not a single panel shifted. The preparation took six hours. The alternative — losing panels from 30m height — would have been catastrophic.
Case Study: 8,000-Tonne Clinker Silo — Roof and Hopper Installation
A cement plant in central China needed an 8,000-tonne clinker silo with a 32m diameter and 28m shell height. The roof was conical (22° slope) with a central dust collector mounting. The hopper was conical, 65° slope, with a 600mm diameter discharge gate.
The roof comprised 24 bolted panels, each weighing approximately 1.2 tonnes. We erected them over 12 days using a 200-tonne crawler crane. The panels were placed in the numbered sequence, torqued in three passes to 280 Nm (M24 grade 10.9 bolts), and sealed with EPDM gaskets and polysulfide sealant. The roof-to-wall junction used a 300mm EPDM flashing with a movement loop.
The hopper was assembled on the ground inside the foundation, welded to EN 1090 Execution Class 2, with 10% UT inspection on main seams. It weighed 95 tonnes and was lifted in a single operation using a 500-tonne crawler crane. The lift took three hours. Level was checked at four points — maximum deviation was 3mm, well within the 5mm tolerance.
Total installation time for roof and hopper: 18 working days. Zero safety incidents. The silo was water-tested (hose test at 5 liters/minute for 30 minutes) and passed with no leaks. It's been in service for four years with no reported issues.
Frequently Asked Questions
What bolt torque should I use for roof panel connections?
For M20 grade 10.9 bolts with EPDM gaskets, the typical torque is 250–300 Nm. For M24 bolts, it's 400–450 Nm. Always follow the project-specific torque specification on the drawing — it accounts for the gasket material, bolt coating, and connection geometry. Torque in three passes (50%, 80%, 100%) in a star pattern, not a circle.
How do I prevent water leaks at the roof-to-wall junction?
Use a flexible EPDM flashing (1.5mm thick, 300mm wide) with a 50mm movement loop, bolted at 150mm centers with EPDM washers. Apply a polysulfide sealant bead over the flashing after torque verification. Ensure the roof overhang is at least 100mm past the shell wall. Avoid silicone sealant — it fails within 18 months in UV exposure.
What's the maximum hopper level tolerance before final welding?
The hopper must be level within ±5mm across its diameter before the final welds to the shell ring are made. Check with a digital inclinometer at four points, 90° apart. If the hopper is tilted beyond this, the material flow will be asymmetric, causing persistent rat-holing on the high side and uneven wall loading.
Need Help with Your Silo Roof and Hopper Installation?
Manxing has designed and installed silo roof and hopper systems for over 200 projects across 30+ countries. From 2,000-tonne cement silos to 20,000-tonne clinker storage, we handle the engineering, fabrication, and installation — including bolt torque verification, weld inspection, and water testing. Contact us for a project review or installation support.