


Dust Explosion Prevention and Mitigation in Industrial Silos: What Actually Works
Dust explosions in industrial silos kill people and destroy plants every year. The two ways to stop them are preventing the explosion from starting and mitigating the pressure if it does. Both require strict adherence to standards like EN 14491 and ISO 15012, plus a design that accounts for the specific bulk material you're storing.
The Combustible Dust Pentagon
Here's the thing. A fire needs three elements: fuel, heat, and oxygen. An explosion needs two more: confinement and dispersion. Remove any one of these five, and you're safe. A silo naturally provides the confinement. Your job is to control the other four.
Fuel, Oxidant, and Ignition
Bulk solids like coal, cement, and fly ash are the fuel. The oxygen is already in the air. The ignition source is the wildcard. It could be a static discharge, a hot bearing, or a smoldering ember dropped in with the material. The Minimum Ignition Energy (MIE) for coal dust is around 30 to 50 millijoules. A static spark from a poorly grounded conveyor belt? That's 200 millijoules. You do the math.
I was on a site in Vietnam where the dust layer on the cable trays was 3mm thick. That's a secondary explosion waiting to happen. A primary blast inside the silo shakes the structure, kicks up that settled dust, and ignites it. The secondary explosion is what levels the building.
Confinement and Dispersion
A silo is a pressure vessel by design, but it's not rated for internal deflagration pressures. The maximum explosion pressure (Pmax) for most industrial dusts sits between 8 and 10 bar(g). A standard steel silo is structurally rated for maybe 0.5 bar(g) of internal pressure. If an explosion occurs, the shell will rupture before the relief devices can react.
The Kst value (deflagration index) tells you how fast the pressure rises. St1 dusts (like cement or grain) have a Kst of 0 to 200 bar·m/s. St2 (like coal or sugar) runs 200 to 300. St3 (like aluminum or reactive chemicals) exceeds 300. The higher the Kst, the faster your mitigation system has to react. You've got milliseconds.
Passive Prevention: Designing the Danger Out
Passive systems don't require sensors or power. They just work. If you get the design right, you don't need active suppression. But you have to be meticulous.
Material Selection and Grounding
Static electricity is the most common ignition source in pneumatic conveying systems. You can't eliminate it, but you can control it. Every metallic component within the silo—ladders, level probes, aeration pads—must be bonded and grounded. Bonding equalizes the electrical potential between objects. Grounding takes that potential to earth.
The resistance from any point on the equipment to the ground must be less than 10 ohms. For the grounding electrode itself, it must be less than 1 ohm. We spec copper-clad steel rods driven 3 meters deep, connected via exothermic welding. No clamps. Clamps corrode. I've seen a grounding clamp fail after 18 months in a coastal plant in Malaysia because of salt spray. The static built up, discharged into the silo headspace, and ignited the methane off-gassing from the coal. The baghouse caught fire. It cost them $40,000 in filter media and three days of downtime.
Inerting and Venting
If you can't eliminate the ignition source, eliminate the oxygen. Inerting replaces the headspace oxygen with nitrogen or flue gas. For coal and petcoke silos, you need to keep the oxygen concentration below 8%. For chemical powders, it might need to be below 4%.
The cost of a nitrogen generation system runs $50,000 to $100,000 depending on flow rate. It's expensive. But compare that to the cost of a silo replacement. If inerting isn't feasible, you rely on explosion venting. Venting uses rupture panels that burst at a predetermined pressure (Pstat), usually 0.5 to 1.0 bar(g), directing the blast flame out of the silo before the shell fails.
Active Mitigation: When Prevention Fails
Active systems detect the explosion in its infancy and suppress it. They're fast. They have to be. The pressure rise in a St2 dust explosion can hit 10 bar(g) in under 100 milliseconds.
Explosion Venting vs. Suppression
Venting is passive. Suppression is active. A suppression system uses optical detectors to sense the pressure rise or infrared radiation. It triggers a high-rate discharge (HRD) bottle that floods the silo with suppressant—usually monoammonium phosphate—in under 50 milliseconds. The suppressant absorbs the heat and smothers the flame.
But suppression has a flaw. It only works if the suppressant can mix with the dust cloud before the pressure exceeds the silo's structural limit. If the dust is deep inside a 5,000-tonne silo, the suppressant might not reach it in time. Venting is more reliable for large volumes, but it shoots a fireball out of the silo. You need a safe discharge area, which isn't always available in a congested plant.
Chemical Isolation
An explosion in the silo is bad. An explosion that travels down the pneumatic conveying line into the dust collector is catastrophic. You need isolation. A rotary valve at the silo outlet acts as a mechanical barrier, but it's not enough. The flame can pass through the valve clearances.
You need chemical isolation. An HRD barrier installed on the inlet and outlet piping fires a suppressant cloud into the pipe the moment the detector senses a pressure spike. It creates a wall of chemical foam that stops the flame front. Without isolation, you're just moving the explosion to the next piece of equipment.
Operational Protocols: The Human Factor
You can design the perfect system, and a contractor will install a bypass switch for the suppression system because "it keeps tripping." Or an operator will prop open the access door to clear a blockage. The human factor is the weakest link.
Housekeeping and Ignition Source Control
Dust layers thicker than 1/32 of an inch (0.8mm) are a secondary explosion hazard. Period. Housekeeping isn't about looking clean; it's about removing the fuel. Use explosion-proof vacuum systems. Never use compressed air to clean dust. Compressed air just disperses the dust into a cloud, creating the exact conditions for an explosion.
Hot work permits are non-negotiable. A welding spark has an MIE of essentially zero. It will ignite anything. I remember a commissioning in Malaysia. The suppression system fired during a false alarm. The HRD bottle discharged 4kg of ABC powder into the silo. Took us 16 hours to clean out the mess. The client was furious, but the system worked exactly as designed. The false alarm was caused by a contractor welding near the optical detector without a permit.
Maintenance and Inspection Cycles
Vent panels are single-use. If they burst, you replace them. But they can also fail prematurely. In Saudi Arabia, 45°C ambient temperatures caused the vent panels to warp from thermal expansion. The warping created a 2mm gap. Moisture got in, rusted the panel, and reduced the burst pressure by 30%. We had to spec stainless steel panels with a 2mm gap tolerance and silicone gaskets.
Check your grounding connections quarterly. Check your HRD bottles annually. The propellant in an HRD bottle is nitrogen at 60 bar. If the seal leaks, the pressure drops, and the bottle won't fire. A quarterly bolt-torque check took our crew four hours. It added seven years to that silo's service life. The math works.
Don't guess the vent area. Use the EN 14491 formula:
A = (Kst * V^(2/3)) / (Pstat * C). For a 3,000 m³ coal silo with a Kst of 150 bar·m/s and a Pstat of 0.5 bar(g), you need roughly 1.2 m² of vent area. If you're venting into a duct, add 0.5 m² for every meter of duct length. If you're venting to a safe area, ensure the blast zone is clear of personnel and equipment for at least 15 meters.
Case Study: 5,000-Tonne Coal Silo in Indonesia
A cement plant in Kalimantan was storing coal in a 5,000-tonne silo. The coal had a Kst of 150 bar·m/s and an MIE of 40 mJ. The plant had no suppression system, no isolation, and the grounding was done with galvanized clamps that had corroded. A static discharge ignited the headspace. The pressure blew the roof off the silo. The fire spread to the baghouse. Total loss: $1.2 million.
We redesigned the system. We installed 3 x 0.4m² vent panels on the roof, discharging into a safe area 20 meters from the silo. We added an HRD suppression system with optical detectors and a 4kg suppressant bottle. We installed chemical isolation barriers on the inlet and outlet ducts. We replaced the grounding with exothermic-welded copper-clad steel rods. Total cost of the mitigation system: $47,000. That's 4% of the silo's replacement cost. The plant has been running for six years without an incident.
FAQ
What is the difference between explosion venting and suppression?
Venting is passive. It uses rupture panels that burst at a set pressure, directing the flame out of the silo. Suppression is active. It uses sensors to detect the explosion and fires a chemical suppressant to smother the flame before the pressure builds. Venting is cheaper and more reliable for large volumes, but it requires a safe discharge area. Suppression is better for congested plants, but it requires maintenance.
How often should I test my grounding system?
Quarterly. Use a megohmmeter to measure the resistance from the equipment to the ground. It must be less than 10 ohms for bonding, less than 1 ohm for the grounding electrode. If the resistance climbs, check for corrosion at the connections. Replace clamps with exothermic welds.
Can I use a standard pressure relief valve for dust explosions?
No. Standard relief valves are designed for gas or liquid. Dust is slow-moving and can clog the valve seat. You need a rupture panel—a thin metal sheet designed to burst at a precise pressure. The panel must be certified to EN 14491 or NFPA 68. A standard valve won't open fast enough.
Protect Your Plant with Manxing
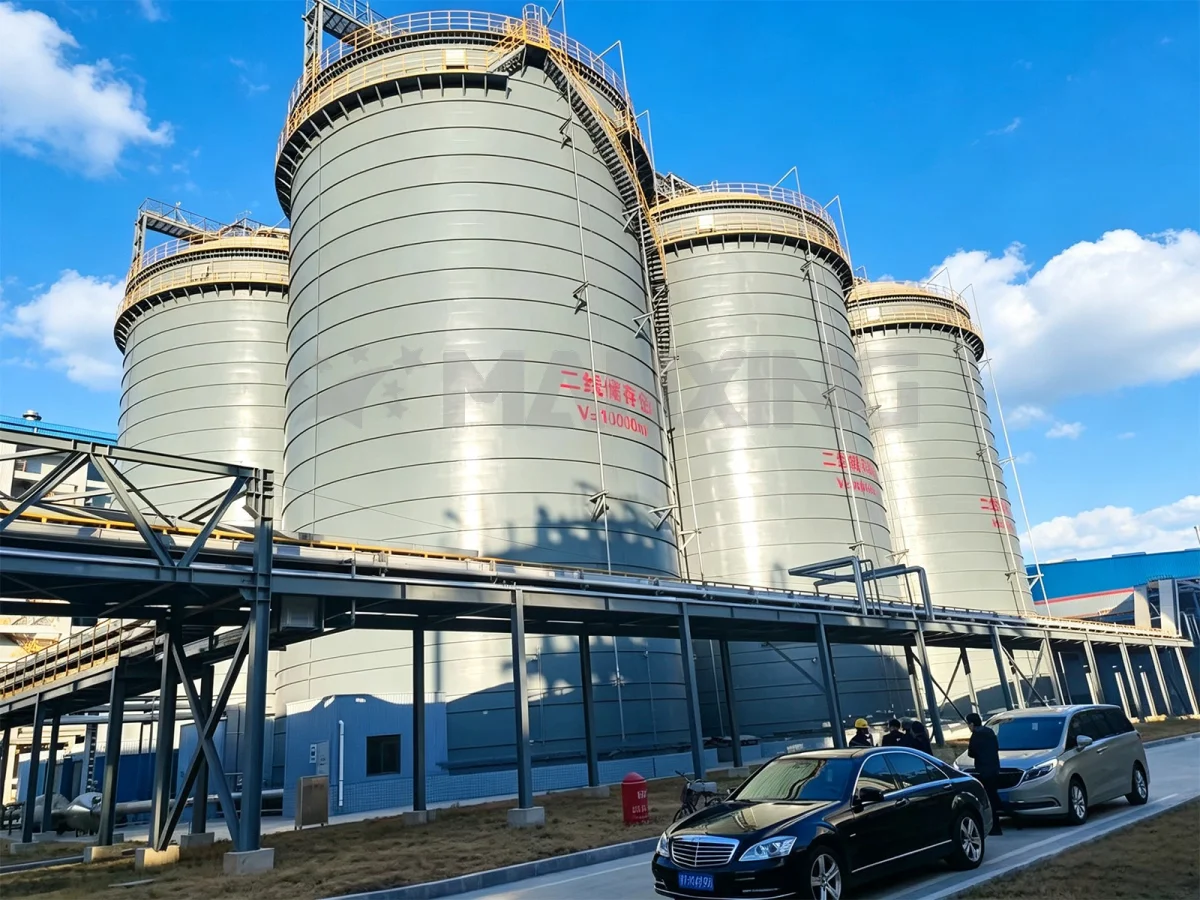
At Manxing, we've designed silo systems across 30+ countries for cement, clinker, fly ash, coal, and slag plants. We don't just sell steel. We engineer safety. Our EPC contracts include full dust explosion risk assessments, vent area calculations, grounding design, and suppression system integration—all compliant with EN 14491, ISO 15012, and ISO 21873.
Don't wait for a 2am phone call about a blown roof. Contact Manxing today for a site-specific dust explosion prevention audit. We'll give you the numbers, the design, and the peace of mind.