


Rust Prevention and Repair for Industrial Silos: A Field Engineer's Guide
Steel silos corrode — that's not a question, it's a timeline. The real question is whether you're managing that timeline or letting it manage you. After fifteen years of specifying coating systems, watching blast profiles under a flashlight at midnight, and signing off repairs on silos from Shandong to Saudi Arabia, I can tell you this: rust prevention isn't about the paint. It's about the preparation, the specification, and the discipline to inspect when nobody's watching. Here's what actually works.
1. Understanding Why Industrial Silos Corrode Faster Than You Think
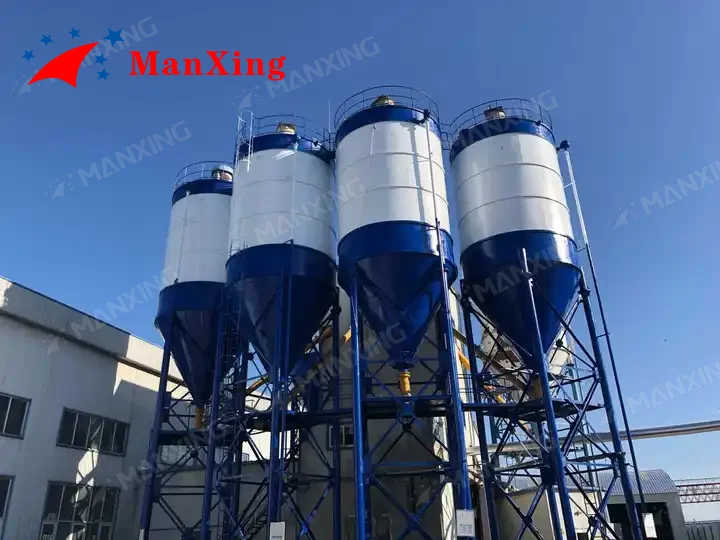
The Electrochemical Process Nobody Explains at the Bid Stage
Corrosion isn't rust appearing on steel. It's an electrochemical cell forming on your silo wall — anode, cathode, electrolyte, metallic path. All four have to exist. Remove one, and the reaction stops. That's the entire science, right there.
Inside a cement silo, you've got condensation cycling between 40°C and 15°C depending on ambient conditions and material temperature. That condensation is your electrolyte. The steel itself provides the metallic path. Oxygen dissolves into the moisture film. And any scratch through your coating system? That's your anode, sacrificing itself to protect the surrounding cathode. The math is brutal: a 2 mm pit in a 10 mm wall plate at 3,000 microamps per square centimeter can penetrate through in under four years.
I've seen it happen faster. A fly ash silo in Jiangsu — commissioned in 2018, first wall thickness readings in 2021 showed 1.3 mm loss on the lower ring. The coating had been applied over mill scale that looked solid but wasn't. Three years. That's all it took.
Material-Specific Corrosion Rates You Need to Know
Not all stored materials are equal enemies. Coal is relatively benign if it stays dry — corrosion rates around 0.05 to 0.1 mm per year on uncoated carbon steel. But coal absorbs moisture, and once the relative humidity inside the silo crosses 60%, that rate triples. Chloride content in the coal accelerates it further. I've measured 0.4 mm per year on coal silos in coastal Guangdong where the coal itself carried 0.15% chloride by weight.
Slag is worse. The sulfur compounds in granulated blast furnace slag create acidic condensation when humidity cycles. We've documented corrosion rates of 0.2 to 0.35 mm per year on uncoated interior surfaces. Fly ash sits somewhere in the middle — the alkalinity actually helps, passivating the steel surface to some degree, but carbonation from absorbed CO2 breaks that passivation down over time.
Cement? The calcium hydroxide in cement dust creates a naturally alkaline environment, pH 12 to 13, which passivates steel. But that same alkalinity attacks zinc-rich primers through saponification. So your coating system has to be chosen for the material, not just the environment. This is where generic specifications fail.
Environmental Accelerators Beyond the Stored Material
External corrosion is a different animal. Coastal sites — within 5 km of open sea — deliver chloride deposition rates of 300 to 600 milligrams per square meter per day. That's enough to break down most single-coat systems within five years. Industrial zones with SO2 emissions create sulfuric acid micro-environments on exterior surfaces. I've seen exterior silo walls in Hebei province lose 0.15 mm per year from acid deposition alone, before you even factor in UV degradation of the coating.
Temperature cycling matters more than people realize. A silo in Inner Mongolia swings from -30°C in winter to 35°C in summer. That's a 65-degree range, and the steel expands and contracts at 12 microstrains per degree Celsius. Over a 30-meter diameter silo, that's 22 mm of circumferential movement per cycle. Coatings that can't flex with that movement crack. Water gets in. And then you're back to the electrochemical cell.
2. Surface Preparation: The Step That Makes or Breaks Everything
Abrasive Blasting Standards and What They Actually Mean
Here's the thing. You can specify the best coating system money can buy — a 300-micron epoxy novolac at $45 per square meter — and it'll fail in two years if the surface prep is wrong. The coating is only as good as the steel it's bonded to. Full stop.
ISO 8501-1 defines blast cleaning grades. Sa2½ — "very thorough blast cleaning" — is the minimum I'll accept for any interior silo coating. Every square millimeter of the surface shall be free from visible oil, grease, mill scale, rust, and foreign matter, with any remaining residues showing only slight staining. That's the standard. In practice, I've watched crews in Vietnam blast to what they called Sa2½, and under a flashlight at a 30-degree angle, you could still see mill scale shadows on 40% of the surface. That coating failed in eighteen months.
For aggressive environments — coastal, high-humidity, acidic material contact — I specify Sa3. "White metal." No mill scale, no rust, no shadows. The surface is uniformly metallic grey. It costs more. Blasting to Sa3 takes roughly twice as long as Sa2½ because the crew has to make multiple passes. But on a 5,000-square-meter silo interior, the difference in coating life is typically eight to twelve years versus three to five. The math works.
Surface profile matters too. Most epoxy coatings need a anchor profile of 50 to 75 micrometers — that's the peak-to-valley height of the blasted surface, measured with replica tape per ISO 8503-1. Too smooth, and the coating has nothing to grip. Too sharp, and the peaks poke through the coating film, creating initiation points for corrosion. I've seen crews use the wrong grit size — 0.8 mm instead of the specified 0.4 mm — and produce a profile of 110 micrometers. The coating looked fine for six months. Then it started peeling in sheets.
Chemical Preparation Methods When Blasting Isn't Practical
Sometimes you can't blast. Retrofit work on an operating silo, for example, where dust from blasting would contaminate the stored material. Or confined spaces where abrasive recovery is impractical. In those cases, you're looking at chemical methods — acid pickling, phosphating, or high-pressure water jetting.
High-pressure water jetting at 2,500 to 3,000 bar can achieve a WJ2 rating per SSPC-SP12/NACE No. 5 — "very thorough water jetting." It removes mill scale and rust without embedding abrasive particles into the surface. The catch: you have to flash-rust the surface immediately after, or coat within hours. Flash rusting — that light orange dusting that appears on wet blasted steel — is acceptable up to a "light" rating per ISO 8501-4. Anything heavier, and you're jetting again.
I remember a project in Malaysia where we had to recoat the interior of a 2,000-tonne cement silo without taking it out of service. We used vacuum-attached water jetting rigs, worked in 12-hour shifts, and coated within four hours of each section being cleaned. The ambient temperature was 34°C with 85% humidity. The flash rusting was relentless. We ended up using a tannin-based rust converter as an intermediate step — not ideal, but it worked. That silo is still in service eight years later.
The Moisture Trap Problem
One detail that kills more coating systems than I can count: moisture trapped in bolt holes, behind stiffeners, and in lap joints. You blast the flat surfaces to beautiful white metal, apply your coating, and six months later you've got rust bleeding out from behind a stiffener that was never properly cleaned.
The fix is tedious but non-negotiable. Every bolt hole gets cleaned with a rotary brush. Every lap joint gets blown out with dry compressed air before coating. Stiffener backs get blasted individually with a right-angle head. On a large silo with 200 stiffeners, this adds maybe two days to the preparation schedule. Skipping it costs you the entire coating system.
3. Protective Coating Systems That Actually Last
Epoxy-Based Systems: The Workhorse
For most industrial silo interiors, a two-coat epoxy system is the baseline. Primer at 75 to 100 microns DFT (dry film thickness), finish coat at 150 to 200 microns. Total system: 225 to 300 microns. That'll give you eight to twelve years in a moderate environment — dry material, interior location, temperature cycling under 40°C.
For aggressive environments, I step up to epoxy novolac or epoxy phenolic. These are chemically resistant to acids, alkalis, and solvents. A novolac system at 350 to 400 microns total DFT handles sulfuric acid condensation from slag storage, alkaline environments from cement, and moderate solvent exposure. Cost is higher — $35 to $55 per square meter applied, depending on access complexity — but the service life jumps to fifteen to twenty years.
The application window is tight. Most epoxy systems have a pot life of 30 to 60 minutes at 25°C. At 35°C, that drops to 15 to 25 minutes. I've watched crews in the Middle East mix batches too large, watch the material skin over in the pot, and then trowel half-cured epoxy onto a silo wall. It looked fine. It wasn't. The intercoat adhesion was compromised, and the system delaminated within two years.
Zinc-Rich Primers: When and When Not to Use Them
Zinc-rich primers — organic or inorganic — provide cathodic protection to the steel. The zinc particles, at 85% by weight in the dry film, sacrificially corrode before the steel does. Inorganic zinc silicate (ethyl or isocyanate-cured) is the standard for structural steel and silo exteriors.
Here's the catch I mentioned earlier: zinc and high alkalinity don't mix. In cement and lime silos, the pH of condensation can reach 12.5 to 13. Zinc reacts with alkali to form soluble zincates — saponification. The primer breaks down, loses adhesion, and the steel corrodes underneath. For cement silo interiors, I don't use zinc-rich primers. Ever. I go straight to an epoxy system on bare steel.
For exteriors and for silos storing neutral materials — coal, aggregates, alumina — inorganic zinc silicate at 75 microns DFT under an epoxy intermediate and polyurethane topcoat is a solid system. Twenty-plus year service life in moderate environments. The key is the recoat window: inorganic zinc must be topcoated within a specific timeframe, usually 48 hours to 72 hours for ethyl silicate, before the surface becomes too cured for intercoat adhesion. Miss that window, and you're solvent-washing or sweep-blasting the entire surface.
Polyurethane and Fluoropolymer Topcoats for Exterior Durability
UV radiation destroys epoxy. Leave an epoxy topcoat in direct sunlight for two years,— it chalks, loses gloss, and eventually erodes. For exterior silo surfaces, the topcoat needs to be UV-stable. Aliphatic polyurethane is the standard — 50 to 75 microns over an epoxy intermediate coat. It holds color and gloss for ten to fifteen years.
For extreme UV environments — high-altitude sites, equatorial locations — fluoropolymer topcoats (PVDF or FEVE) are worth the premium. They cost two to three times as much as polyurethane, but they'll hold gloss and color for twenty-five years. I specified a PVDF system on a cluster of alumina silos in Qatar where summer surface temperatures hit 65°C. Fifteen years later, the gloss retention is still above 80%. The polyurethane system on an adjacent building? Replaced twice.
4. Cathodic Protection for Silo Foundations and Floors
Sacrificial Anode Systems
Silo floors and foundation rings are the most neglected corrosion zone in the entire structure. Material sits on the floor, moisture wicks up from the ground, and the concrete-to-steel interface becomes a corrosion cell. For silos on shallow foundations, I specify a sacrificial anode system — magnesium or zinc anodes embedded in the foundation ring.
A typical 3,000-tonne cement silo on a ring foundation needs 8 to 12 magnesium anodes, each 14.5 kg, spaced evenly around the perimeter. They provide 100 to 110 millivolts of protection potential to the steel, measured against a copper-copper sulfate reference electrode per NACE SP0169. The anodes last eight to fifteen years depending on soil resistivity. In low-resistivity soils — below 5,000 ohm-centimeters — they corrode faster and need replacement sooner.
The connection is critical. Each anode must be electrically bonded to the silo structure with a copper cable, exothermically welded or bolted to a test point. I've seen installations where the cables were simply laid in the soil next to the anode with no connection to the structure. Zero protection. The anodes corroded uselessly while the foundation steel rusted.
Impressed Current Systems for Large Installations
For multi-silo facilities — a cement plant with six or more silos on a common foundation mat — impressed current cathodic protection is more economical than sacrificial anodes. A single rectifier, outputting 5 to 20 amps at 12 to 24 volts DC, protects the entire foundation system through a network of mixed-metal oxide anodes.
The design is site-specific. Soil resistivity measurements per IEEE Standard 81, structure-to-soil potential surveys, and current demand calculations per NACE SP0102. A typical system for a six-silo cluster costs $15,000 to $30,000 installed, with annual operating costs of $2,000 to $4,000 for electricity and monitoring. Compared to the cost of foundation repair — $200,000 to $500,000 for a full foundation ring replacement — it's a rounding error.
5. Repair Techniques for Corroded Silo Structures
Welded Patch Repairs: When and How
When wall thickness drops below the minimum required by EN 1993-4-1 (Eurocode 3, Part 4-1 for silos), you have three options: patch, reinforce, or replace. Patch repair is the most common for localized corrosion — pitting, edge corrosion at lap joints, or corrosion behind stiffeners.
The patch plate must be the same grade as the original steel, minimum 6 mm thick for structural patches, and the weld must be full-penetration per AWS D1.1. Before welding, you cut back the corroded area to sound metal — minimum 50 mm beyond the visible corrosion boundary. I've seen crews weld a patch over a corroded area without cutting back. The corrosion continued underneath the patch, invisible, until the patch fell off.
After welding, the patch area gets the same surface preparation and coating system as the original. If the original was coated, the patch area gets recoated to match. If the original was uncoated — common in older silos — the patch gets a full coating system, and you should seriously consider coating the entire silo while you're at it.
Composite Wrap Systems for Non-Weld Repairs
Welding inside a silo that's stored combustible material — coal, fly ash, grain dust — is a fire and explosion risk. Hot work permits, gas monitoring, fire watch, the whole protocol. For these situations, composite wrap systems using carbon fiber or glass fiber reinforced polymers (CFRP/GFRP) are a viable alternative.
A CFRP wrap at 1.2 mm thickness provides approximately 150 MPa of hoop strength — enough to restore structural capacity to a wall section that's lost 30% of its thickness to corrosion. The surface prep is still critical: the steel must be cleaned to Sa2½, and any pits deeper than 3 mm must be filled with epoxy putty before wrapping. The composite is applied in layers, each layer wetted with saturating resin, with a minimum of 50% fiber volume fraction.
I specified CFRP wraps on a coal silo in Shanxi where the lower three rings had lost 2.5 mm from a nominal 10 mm wall. The alternative was full ring replacement — six weeks of downtime, $180,000 in steel and labor. The wrap repair took four days, cost $45,000, and restored the wall to its original design capacity. That was seven years ago. The wraps are still holding.
Bolted Reinforcement for Structural Stiffeners
When stiffeners corrode — and they always do, because they're the last thing anyone thinks about during coating — bolted reinforcement is faster and safer than welding. Angle sections or channel sections are bolted to the existing stiffener with high-strength friction grip bolts per EN 14399.
The bolt pattern is designed to transfer the full design load through friction between the new and existing steel. Surface contact areas must be cleaned to Sa2½ and coated with a zinc-rich primer to maintain the friction coefficient — typically 0.40 to 0.50 for Class A preparation per EN 1090-2. I've seen installations where the contact surfaces were left bare, and the friction coefficient dropped to 0.25. The bolts loosened within a year.
6. Inspection and Maintenance: The Discipline Nobody Wants
Ultrasonic Thickness Testing
You can't manage what you don't measure. Ultrasonic thickness testing (UTT) per EN 14127 is the standard method for monitoring wall loss. A calibrated probe, coupled to the steel with gel, measures wall thickness to ±0.1 mm accuracy. On a large silo, I specify a grid pattern: one reading every 500 mm vertically and every 1,000 mm circumferentially on the lower three rings, where corrosion is most aggressive.
Frequency: annually for the first three years after commissioning, then every two years if readings are stable. If wall loss exceeds 0.2 mm per year, increase frequency to annual and consider recoating or structural reinforcement. I've seen plants skip UTT for five years because "the silo looks fine." When they finally measured, the lower ring had lost 4 mm from a 12 mm wall. That's a third of the structural capacity, gone.
Coating Failure Analysis
When coatings fail, the failure mode tells you the cause. Blistering at the steel-coating interface? That's osmotic blistering — soluble salts on the surface before coating. Peeling in sheets with good adhesion to the steel but poor intercoat adhesion? That's overcoating beyond the recoat window. Cracking in a pattern that follows the steel surface profile? That's brittleness — wrong coating for the thermal cycling environment.
Each failure mode has a specific remedy. Salt contamination requires re-blasting. Overcoating failure requires removal to bare steel and re-coating. Brittleness requires a different coating system entirely. Patching over a failed coating without diagnosing the cause is throwing money away. The new coating will fail the same way.
Maintenance Scheduling That Actually Gets Done
The best maintenance plan in the world is worthless if it sits in a binder. I build maintenance schedules around existing plant shutdowns — the annual kiln shutdown, the quarterly mill maintenance window. Coating touch-up during a scheduled shutdown costs 30% less than an emergency callout because you're not paying for mobilization and expedited material delivery.
For exterior coatings, a five-year cycle works: visual inspection annually, detailed inspection with DFT measurement and adhesion testing (pull-off per ISO 4624) at year five. For interior coatings, inspection during every material change-out or at least every three years. The cost of a thorough interior inspection — scaffolding, lighting, surface cleaning, DFT measurement — runs $8,000 to $15,000 for a medium silo. The cost of an unplanned coating failure — emergency shutdown, material disposal, full recoat — runs $150,000 to $400,000. The math isn't close.
Case Study: Fly Ash Silo Recoating — Vietnam, 2022
A 4,000-tonne fly ash silo at a power plant in northern Vietnam had been in service for eleven years. The original coating — a single-coat epoxy at 200 microns — was failing extensively. Blistering covered 35% of the interior surface, and wall thickness measurements showed an average loss of 0.8 mm in the lower rings, with isolated pits at 2.5 mm depth.
We specified full interior recoating: abrasive blast to Sa3, two-coat epoxy novolac system at 350 microns total DFT, with a polyurethane exterior topcoat at 75 microns. The project took 22 days — 8 days for blasting, 10 days for coating, 4 days for inspection and touch-up. Ambient conditions were challenging: 32°C average, 80% humidity, with two tropical rain events that delayed exterior work by a day each.
The crew worked in two shifts to maintain the coating application window. DFT readings averaged 365 microns on the interior, 82 microns on the exterior. Pull-off adhesion tests averaged 8.5 MPa — well above the 5 MPa minimum specified. Total project cost was $127,000, including scaffolding, surface preparation, coating materials, and inspection. The plant manager told me the previous recoating quote he'd received — from a contractor who specified Sa2½ and a single-coat system — was $68,000. He went with us. That silo is now on a ten-year inspection cycle, and the first check at year two showed zero coating defects.
Frequently Asked Questions
Q: How often should industrial silo coatings be inspected?
Exterior coatings: visual inspection annually, detailed inspection with DFT and adhesion testing every five years. Interior coatings: inspect during every material change-out or at least every three years. If the stored material is corrosive — slag, coal with high chloride, chemical powders — increase interior inspection frequency to annually. The cost of inspection is trivial compared to the cost of an unplanned failure.
Q: Can you coat over an existing failed coating, or does it need to be removed?
It depends on the failure mode. If the existing coating is well-adhered but just aged — chalking, fading, minor cracking — you can clean, abrade, and apply a compatible topcoat. If the failure is blistering, delamination, or peeling, you must remove the failed coating to bare steel before recoating. Coating over a failed system is a temporary fix at best. I've seen it done. It never lasts more than two years.
Q: What's the expected service life of a properly specified coating system on an industrial silo?
For a two-coat epoxy system at 250 to 300 microns DFT on a properly prepared surface (Sa2½ or better) in a moderate environment: eight to twelve years. For an epoxy novolac system at 350 to 400 microns in an aggressive environment: fifteen to twenty years. For an exterior system with inorganic zinc primer, epoxy intermediate, and polyurethane topcoat: twenty to twenty-five years. These numbers assume proper application, proper DFT, and no surface preparation shortcuts. Cut corners, and you're looking at three to five years regardless of what the coating data sheet claims.
Protect Your Silo Investment with Manxing
At Manxing, we've designed, built, and maintained silo systems across thirty-plus countries. We know that coating failure isn't a materials problem — it's a specification and execution problem. Our EPC contracts include surface preparation standards, coating system specifications, DFT verification protocols, and post-commissioning inspection schedules. We don't just build silos. We build silos that last.
If you're planning a new silo project, a recoating campaign, or a structural assessment of an existing silo, talk to our engineering team. We'll give you a straight answer — no generic specifications, no one-size-fits-all coating recommendations, and no surprises at the commissioning stage.
Contact Manxing's silo engineering team today for a project assessment: www.manxingstorage.com