


The Brutal Truth About Silo Inspection: Schedules, Checklists, and What Actually Saves Your Silo
How often should you inspect an industrial silo? At minimum, walk it daily, measure it quarterly, and audit it annually. What should you check? Shell deformation, cone abrasion, and bolt torque—in that order. Most plants treat their silos like furniture. They don't. A 3,000-tonne concrete monolith sitting under dynamic load is a living, breathing structure. Ignore it, and it will fail.
Why Silos Fail When You Stop Looking
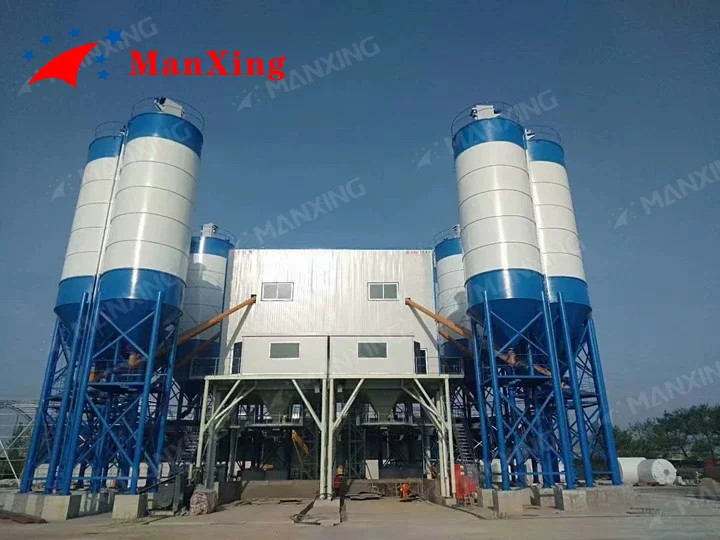
The Physics of Neglect
Bulk solids aren't static. They shift. Janssen's theory explains how vertical pressure converts to lateral pressure against the shell, but real-world bridging and rat-holing create asymmetric loads nobody calculated for. I was on a site in Vietnam where the operator swore the silo was fine. The shell was bulging 40mm out of round. They'd ignored it for 18 months. That asymmetry buckled the stiffeners within a week of our visit.
You can't see stress. You see the aftermath. A longitudinal crack doesn't mean the steel is tired. It means the load path has changed. When material bridges across the silo diameter and then collapses, it generates an impact load 3.5 times the static weight. Your shell wasn't designed for that. Nobody's is.
Abrasion and Corrosion
Coal and slag eat steel. In high-slag environments, we see 3mm wall loss per year near the discharge cone. You can't eyeball that. You need ultrasonic thickness testing. Standard EN 1991-1-1 gives you the load factors, but it doesn't account for localized wear that turns 12mm plate into 6mm scrap.
Corrosion works differently. It's insidious. Condensation on the interior roof deck drips onto the material surface. In a cement silo, that creates a 200mm thick ring of hardened crust. That crust adds 15 tonnes of dead weight to the shell wall. It also blocks your aeration pads. You get a discharge shutdown, and you're wondering why your 5,000-tonne silo is acting like a 500-tonne silo.
The Domino Effect
One failed component triggers the next. A torn aeration pad dumps air into the material prematurely. The material fluidizes unevenly. You get a side discharge, which pushes the shell wall laterally. The shell pushes the stiffener. The stiffener pulls the bolt. The bolt fails. Now you have a 2-meter tear in your cone. This takes about three months if you're unlucky. I've seen it happen in six weeks during a monsoon season.
Building the Inspection Schedule
Daily Walkdowns
Fifteen minutes. That's it. Look for dust trails on the shell—they indicate roof leaks or seal failures. Listen to the aeration fans; a change in pitch means a blocked filter or a torn diaphragm. Check the baghouse differential pressure. If it creeps above 1,200 Pa, you're risking a bag rupture.
Walk the cone. Listen for hollow tapping. That's material build-up detaching from the liner. If you hear it, you've already got a blockage forming. Don't wait for the level gauge to tell you. Level gauges lie. Radar guns read the angle of repose, not the actual volume. A rat-hole inside the silo makes the gauge read 80% when you're actually at 40%.
Quarterly Deep Dives
Get out the tools. Ultrasonic testing at pre-marked points. We specify 20 points per shell ring, minimum. Accuracy down to 0.5mm. Check the fluidizing tiles in the cone. A 2-inch WC pressure drop across the aeration pad means the media is compacting. You'll get bridging within a month.
Inspect the discharge gates. A slide gate that takes 3 seconds longer to open than it did last quarter is binding. The actuator is fighting material ingress into the guide rails. Ignore it, and you'll be cutting the gate out with a torch at 2am.
Annual Structural Audits
This is where you bring in the engineers. Foundation settlement, roof alignment, and weld integrity. Differential settlement exceeding 5mm across the foundation diameter is a red flag. Standard EN 1993 governs the shell design, but it assumes a stable base. If the base moves, the math falls apart.
Check the roof. A 50kPa snow load or 150km/h wind event will find every pinhole in your sealant. Water inside a fly ash silo turns the powder into concrete. I've chipped out 2 tonnes of hardened ash from a single leak. Your dust collector can't handle that moisture either. It blinds the bags. You lose your negative pressure. Now you've got a pressurized silo venting dust into the atmosphere. The EPA doesn't care about your maintenance schedule.
The Field Checklist: What to Measure, Not Just Look At
Shell and Roof Integrity
Check the longitudinal welds first. Circumferential cracks are annoying; longitudinal cracks are fatal. Look at the roof. Water inside a fly ash silo turns the powder into concrete. I've chipped out 2 tonnes of hardened ash from a single leak.
Measure the shell temperature at noon and midnight. A 20°C delta indicates material packed against the wall, blocking airflow. That packed material absorbs moisture. It hardens. You're now breaking concrete with a sledgehammer instead of discharging powder with a fan.
Cones and Discharge Zones
This is where the material moves, and where the steel dies. Measure the angle of repose. If it's steeper than 30 degrees, you've got moisture ingress or particle degradation. Check the liner bolts. A missing M24 bolt at 400 Nm torque means the liner is flapping. That flap acts like a saw, cutting through the shell plate in six months.
Inspect the fluidizing tiles. Cracked tiles dump air into the material bed unevenly. You'll see channeling—material flowing down one side of the silo while the other side stays static. That asymmetry generates a bending moment at the shell-to-cone junction. It's the number one cause of structural failure in cement silos.
Aeration and Dust Collection
Pneumatic conveying lines operate at 2-4 inch WC. If your dust collection system can't keep up, you're pressurizing the silo. ISO 15012 covers dust explosion prevention, but you can't prevent an explosion if your venting is clogged with cement dust. Clean the inlet hoppers. Every time.
Check the relief valves. ASME Section VIII dictates the pressure rating, but a relief valve coated in 5mm of cement dust won't pop at its set pressure. It'll pop at 3 times the set pressure. Or it won't pop at all. Test them manually. Pull the lever. If it doesn't move, replace it.
When the Checklist Screams Red
Cracking Patterns
Not all cracks are equal. A 10mm crack width at the shell-to-cone junction means the structure is yielding. Stop loading immediately. Hairline cracks at the weld toe? Grind them out and re-weld. But if the crack propagates through the parent metal, you're looking at a catastrophic failure.
Mark the ends of the crack with paint. Measure the length every week. If it grows 2mm in a month, you've got a moving load. If it grows 10mm in a week, you've got a collapse in progress. Evacuate the area. Seriously.
Foundation Settlement
We use total stations now, not just spirit levels. A tilt ratio exceeding 1:500 requires grouting. I've seen plants ignore a 1:300 tilt for two years because the silo was "still standing." It was standing on half its base. The other half was suspended, creating a hinge point that cracked the concrete apron.
The fix isn't cheap. You're looking at $45,000 for compaction grouting and three weeks of downtime. But the alternative is a 3,000-tonne silo tipping over. That's a $2,000,000 loss and a year of litigation.
Bolt Torque Failure
In Malaysia, we fought the heat. 40°C on the steel surface. Bolts expand, torque drops. A quarterly retorque of the top 10 ring bolts takes four hours. It prevents a $200,000 roof collapse. The math works.
Use a calibrated torque wrench. Not an impact gun. An impact gun gives you a false sense of security. It reads 400 Nm, but the actual clamp load is 250 Nm because of friction variance. You need the clamp load. The friction is just noise.
Field Tip: Mark your inspection points with weldable studs. Don't rely on paint marks that fade in 6 months of UV exposure. I've seen crews drill into the same spot every year, unknowingly thinning the shell by 0.3mm annually. Drill once, weld a stud, and measure from the stud.
Case Study: The Shandong Fly Ash Silo
A 5,000-tonne fly ash silo in Shandong started showing a 1:280 tilt ratio during a routine annual audit. The plant ignored it for 18 months because the discharge was still working. Eighteen months later, the discharge cone cracked at the 3 o'clock position. Material leaked onto the support structure. We shut it down.
The repair required jacking the silo 12mm back to level, replacing 8 tonnes of structural steel in the cone, and grouting the foundation. Total cost: $45,000 and 21 days of downtime. The quarterly monitoring program we implemented afterward costs $500 per year. The plant manager told me he felt stupid. He shouldn't. He just learned what every silo owner learns eventually.
Frequently Asked Questions
How often should we perform ultrasonic testing on the shell?
Quarterly for high-abrasion materials like slag, coal, and alumina. Annually for cement and fly ash. If you're handling slag with a Mohs hardness above 6, increase the frequency to monthly at the discharge zone. The wear rate isn't linear. It accelerates as the surface roughens.
What is the maximum allowable crack width before we must stop loading?
10mm. Anything wider requires immediate structural assessment. If the crack is at the shell-to-cone junction, stop loading at 5mm. That junction is your primary load path. A failure there doesn't leak material. It drops the silo.
Can we inspect a silo while it's full?
Yes, for visual and acoustic checks. But ultrasonic testing and internal inspections require emptying the silo. You can't UT through material, and you can't see the cone liner through 3,000 tonnes of powder. Schedule your internal inspections during planned plant shutdowns. Don't wait for a failure to force the shutdown.
Protect Your Investment with Manxing
At Manxing, we don't just build silos. We engineer maintenance into the design. Our EPC contracts include detailed inspection schedules, pre-marked UT points, and accessible aeration systems. We've commissioned projects across 30+ countries, and we've learned that a silo is only as good as its maintenance program.
Don't wait for the 2am phone call. Contact Manxing today to schedule a structural audit or discuss your next bulk material storage project. We'll make sure your silo stands for decades, not just years.