


Silo Maintenance Cost Optimization: What Actually Works (And What Doesn't)
A well-maintained industrial silo costs between $0.80 and $2.10 per tonne of stored material annually. A neglected one? That number jumps to $6–15 per tonne once you factor in emergency repairs, product loss, and unplanned downtime. The biggest savings don't come from cutting maintenance — they come from doing the right maintenance at the right time, guided by actual condition data instead of a calendar.
The Real Cost of Silo Maintenance — Beyond the Spreadsheet
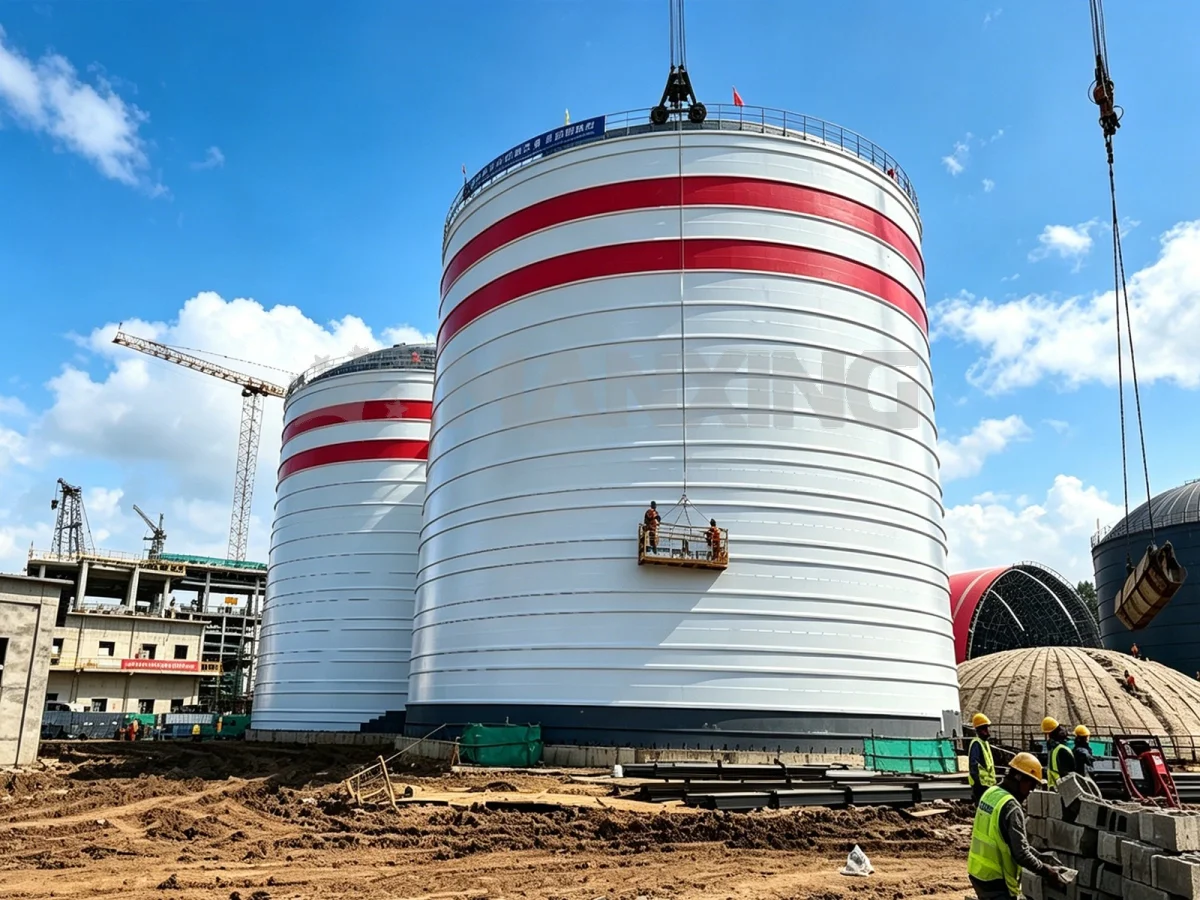
What a "normal" maintenance budget looks like
I've reviewed maintenance budgets across 40+ cement and slag plants in the last decade. The ones running efficiently — not the ones spending the most — allocate roughly 2.5–3.5% of the silo's total installed cost per year. For a 5,000-tonne cement silo that cost $1.2 million to build, that's $30,000–$42,000 annually. That covers scheduled inspections, bolt re-torquing, coating touch-ups, aeration system servicing, and dust collector filter changes.
Here's where it gets interesting. Plants that spend less than 1.5% per year almost always end up spending 5–8% within three years. Deferred maintenance on a silo isn't like deferring an oil change on your car. It's like ignoring a crack in a dam wall — the consequences compound exponentially.
The hidden costs nobody budgets for
Product degradation is the silent budget killer. I walked into a clinker storage facility in Vietnam where the silo's aeration system had been running at 40% capacity for eight months. The material had compacted into a 2-metre rat-hole that reduced effective storage from 8,000 tonnes to roughly 5,200. They were paying to store air. The lost capacity alone cost them $180,000 in unnecessary trucking and re-handling over that period.
Then there's the regulatory angle. Under EN 14491 for dust explosion protection, your explosion vent panels and suppression systems have mandatory inspection intervals. Miss those, and you're not just risking a fine — you're risking the entire facility. I've seen a single missed inspection on a coal silo's explosion panel result in a $340,000 insurance claim denial after a minor deflagration event. The panel had corroded shut. It wouldn't have cost $200 to replace.
Predictive vs. Reactive: The Maintenance Strategy That Pays for Itself
Why time-based maintenance wastes money
The default approach in most plants is calendar-based: inspect every six months, replace filters every year, re-torque bolts every two years. It's simple. It's also wasteful. A cement silo in a dry climate with low humidity might have bolt connections that are perfectly fine after five years. The same silo in a coastal plant in Indonesia? Those bolts might need attention after 18 months.
Time-based schedules don't account for actual operating conditions. They don't account for material abrasiveness, temperature cycling, humidity, or how often the silo actually cycles between full and empty. A silo that turns over every three days experiences completely different fatigue loading than one that sits at 80% capacity for weeks.
Condition monitoring that actually works
The shift to condition-based maintenance isn't glamorous, but the numbers are hard to argue with. We installed vibration sensors on the rotary valve drives at a slag grinding plant in Shandong. Within four months, the data showed a bearing on one valve was trending toward failure — vibration amplitude had increased from 2.1 mm/s to 6.8 mm/s. They scheduled a replacement during a planned 8-hour shutdown. Total cost: $1,200 for the bearing and four hours of labor.
Six months later, the same bearing on a parallel valve showed the same trend. Same fix, same cost. Without monitoring, those bearings would have failed catastrophically — each failure costing $8,000–$12,000 in emergency repair, lost production, and material spillage. The monitoring system paid for itself twice over in the first year.
For structural monitoring, ultrasonic thickness testing on shell plates is the single highest-ROI inspection you can do. A 15-minute UT scan on a weld seam costs maybe $50. Finding a 30% wall loss before it becomes a leak? That's a $200,000 repair avoided. We specify UT testing at 24-month intervals for cement and fly ash silos, and 12-month intervals for abrasive materials like slag and coal.
Structural Maintenance: The Details That Prevent Catastrophic Failure
Bolt torque and connection integrity
This is the one that keeps me up at night. Bolted silo connections — flange joints, manway covers, roof hatch seals — are the most common failure point I see in the field. And it's almost always preventable.
Under Eurocode 3 (EN 1993-4-1 for silos specifically), bolted connections in tension zones require periodic re-torquing. The standard doesn't give you a fixed interval because it depends on the loading cycle, but in practice, I recommend checking critical connections at 12-month intervals for the first two years, then adjusting based on findings. If you're losing more than 10% of specified torque on a connection, something's wrong — either the gasket is degrading, the bolt is yielding, or the structure is settling.
I remember a project in Malaysia where a 3,000-tonne fly ash silo had been in service for four years with zero bolt maintenance. When we finally got a torque wrench to the flange connections, 30% of the bolts on the lower ring were below 50% of specification. The gasket had compressed and the bolts had relaxed under thermal cycling. We re-torqued the entire ring in two days. Cost: $4,500. The alternative — a flange separation during filling — would have dumped 2,800 tonnes of fly ash across the plant. Cleanup alone would have exceeded $200,000.
Corrosion monitoring and coating life
External corrosion on carbon steel silos follows a predictable pattern if you know where to look. The worst areas are always the same: the roof-to-shell junction, the bottom ring where moisture collects, any area where insulation is damaged, and the inside of the shell above the material level where condensation forms.
A good epoxy coating system — properly applied at 250–300 microns DFT — will last 12–15 years in a moderate industrial environment. In a coastal or high-humidity location, expect 7–10 years. The key is catching coating failure early. Once rust starts under a coating, it spreads laterally faster than it penetrates. A 50mm blister you find today becomes a 2m² delamination zone in 18 months.
We budget $8–$15 per square meter for spot repair and recoating of localized damage. Full external recoating of a 5,000-tonne silo runs $45,000–$70,000 depending on access complexity. Compare that to shell plate replacement, which starts at $150,000 and goes up fast.
Mechanical Systems: Keeping Conveying and Aeration Running
Aeration pad replacement cycles
Aeration pads in a cement silo typically last 3–5 years. In a slag or coal silo, where the material is more abrasive and often has higher moisture content, that drops to 18–30 months. The failure mode is almost always clogging, not physical wear — fine particles migrate into the fabric and restrict airflow until the pad is effectively solid.
The cost of replacing aeration pads is modest: $15–$40 per pad depending on size and material. A typical 5,000-tonne cement silo might have 120–150 pads. Full replacement runs $2,000–$5,000 in materials plus two days of confined space entry labor. But here's the thing — if you let pads go too long, the material compacts against the silo wall. You're not just replacing pads then. You're dealing with a bridging or rat-holing situation that might require manual entry, vacuum trucks, or in extreme cases, cutting an access hole in the cone.
Dust collector maintenance economics
The dust collector is the most maintenance-intensive piece of equipment on any silo system, and it's the one most likely to be ignored until something breaks. Filter bags in a cement silo dust collector last 18–36 months depending on the material and operating hours. Pulse valves fail. Solenoid coils burn out. Diaphragms crack.
A well-maintained dust collector operating at design differential pressure (typically 1,000–1,500 Pa) uses about 30% less compressed air than one running at 2,000+ Pa because the filters are blinded. Over a year, that compressed air savings alone can be $3,000–$8,000 on a single silo. Add in the cost of premature filter replacement — bags that should last 30 months but fail at 18 because of over-pulsing — and you're looking at $5,000–$12,000 in unnecessary annual cost.
Got a call at 2am from a plant in Shandong — baghouse differential pressure had crept to 1,800 Pa. They were 40 minutes from a shutdown. We walked them through cleaning the inlet hoppers on the phone instead of sending anyone. Pressure dropped to 1,100 Pa within an hour. The root cause was a failed pulse valve that had been stuck open for three weeks, continuously pulsing one row of bags while the others blinded. A $90 valve replacement saved them a $15,000 filter change and a production shutdown.
The Maintenance Schedule That Actually Saves Money
Weekly, monthly, annual task breakdown
The most cost-effective maintenance schedule I've seen isn't the most detailed one — it's the one that gets followed. Here's a framework that works for most industrial silos storing cement, fly ash, or slag:
Weekly: Visual inspection of silo exterior, check dust collector differential pressure, verify level sensor readings, listen for unusual sounds from mechanical equipment. Takes 20 minutes. Costs nothing.
Monthly: Inspect aeration system airflow, check bin activator and rotary valve operation, verify load cell calibration (compare indicated weight against known truck weights), inspect roof vent and filter housing. Takes 2–3 hours. Cost: labor only.
Quarterly: Bolt torque spot-check on 10% of accessible connections, inspect coating condition on exterior, test explosion vent panels (visual and functional check per EN 14491), clean dust collector hopper and inspect filter condition. Takes 1–2 days. Cost: $500–$1,500 including any minor parts.
Annually: Full structural inspection including UT thickness testing on shell plates, complete bolt torque survey, internal inspection of cone and outlet areas, dust collector filter replacement (or condition assessment), load cell calibration certification, review and update maintenance records. Takes 3–5 days. Cost: $8,000–$20,000 depending on silo size and access requirements.
Spare parts inventory optimization
Most plants either have too many spare parts (cash sitting on a shelf) or too few (waiting three weeks for a $30 part). The sweet spot is keeping critical spares that have a lead time longer than your maximum acceptable downtime.
For a typical cement silo, that means: one spare rotary valve rotor (lead time 4–6 weeks), one set of aeration pads for the most critical zone (lead time 2–4 weeks), one spare dust collector pulse valve and solenoid kit (lead time 1–2 weeks), and a set of filter bags if your supplier lead time exceeds 4 weeks. Total inventory value: $3,000–$8,000. The cost of not having these parts when you need them: $10,000–$50,000 per day of unplanned downtime.
Case Study: Slag Silo Maintenance Overhaul — Jiangsu Province
A slag grinding plant in Jiangsu had two 4,000-tonne slag silos that were costing them $95,000 per year in maintenance — mostly reactive. Emergency rotary valve repairs, unplanned dust collector shutdowns, and two incidents of material bridging that required manual break-down with pneumatic hammers.
We audited their maintenance program and found three root causes. First, they were running time-based maintenance on a material that's significantly more abrasive than cement — their aeration pad replacement interval was 36 months when it should have been 18. Second, they had no condition monitoring on the dust collector, so filter bags were being replaced on a fixed 24-month schedule regardless of actual condition. Third, their bolt torque hadn't been checked since commissioning three years earlier.
We implemented a condition-based program: vibration monitoring on rotary valves, differential pressure trending on the dust collector, UT testing on the shell plates, and a revised bolt torque schedule at 12-month intervals. Aeration pads were replaced on a 20-month cycle with quarterly airflow checks to catch early clogging.
Year-one results: maintenance costs dropped from $95,000 to $41,000. Zero unplanned downtime events. The dust collector filter bags, which had been replaced every 24 months at a cost of $6,500, lasted 34 months under the new program because we stopped over-pulsing blinded bags. The total investment in monitoring equipment and revised procedures was $12,000. Payback period: four months.
Frequently Asked Questions
How often should I inspect my silo's structural bolts?
For the first two years after commissioning, check critical connections at 12-month intervals. After that, adjust based on findings. If you're losing less than 5% of torque, you can extend to 18–24 months. If you're losing more than 10%, investigate the cause — gasket degradation, bolt yielding, or structural settlement — and shorten the interval. Under EN 1993-4-1, there's no mandated interval, but the standard requires that connections maintain their design preload throughout the service life. That means you have to verify it, not assume it.
What's the most cost-effective maintenance investment for an aging silo?
Without question: ultrasonic thickness testing on the shell plates. A full UT survey of a 5,000-tonne silo costs $3,000–$5,000 and takes two days. It tells you exactly where material loss is occurring and how fast. Without it, you're guessing. I've seen plants spend $40,000 recoating a silo exterior when the real problem was internal corrosion in the upper shell that nobody could see. UT testing prevents exactly that kind of misdirected spending.
Can I reduce dust collector maintenance costs without compromising performance?
Yes, and the biggest lever is differential pressure monitoring. Most dust collectors are pulsed on a fixed timer — say, every 15 seconds regardless of filter condition. That wastes compressed air and shortens bag life. Switching to demand-based pulsing (triggered by differential pressure reaching a setpoint, typically 1,200–1,500 Pa) reduces compressed air consumption by 25–40% and extends filter life by 20–30%. The retrofit cost for a differential pressure controller and modified pulse sequence is $1,500–$3,000. Annual savings on a single silo: $4,000–$10,000.
Get a Maintenance Cost Assessment for Your Silo System
Manxing provides maintenance program audits, condition-based monitoring system design, and full EPC silo maintenance contracts. We've optimized maintenance programs for over 200 industrial silos across cement, slag, fly ash, and coal applications. Tell us what you're storing, how old your silos are, and what your current annual maintenance spend looks like — we'll tell you where the money is leaking.
Contact Manxing Engineering →