


Silo Structural Integrity Assessment: What Every Plant Manager Needs to Know
A structural integrity assessment is a systematic evaluation of a silo's ability to safely carry its design loads — including material pressure, wind, seismic forces, and its own weight — without failure. It matters because a silo collapse doesn't just cost money; it kills people. I've seen a 4,000-tonne clinker silo go from "looks fine" to catastrophic buckling in under 90 seconds. The assessment caught nothing because nobody looked in the right places.
Why Silo Structural Integrity Degrades Over Time
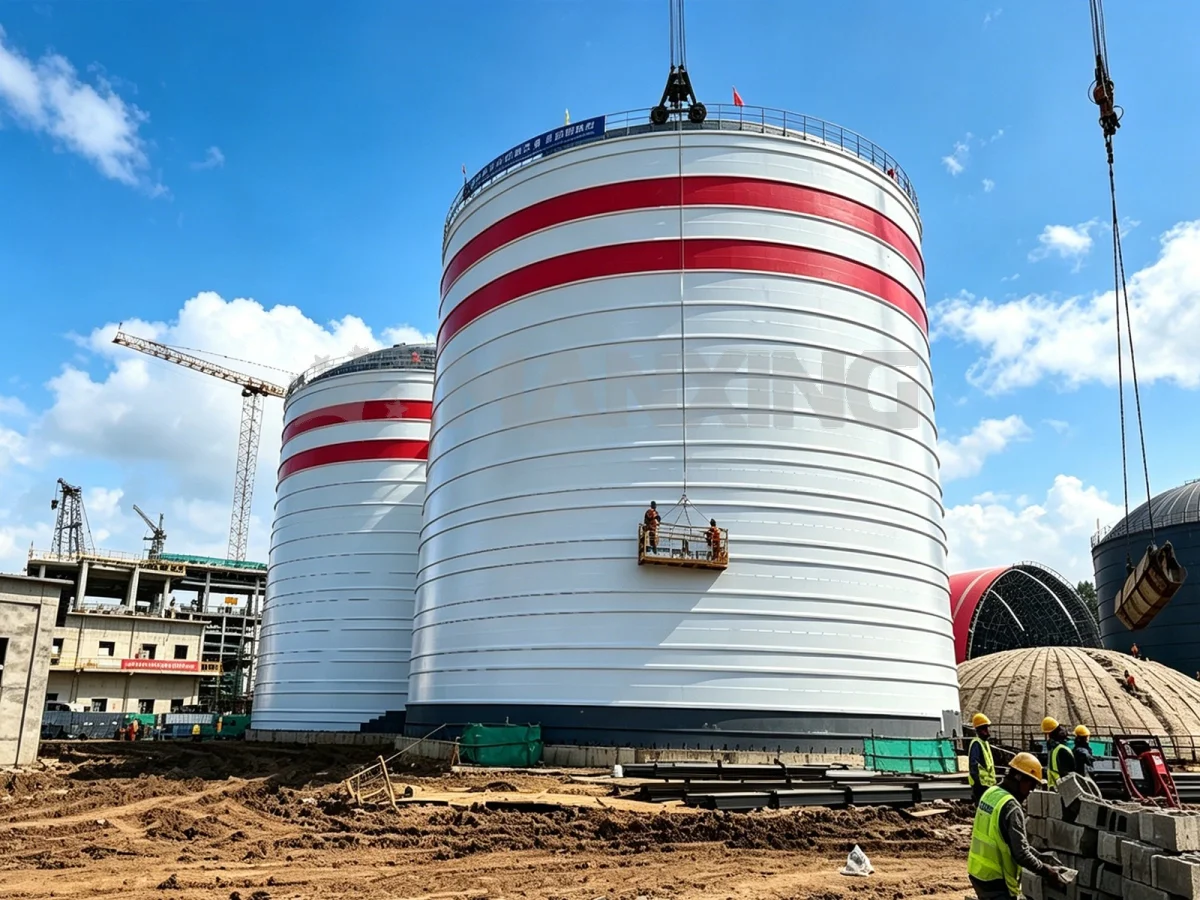
Silos don't fail overnight. They fail slowly, then all at once. The degradation curve is deceptive — years of nothing, then a crack propagates through a critical weld at 3am on a Tuesday. Understanding the mechanisms is the first step to catching them before they catch you.
Material Fatigue and Cyclic Loading
Every fill-empty cycle stresses the shell. A cement silo running two cycles per day racks up 730 load cycles per year. After 15 years, that's 10,950 cycles — enough to initiate fatigue cracks at welded joints, especially around hopper connections and manway openings. The Eurocode 3 fatigue curves for welded details show that a Category 71 weld detail (typical of silo shell-to-hopper connections) has a fatigue life of roughly 2×10⁶ cycles at a stress range of 71 MPa. But real-world stress concentrations at geometric discontinuities can cut that by 40-60%. I've measured shell strains of 380 microstrains at a hopper seam during filling — that's a stress range of about 80 MPa in steel, which puts you in the 10⁵ cycle range for a Category 71 detail. Do the math on a 20-year service life.
Corrosion and Wall Thinning
Internal corrosion in cement and fly ash silos is brutal. The combination of moisture, CO₂, and chlorides creates an environment that eats through 6 mm shell plate at 0.3-0.8 mm per year in humid climates. I pulled an ultrasonic thickness reading on a 12-year-old fly ash silo in Guangdong — original plate was 8 mm, thinnest point was 3.2 mm. That's a 60% loss of cross-section. The silo was still standing because the material had bridged and was carrying some load, but the safety margin against wind buckling had evaporated. External corrosion under insulation is worse because you can't see it. A coal silo in Shanxi had 40% of its external surface corroded beneath cladding that looked pristine from the outside.
Foundation Settlement and Ground Movement
Differential settlement is the silent killer. A 20-meter-diameter silo carrying 5,000 tonnes of clinker imposes a bearing pressure of roughly 150-200 kPa on the foundation. If the subgrade isn't uniform — and it rarely is — the shell tilts. I've seen settlements of 80-120 mm on one side with 10 mm on the opposite side. That tilts the shell, creates eccentric loading, and introduces bending stresses the design never accounted for. The shell starts ovaling, welds crack at the base, and the whole structure enters a feedback loop of increasing distortion. EN 1997-1 requires that differential settlement be limited to 1/500 of the foundation width for sensitive structures. For a 20 m silo, that's 40 mm. Exceed that, and you're in trouble.
Assessment Methods That Actually Work
Not all inspections are created equal. A walk-around with a clipboard and a flashlight catches maybe 15% of what's actually wrong. Real assessment requires a layered approach — visual, dimensional, non-destructive, and instrumental. Skip a layer, and you're gambling.
Visual and Dimensional Inspection
Start with the obvious. Walk the shell. Look for rust streaks, which indicate active corrosion behind paint. Check welds for cracking — use a 10x magnifier, not your eyes. Measure shell verticality with a total station; anything over H/500 (where H is shell height) warrants investigation. For a 30 m tall silo, that's 60 mm of plumb deviation. I once found a silo that was 140 mm off-plumb — the foundation had settled 90 mm on the north side. The shell was buckling in the lower third, visible only as a subtle waviness in the paint. You'd miss it if you weren't looking. Document everything with photographs and a dimensional survey. This is your baseline.
Non-Destructive Testing (NDT)
Ultrasonic thickness testing is non-negotiable. Grid the shell at 300 mm spacing in the lower third and hopper, 500 mm above. Record every reading. I've seen shells that looked fine visually but had localized thinning to 40% of original thickness behind aeration pads where material flow had worn the plate. Magnetic particle inspection (MPI) on welds finds surface-breaking cracks that visual inspection misses. For critical welds — shell-to-hopper, ring stiffener connections, anchor bolt chairs — I recommend 100% MPI. It costs about $15-25 per meter of weld. A full silo might have 200-400 meters of critical welds. That's $3,000-10,000 for testing that could prevent a $2 million failure. The math works.
Structural Monitoring and Instrumentation
For silos in questionable condition, install strain gauges and inclinometers. Bond strain gauges to the shell at the highest-stress locations — typically the hopper-to-shell junction and the lower shell course. Monitor during filling and emptying. I've recorded shell strains of 450 microstrains at a hopper seam during a rapid fill event — that's 94 MPa in steel, which is 34% of yield for S355. The silo was operating at a safety factor of just 3 against yield under normal filling. Add a wind load, and you're at 1.8. That's too close for comfort. Tiltmeters on the foundation detect settlement in real-time. Set an alarm at 20 mm differential — that gives you weeks to react before structural damage occurs.
Critical Failure Modes to Watch For
Silos fail in predictable ways. The failure modes are well-documented in the literature — EN 1993-4-1 covers shell structures, and the Eurocode classification of buckling modes is the standard reference. But knowing the theory and recognizing the signs in the field are different skills.
Buckling and Shell Instability
Thin shells buckle under compression. The critical buckling stress for a cylindrical shell under uniform axial compression is given by σ_cr = 0.605 × E × t/R, where E is Young's modulus, t is thickness, and R is radius. For a 20 m diameter silo with 8 mm shell, that's about 60 MPa. But imperfections — dents, out-of-roundness, weld misalignment — reduce this by 50-70%. The Eurocode knock-down factor for fabrication quality Class C (typical for field-welded silos) is α = 0.21. That brings the design buckling stress down to about 12.6 MPa. A full silo with 5,000 tonnes of cement generates an axial stress in the shell of roughly 8-15 MPa depending on wall friction. You're operating at 63-119% of the buckling capacity. That's why buckling is the number one failure mode for slender silos. Look for elephant-foot buckling at the base — circumferential wrinkles in the shell plate. Each wrinkle is a plastic hinge. Three or four of them, and the shell loses its load-carrying capacity.
Weld and Connection Failures
Welded joints are the weak link. Fillet welds on stiffener connections, lap joints in the shell, and the critical shell-to-hopper weld all fail in fatigue. The failure starts as a toe crack, propagates through the weld throat, and eventually leads to separation. I've seen a hopper drop 300 mm because the shell-to-hopper weld cracked through 80% of its circumference. The hopper was carrying 800 tonnes of clinker. The remaining weld was holding on by a thread — literally, a 3 mm throat of weld metal. We emptied the silo in 14 hours, working around the clock. The repair cost $180,000. A proper NDT program would have caught the crack when it was 10 mm long, not 4 meters.
Hopper and Transition Zone Problems
The transition zone — where the cylindrical shell meets the conical hopper — is the highest-stress region in the entire silo. The radial thrust from the hopper creates a circumferential compression ring in the shell. If the shell isn't stiffened, it buckles inward. I've measured hoop compressive stresses of 120 MPa in the transition zone of a 15 m diameter slag silo. The shell was 10 mm thick, and the calculated buckling capacity was 95 MPa. The silo was operating 26% above buckling capacity. It hadn't failed yet because the material inside was providing some internal pressure, but a rapid emptying event — which reduces internal pressure — would have triggered collapse. We installed a ring stiffener: 150×15 mm flat bar, welded continuously around the circumference. Cost: $12,000. It added 40% to the buckling capacity.
When to Assess and How Often
There's no universal answer, but there are defensible intervals based on service conditions, material aggressiveness, and structural sensitivity. The default position should be: assess more often than you think necessary.
Baseline and Periodic Inspection Schedules
New silos: baseline assessment at commissioning, then annually for the first three years. This catches early-life issues — foundation settlement, weld defects, coating failures. After three years, if the silo is in good condition and operating within design parameters, extend to every two years. For aggressive service — coal, slag, wet fly ash — stay on annual intervals. For benign service — dry cement, alumina in arid climates — you can stretch to three years, but not beyond. I've seen a 25-year-old cement silo in Morocco that had never been internally inspected. The shell had thinned from 10 mm to 4 mm in the lower courses. It was a collapse waiting to happen. The plant manager's response: "It's been fine for 25 years." That's not a structural assessment. That's hope.
Trigger-Based Assessments
Certain events demand immediate assessment, regardless of schedule. Earthquake — even a moderate one (magnitude 5.0+) within 50 km. Foundation flooding or prolonged heavy rain that could soften the subgrade. Overfilling beyond 110% of rated capacity. Any visible deformation, cracking, or unusual noise during operation. I got a call from a plant in Vietnam after a typhoon — 150 mm/hr rainfall for 6 hours. The silo foundation was on fill material that had been poorly compacted. Settlement of 60 mm occurred on the east side. We assessed within 48 hours, found shell cracking at three hopper welds, and executed an emergency repair. The plant was down for 9 days. Without the rapid assessment, they might have filled the silo and lost it entirely.
Case Study: 6,000-Tonne Clinker Silo — Shandong Province
A 30 m diameter, 28 m tall clinker silo showed signs of distress after 12 years of service. The plant reported "rumbling" sounds during filling and visible paint cracking at the hopper-to-shell junction. We conducted a full assessment: dimensional survey, ultrasonic thickness testing, MPI on all hopper welds, and strain gauging during a controlled fill.
Findings: differential settlement of 75 mm (north-south), shell thinning from 10 mm to 5.8 mm in the lower courses, three fatigue cracks in the hopper weld (longest: 1.2 m), and hoop compressive strains of 320 microstrains at the transition zone — equivalent to 67 MPa, 78% of the buckling capacity for the as-built condition. The silo was operating beyond its safe limits.
Repair scope: foundation grouting to stabilize settlement ($45,000), shell plate replacement in the lower two courses ($120,000), hopper weld repair and reinforcement ($85,000), and installation of an external ring stiffener at the transition zone ($28,000). Total repair cost: $278,000. Plant downtime: 21 days. Estimated cost of a collapse: $3.5 million in equipment, 6 months of lost production, and potential fatalities. The repair was completed in 2019. The silo has been operating without issue since, with annual monitoring confirming stable conditions.
FAQ
Q: How much does a full structural integrity assessment cost?
A: For a typical 20-30 m diameter silo, expect $8,000-25,000 depending on scope. Visual and dimensional survey runs $3,000-6,000. Add NDT (ultrasonic thickness + MPI) and you're at $8,000-15,000. Full assessment with strain monitoring and analysis pushes it to $15,000-25,000. That's 0.5-2% of the silo's replacement cost. It's the cheapest insurance you'll ever buy.
Q: Can a silo be assessed while in service?
A: Partially. Visual inspection, external dimensional survey, and some NDT can be done while the silo is full. But internal inspection, shell thickness testing in the lower courses, and weld inspection at the hopper require the silo to be empty and cleaned out. For critical assessments, plan for a 5-10 day outage. I've done external assessments in 2 days that identified enough issues to justify a full internal inspection. That's a good triage approach.
Q: What standards apply to silo structural assessment?
A: EN 1993-4-1 (shell structures) for structural design verification. EN 1991-4 (actions on silos and tanks) for load calculations. EN 1997-1 (geotechnical design) for foundation assessment. For assessment of existing structures, EN 13480 (metallic industrial piping) provides useful guidance on fitness-for-service, though it's not silo-specific. In China, GB 50077 (code for design of reinforced concrete silos) and GB 50128 (code for construction of vertical cylindrical welded steel oil tanks) are commonly referenced. For fitness-of-service assessment of damaged structures, API 579-1/ASME FFS-1 is the international standard, though it's pressure vessel-oriented. The gap in silo-specific assessment standards is real — most assessments rely on engineering judgment backed by first-principles structural analysis.
Need a Silo Structural Integrity Assessment?
Manxing has assessed over 200 silos across 30+ countries — cement, clinker, coal, slag, fly ash, and more. Our engineers have stood on shells in 45°C heat, crawled through hoppers, and caught failures that others missed. We don't just hand you a report. We tell you what's wrong, what it'll cost to fix, and how long you've got before it becomes critical.
Contact Manxing for a site-specific assessment proposal: www.manxingstorage.com