


FRP and Composite Materials in Silo Construction: What Actually Works in the Field
FRP and composite materials aren't replacing steel or concrete silos — they're solving specific problems those materials can't handle. If you're storing corrosive chemicals, abrasive fly ash, or hygroscopic powders that bridge and rat-hole, composites give you flow reliability and corrosion resistance that painted steel won't survive past year five. Here's where they earn their keep, and where they'll cost you.
Where FRP and Composites Fit in Silo Design
Not a Full Replacement — A Targeted Solution
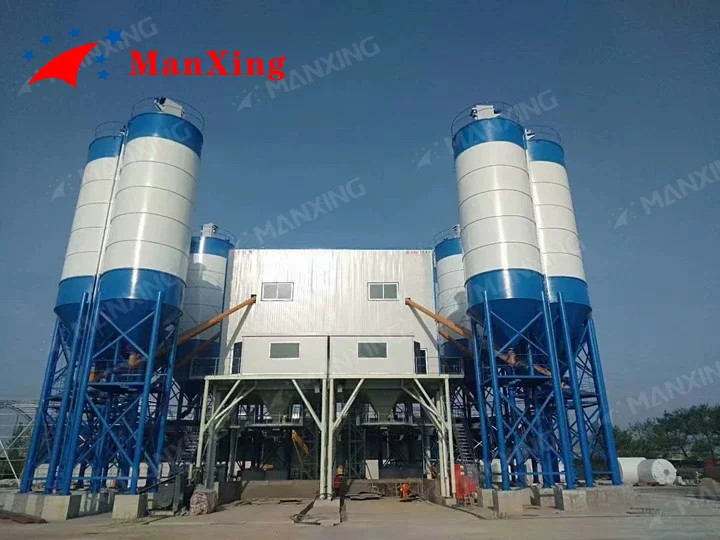
I've had clients ask me to build an entire 5,000-tonne cement silo out of fiberglass. I won't do it, and here's why: the structural demands of a large bulk storage silo — wind loading per EN 1991-1-4, seismic forces, material pressure per EN 1991-4, thermal expansion — these are steel and concrete problems. FRP doesn't have the modulus of elasticity to handle those loads at scale without becoming prohibitively thick and expensive.
But put that same FRP inside a steel shell as a liner, or use it for a chute, a roof panel, a conical hopper section, or a small-capacity day bin under 200 tonnes, and suddenly it's the smartest material on the site. The trick is knowing the boundary. I've seen projects where the engineer specified FRP for everything because the brochure looked good. Eighteen months later, the shell was buckling under thermal load. That's not a material failure — it's a design failure.
The Materials You'll Actually Encounter
When we say "FRP" in silo work, we're usually talking about glass-fiber-reinforced polyester (GRP) or glass-fiber-reinforced vinyl ester (GRE). The difference matters more than most people think. Polyester handles most cement and fly ash applications fine. But if you're storing ammonium chloride, sodium hypochlorite, or anything with a pH below 2 or above 12 at elevated temperatures, vinyl ester is the only choice. I've seen polyester liners dissolve in 14 months in a chemical plant in Jiangsu. The vinyl ester replacement is still running after six years.
Carbon fiber composites show up in high-stiffness applications — think large-diameter ducting or structural reinforcement — but the cost is 8 to 12 times that of glass fiber. For most silo applications, E-glass or S-glass in a polyester or vinyl ester matrix is the practical range. Basalt fiber is gaining traction in some European projects for its temperature resistance (stable to about 650°C versus 350°C for glass), but supply chains are still thin outside China and Russia.
The Real Advantages (and Where They Matter)
Corrosion Resistance That Steel Can't Match
This is the headline, and it's legitimate. A steel silo storing fly ash in a coastal environment — I'm thinking of a project in Vietnam, 400 meters from the South China Sea — will need its interior recoated every 3 to 4 years if it's carbon steel with an epoxy lining. The chloride-laden humidity gets through pinholes you can't see. We switched the hopper section to GRE for a follow-up project at the same plant. After seven years, the liner looks almost new. The steel shell above it needed its second repaint at year five.
The numbers back it up. FRP doesn't corrode in the electrochemical sense — there's no galvanic cell. Chemical resistance depends on the resin matrix, but properly specified GRE handles a pH range of 1 to 14 at temperatures up to 120°C. That covers almost every industrial powder and granular material I've encountered. The exception is concentrated hydrofluoric acid and some strong oxidizing agents, which attack the glass fibers themselves.
Weight Savings That Change the Foundation Math
FRP weighs 1,800 to 2,000 kg/m³. Steel is 7,850 kg/m³. Concrete is 2,400 kg/m³. That density difference doesn't just mean lighter panels — it means smaller foundations, lighter support structures, and in retrofit scenarios, it means you can add internal liners or chutes without exceeding the original structural load capacity.
I remember a project in Malaysia where the client wanted to add a 150-tonne fly ash day bin inside an existing steel structure. The original structure was already at 85% of its rated capacity. A steel bin would have pushed it over. We built the bin in FRP — shell, hopper, and roof — and came in at 4.2 tonnes total. The steel equivalent would have been around 11 tonnes. The structural engineer signed off without a single reinforcement. That's the kind of weight saving that changes a project from "maybe" to "yes."
Flow Promotion and Abrasion Resistance
FRP surfaces are smoother than steel — typically a surface roughness (Ra) of 0.5 to 2.0 micrometers versus 3 to 12 for painted steel. For cohesive materials like moist fly ash, gypsum, or fine chemical powders, that reduced wall friction can mean the difference between mass flow and funnel flow. Mass flow gives you first-in-first-out discharge, no stagnant zones, and predictable discharge rates. Funnel flow gives you rat-holing, bridging, and the 3am phone call about a blocked outlet.
Abrasion resistance is more nuanced. FRP handles fine particle abrasion well — the resin surface erodes slowly, and the glass fibers underneath maintain structural integrity. But if you're handling large, sharp particles like limestone or coal at high impact angles, the resin can erode preferentially, exposing fibers and creating a rough surface that accelerates wear. In those cases, I'll specify a ceramic-filled resin or a urethane-lined steel chute instead. FRP isn't magic — it's a tool for specific jobs.
The Limitations Nobody Puts in the Brochure
Fire Performance — The Elephant in the Room
FRP burns. Polyester resin ignites at around 300 to 350°C. Vinyl ester is similar. Once ignited, it produces dense black smoke and toxic gases including carbon monoxide and styrene. For coal storage applications, this is a non-negotiable design constraint. ISO 15012 and EN 14491 both address dust explosion and fire prevention in bulk storage, and FRP components need to be evaluated against those standards just like any other material.
In coal silos, I won't specify FRP for any component that could be exposed to a fire source — no FRP liners near conveyor transfer points, no FRP roof panels where spontaneous heating could initiate. Where I do use FRP in coal applications, it's for external chutes and dust collection ducting, always with fire-retardant resin (halogenated or alumina-trihydrate filled) and always with the client's explicit sign-off on the fire risk assessment. Some engineers won't touch FRP in coal plants at all. I understand that position, even if I don't always share it.
UV Degradation and Long-Term Aging
Unprotected FRP loses 20 to 30% of its mechanical properties after 10 to 15 years of direct UV exposure. The resin surface chalks, fibers become exposed, and the laminate weakens from the outside in. For exterior silo components — roof panels, external chutes, handrails — you need either a UV-stabilized gel coat, a painted finish, or a sacrificial surface veil. I've seen FRP roof panels on a silo in Rajasthan, India, where the surface was so degraded after 12 years that you could push a screwdriver through the top 0.5 mm of laminate. The structural layers underneath were fine, but water had been wicking in through the degraded surface for years.
The fix is simple and cheap: a 0.3 to 0.5 mm UV-resistant gel coat applied during manufacturing, or a polyurethane paint system applied on site. Either one adds maybe 8 to 12% to the component cost and buys you 20-plus years of service. Skipping it to save money is false economy.
Cost Reality Check
FRP components cost 2 to 4 times more than equivalent carbon steel components by weight. A GRE hopper liner for a 2,000-tonne silo might run $15,000 to $25,000 in material alone, versus $5,000 to $8,000 for a painted steel liner. But the steel liner will need recoating or replacement every 5 to 7 years in a corrosive environment. Over a 25-year silo life, the FRP liner is cheaper on a net-present-value basis. I've run the numbers for clients in Indonesia, Brazil, and Turkey — the crossover point is usually between year 8 and year 12.
The problem is that capital budgets and maintenance budgets live in different spreadsheets. The project team that builds the silo doesn't pay for the repainting. So FRP loses the first-cost comparison even when it wins the lifecycle comparison. If you're the plant owner, push back on that. Ask for the 20-year cost, not the day-one cost.
Design Standards and Engineering Considerations
What the Codes Actually Say
FRP silo design doesn't have a single dedicated code the way steel has EN 1993-4-1 or concrete has EN 1992-4. Instead, you're pulling from a patchwork: BS EN 13121 for static tanks, ASME RTP-1 for reinforced thermoset plastics, and various manufacturer-specific design manuals that reference ISO 14692 for piping components. For structural FRP shapes, ASTM D3039 covers tensile properties, and ASTM D638 covers flexural properties. The design approach is typically allowable stress rather than limit state, which means higher safety factors — typically 3.0 to 4.0 on ultimate tensile strength for structural applications.
That higher safety factor is partly why FRP silos feel overdesigned compared to steel. A steel silo might use a safety factor of 1.5 to 2.0 on yield strength. FRP uses 3.0 to 4.0 on ultimate. The reason is variability — FRP properties depend on fiber orientation, resin content, cure quality, and manufacturing method in ways that rolled steel doesn't. A good fabricator with consistent quality control can justify lower safety factors, but most designers stick with the conservative values because the consequences of getting it wrong are severe.
Connection Details — Where Projects Go Wrong
FRP doesn't weld. It bolts, bonds, or flanges. And every connection is a potential failure point. Bolt holes in FRP create stress concentrations that are 2 to 3 times higher than in steel because the material can't yield locally to redistribute stress. Edge distances need to be at least 3 times the bolt diameter — 5 times is better. I've seen a flange connection on a FRP duct in a cement plant fail after 6 months because the designer used steel spacing rules. The FRP cracked along the bolt line from thermal cycling.
Adhesive bonding works well for FRP-to-FRP joints if the surfaces are properly prepared — grit blasted or sanded to remove the gel coat and expose fresh laminate. But bonded joints are sensitive to surface preparation, humidity during cure, and temperature. On site, those conditions are hard to control. I prefer mechanical connections for field joints and reserve adhesive bonding for factory-assembled modules. It's less elegant, but it's reliable.
Case Study: GRE Liner Retrofit in a Fly Ash Silo — Shandong Province, China
A 3,000-tonne fly ash silo at a coal-fired power plant was experiencing severe internal corrosion. The original carbon steel interior with an epoxy coating had failed after 4 years — the coating was blistering and peeling in sheets, and the bare steel underneath was pitting to depths of 1.5 mm. The plant was losing product to contamination and facing a full internal recoat that would take the silo offline for 3 weeks.
We designed a GRE liner system — 3 mm thick panels, mechanically fastened to the existing shell with stainless steel bolts at 300 mm centers, with a 5 mm drainage gap behind each panel. The conical hopper section used 4 mm GRE with a 45-degree wall angle to promote mass flow. Total liner weight was 1.8 tonnes. Installation took 12 days with a crew of 6, and the silo was back in service within 2 weeks of mobilization.
Cost: ¥380,000 for materials and installation. The alternative — full internal recoat with surface preparation — was quoted at ¥220,000 but would have needed repeating every 4 to 5 years. At the 20-year mark, the GRE liner had paid for itself twice over. After 9 years of service, the liner shows no measurable degradation. The plant's maintenance team checks it annually during scheduled outages. They've never found anything to fix.
Frequently Asked Questions
Can you build an entire large-capacity silo out of FRP?
For silos above about 200 tonnes, a fully FRP shell is rarely practical. The structural demands — wind, seismic, material pressure — require laminate thicknesses that become cost-prohibitive and heavy enough to negate the weight advantage. FRP works best as a liner, hopper, chute, or small-capacity bin. For large silos, steel or concrete for the shell with FRP for the wetted or high-wear surfaces is the standard approach.
How does FRP handle thermal expansion compared to steel?
FRP has a coefficient of thermal expansion of 18 to 24 × 10⁻⁶/°C, roughly 1.5 to 2 times that of steel (12 × 10⁻⁶/°C). In a silo exposed to direct sun, a 40°C temperature swing means the FRP component will expand about 30% more than the steel shell around it. This has to be accommodated in the connection design — slotted bolt holes, flexible gaskets, or expansion joints. Ignore it, and you'll get buckled panels or cracked connections within the first year.
What's the expected service life of FRP in a cement or fly ash silo?
With proper resin selection and UV protection where needed, FRP components in cement and fly ash service routinely achieve 20 to 30 years. I've seen GRE liners in fly ash silos still performing after 15 years with no maintenance beyond annual inspection. The key variables are resin type (vinyl ester for aggressive chemistry), thickness (3 to 5 mm for liners, 5 to 8 mm for structural components), and connection design. Get those three right, and the material takes care of itself.
Need FRP or Composite Solutions for Your Silo Project?
Manxing has designed and installed FRP liners, chutes, hoppers, and small-capacity composite silos across cement, fly ash, chemical, and mineral processing plants in 30+ countries. We'll tell you where composites make sense — and where they don't. No brochure promises, just engineering judgment from a team that's been on the tools.