


Material Selection Guide for Different Bulk Materials: What Actually Works in Industrial Silos
Choosing the wrong steel for a bulk solids silo isn't a paperwork error — it's a structural failure waiting to happen. The right material selection depends on three things: the material's abrasiveness, its moisture content and chemical profile, and the temperature range it'll see in service. Get those three right, and your silo lasts 25+ years. Get them wrong, and you're looking at wall thinning, stress cracking, or a full replacement inside a decade.
Why Material Selection Is the Decision You Can't Undo
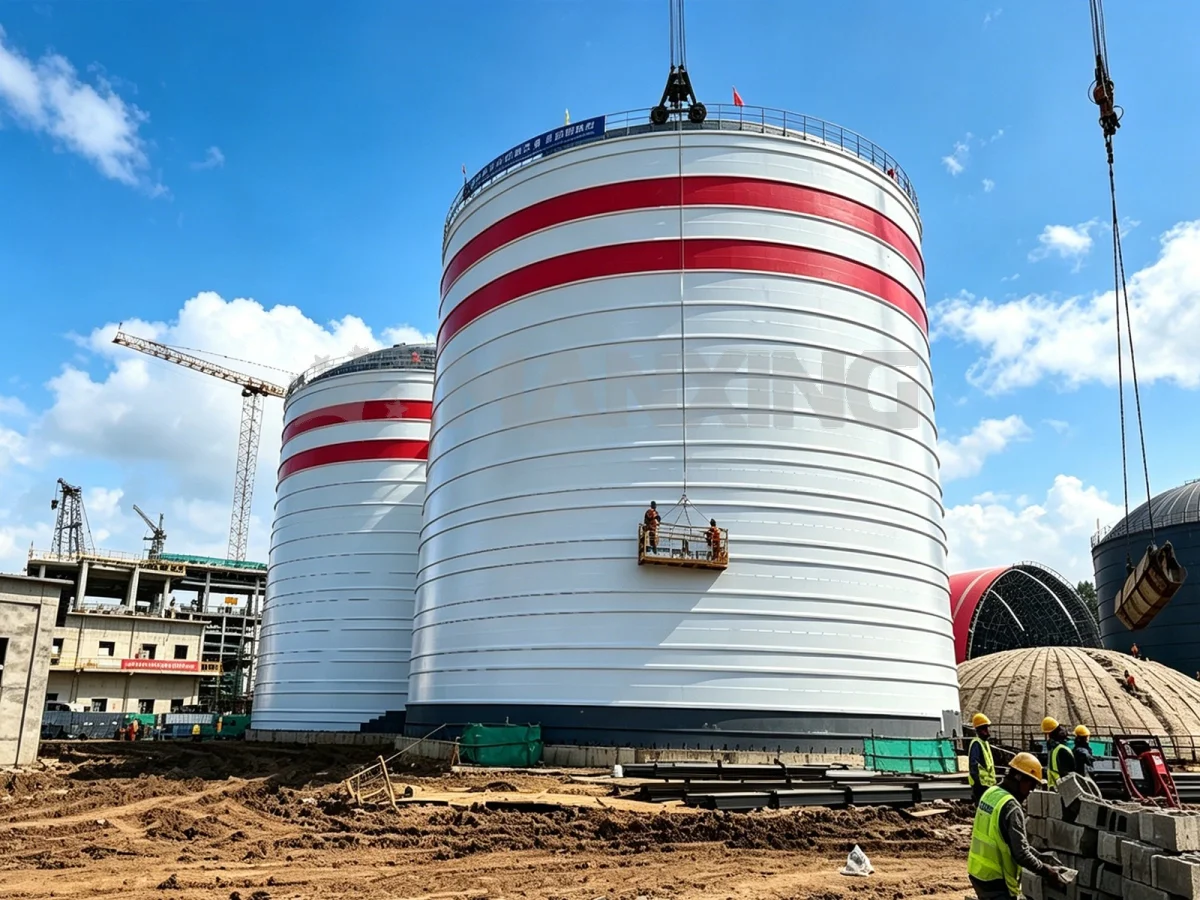
Here's the thing. Once a silo is erected, you can't swap the shell plate. You can add liners, you can patch, you can pray — but the base material is locked in. I've seen plants spend $180,000 on a clinker silo only to discover eighteen months later that the carbon steel walls were losing 1.2 mm per year to abrasion. The fix? A $340,000 internal liner retrofit with six weeks of downtime. Nobody budgets for that.
Material selection isn't just about corrosion charts in a textbook. It's about the specific bulk material, the specific climate, and the specific operating pattern of your plant. A cement silo in coastal Vietnam faces a completely different challenge than the same silo in inland Kazakhstan. Same product. Different world.
The Three Factors That Actually Drive Selection
Every bulk material has a personality. Some are abrasive. Some are corrosive. Some are both. And some sit quietly for months, generating condensation in the headspace that eats the roof from the inside out.
Abrasion resistance matters most for hard, angular particles — clinker, slag, alumina, silica sand. These materials don't just sit there. They slide, they roll, they impact the wall at angles that gouge steel. A 10,000-tonne clinker silo with a 6 m diameter sees roughly 15 tonnes of material sliding down the wall during every extraction cycle. Multiply that by 300 cycles a year, and you're looking at 4,500 tonnes of abrasive contact annually. On bare carbon steel, that's measurable wall loss within two years.
Corrosion resistance is driven by moisture and chemistry. Fly ash with a pH of 11–13 is aggressively alkaline. Coal with 8–12% sulfur content generates sulfuric acid when moisture condenses. Limestone might seem benign, but in a humid environment with CO₂ in the headspace, you get carbonic acid formation that attacks zinc coatings and bare steel alike.
Temperature changes everything. At 80–120°C — typical for hot cement or clinker — oxidation rates accelerate. At sub-zero temperatures, carbon steel transitions from ductile to brittle. The ductile-to-brittle transition for mild carbon steel starts around -20°C. In northern China, Mongolia, or Kazakhstan, winter temperatures hit -35°C. That's not a theoretical concern. That's a shell fracture risk.
What the Standards Actually Say
Eurocode 3 (EN 1993-4-1) governs silo structural design, but it doesn't tell you which steel grade to pick. That's on you. The standard gives you load cases, buckling curves, and weld detail categories. The material choice comes from your process knowledge.
For reference, EN 10025 covers structural steel grades — S235, S275, S355, and up. ASTM A36 and ASTM A572 are the common North American equivalents. For corrosion resistance, you're looking at ASTM A588 (weathering steel) or stainless grades like 304L and 316L under ASTM A240. Abrasion-resistant plate falls under AR400, AR450, AR500 — the number being the Brinell hardness.
The standards give you the framework. Your material selection fills in the blanks.
Carbon Steel: The Default Choice and Its Limits
Carbon steel — S275 or S355 in Europe, A36 or A572 in North America — is what most silos are built from. It's cheap, it's available everywhere, it welds beautifully, and every fabrication shop on the planet knows how to work with it. For dry, non-corrosive, non-abrasive materials like Portland cement at ambient temperature, it's perfectly fine.
But "perfectly fine" has a narrower range than most people think.
When Carbon Steel Works
Portland cement (dry,
The key word is "dry." The moment moisture enters the equation, carbon steel's corrosion rate jumps. At 60% relative humidity inside the silo, bare carbon steel corrodes at roughly 0.05–0.1 mm/year. At 85% humidity with condensation, that number doubles or triples. A 6 mm wall plate can lose 30% of its thickness in 15 years if the environment is wet enough.
When Carbon Steel Fails
Hot clinker at 150–250°C. Coal with high sulfur content. Salt-contaminated limestone. Seawater-cooled plant environments. These are the applications where carbon steel is a gamble — and not a good one.
I remember a project in Malaysia where a client insisted on carbon steel for a 5,000-tonne coal silo. The coal had 9% sulfur and 11% moisture. Within fourteen months, the lower cone showed pitting corrosion up to 3 mm deep. The plant manager called me, not to ask what went wrong, but to ask how fast we could line it. We ended up installing a 316L stainless steel liner in the lower 4 meters of the cone. Cost more than if we'd just built the cone in stainless from the start.
Stainless Steel: Where It Pays for Itself
Stainless steel in silo construction isn't about being fancy. It's about eliminating corrosion as a failure mode. The upfront cost is 3–5 times carbon steel, but the lifecycle cost tells a different story.
304L vs. 316L — The Practical Difference
For most bulk solids applications, 304L (1.4301) is sufficient. It handles alkaline environments, moderate acid exposure, and food-grade requirements. Cement, fly ash, most minerals — 304L handles them without breaking a sweat.
316L (1.4404) adds molybdenum — 2–3% — which dramatically improves resistance to chloride-induced pitting. If your plant is within 10 km of the coast, or if your bulk material contains chlorides (some fly ashes do, some slags do), 316L is the right call. The cost premium over 304L is roughly 25–30%, but the pitting resistance is in a different league entirely.
Here's a number that matters: in a salt-laden coastal environment, 304L can show pitting within 3–5 years. 316L will typically last 15–20 years without significant pitting. That's the difference between a maintenance headache and a set-it-and-forget-it installation.
Where to Use Stainless — and Where to Save
You don't always need the entire silo in stainless. A common approach — and one we use regularly at Manxing — is a hybrid design. Carbon steel shell and roof, stainless steel lower cone and discharge zone. The lower 3–5 meters of a silo sees the most abrasion, the most moisture accumulation, and the most impact. That's where stainless earns its keep.
For a 3,000-tonne cement silo, a hybrid design might add $45,000–$65,000 to the material cost compared to full carbon steel. But it eliminates the need for a cone liner replacement at year 8–10, which would cost $80,000–$120,000 with downtime. The math isn't close.
Abrasion-Resistant Plate and Wear Liners
Some materials don't corrode steel — they eat it. Clinker, alumina, silica sand, iron ore, and granulated slag are the usual suspects. These materials have Mohs hardness values of 5–7, and they move across steel surfaces at velocities up to 2–3 m/s during discharge. The result is mechanical wear, not chemical corrosion.
AR400 plate (400 BHN) is the workhorse for abrasion-resistant applications. It's through-hardened, weldable with proper procedures, and available in thicknesses from 6 mm to 50 mm. For most clinker and slag silos, an AR400 liner in the lower cone and transition zone extends service life by 8–12 years compared to bare carbon steel.
AR500 (500 BHN) is harder but less ductile. It's better for high-impact zones — the area directly below the fill point, where material drops 4–8 meters and hits the cone wall at full velocity. I've seen AR500 liners in alumina silos last 10+ years with minimal wear. The same zone in bare S355 steel? You're replacing plates every 18–24 months.
Ceramic and Polyurethane Liners
For extreme abrasion, steel liners aren't always the answer. Ceramic tile liners (92% alumina, Mohs hardness 9) can outlast steel by a factor of 5–10 in high-wear zones. The downside is weight — ceramic adds 30–40 kg/m² — and brittleness. A direct impact from a large clinker lump can crack tiles.
Polyurethane liners are the opposite: flexible, impact-resistant, but limited to temperatures below 80°C. They work well for softer abrasive materials like limestone and aggregates at ambient temperature. For hot materials, stick with steel or ceramic.
Specialty Materials for Extreme Conditions
Some applications push beyond the standard playbook. Hot materials, highly corrosive chemicals, and cryogenic storage all demand specific material choices that most silo designers never encounter — but when you do, there's no room for guessing.
Hot Material Silos (Clinker, Hot Ash, Heated Minerals)
Clinker at 200°C changes the game in two ways. First, the steel loses strength. At 200°C, S355 retains about 90% of its yield strength. At 300°C, it's down to 80%. At 400°C, you're at 60% — and you need to account for that in your structural design per EN 1993-1-2.
Second, thermal cycling causes fatigue. A silo that fills with hot material during the day and cools at night sees daily temperature swings of 100–150°C. Over a year, that's 365 thermal cycles. Over 20 years, that's 7,300 cycles. Fatigue cracking at weld toes in the shell-to-cone junction is a real failure mode — and one that's caught more than one plant off guard.
For hot clinker silos, we typically specify ASTM A516 Grade 70 pressure vessel plate for the lower shell and cone. It has better elevated-temperature properties than structural grades, and it's readily available in thicknesses up to 60 mm. Combined with an AR400 liner in the cone, this gives you a silo that handles both the thermal and abrasive loads.
Corrosive Chemical Powders
Sodium carbonate, calcium hypochlorite, certain fertilizer compounds — these materials are chemically aggressive in ways that standard carbon steel can't handle. For these applications, duplex stainless steels (2205, 2507) or even fiber-reinforced polymer (FRP) construction may be warranted.
Duplex 2205 has roughly twice the yield strength of 316L and significantly better stress corrosion cracking resistance. It's more expensive — about 2–3 times the cost of 316L — but for a 2,000-tonne sodium carbonate silo in a coastal plant, it's the only material that makes sense long-term.
Case Study: 8,000-Tonne Clinker Silo — Shandong Province, China
A cement plant in Shandong needed a new clinker silo. The clinker temperature at the silo inlet was 180°C, with peaks to 220°C during kiln upset conditions. The material was highly abrasive — 28-day unconfined compressive strength of the parent limestone was 95 MPa, producing hard, angular clinker particles.
The original design from a local firm called for S355 carbon steel throughout, with a polyurethane cone liner. We reviewed the spec and flagged three problems: polyurethane degrades above 80°C, carbon steel at 200°C loses 10% of its yield strength, and the cone would see severe abrasion from clinker sliding at 1.5–2 m/s during discharge.
Our redesign used ASTM A516 Grade 70 for the lower 6 meters of the shell and the full cone, with an AR500 wear liner (12 mm thick) in the cone's lower 3 meters. The upper shell remained S355 with a standard epoxy coating system. The roof structure was S355 with a 316L stainless steel inner liner in the headspace to handle condensation from temperature cycling.
The result: the silo was commissioned in 2019. As of 2024, the AR500 liner shows less than 1 mm of wear. The shell thickness measurements at the 2023 inspection were within 0.2 mm of original. The plant's maintenance team reports zero corrosion-related issues. Total material cost premium over the original carbon-steel design was approximately $120,000. Estimated avoided maintenance cost over 20 years: $400,000–$500,000.
FAQ
Can I use the same silo material for different bulk materials if I clean it between campaigns?
Technically yes, but it's risky. Cross-contamination is a real problem — residual material in aeration pads, corners, and wall crevices can react with the next material. More importantly, if the previous material was corrosive, it may have already compromised the wall surface in ways you can't see. We recommend dedicated silos for chemically incompatible materials. If you must share, at minimum do a full internal inspection and wall thickness survey before switching.
How do I know if my existing silo needs a material upgrade?
Wall thickness monitoring is the answer. Ultrasonic thickness testing at 1 m grid points, focusing on the lower shell, cone, and discharge zone, gives you a clear picture. If you're losing more than 0.1 mm/year on carbon steel, something's wrong — either the material is more corrosive than expected, or moisture control is failing. If you're losing more than 0.3 mm/year, you need a liner or a material upgrade. Don't wait until you're measuring holes.
Is weathering steel (Corten) a good choice for silos?
For outdoor structural elements like roof frames and stair towers, yes — weathering steel forms a stable oxide layer that protects against atmospheric corrosion. For the silo shell in contact with bulk material, no. The oxide layer doesn't form properly under a blanket of stored material, and the material's moisture can actually accelerate localized corrosion. I've seen Corten silo shells fail in ways that painted carbon steel wouldn't have. Stick with painted carbon steel or stainless for the shell.
Need Help Specifying the Right Material for Your Silo?
At Manxing, we've designed and built silos for cement, clinker, fly ash, coal, slag, alumina, and over 30 other bulk materials across 30+ countries. Every project starts with a material assessment — because the wrong steel grade is the most expensive mistake you can make.
Contact our engineering team at manxingstorage.com for a free material selection review. Send us your bulk material specs, operating temperatures, and site conditions. We'll tell you exactly what works — and what doesn't.