


How to Evaluate Industrial Silo Manufacturers: A Field Engineer's Comparison Framework
You're spending $2–15 million on a storage silo system. The wrong manufacturer won't show their problems until year three — when your roof bolts are shearing and your discharge cones are worn through. This guide walks you through the five things that actually separate a reliable EPC silo contractor from a steel fabricator with a nice brochure. I've sat through enough factory audits and site commissions to know the difference.
1. Engineering Depth: It's Not Just Steel, It's a Pressure Vessel Problem
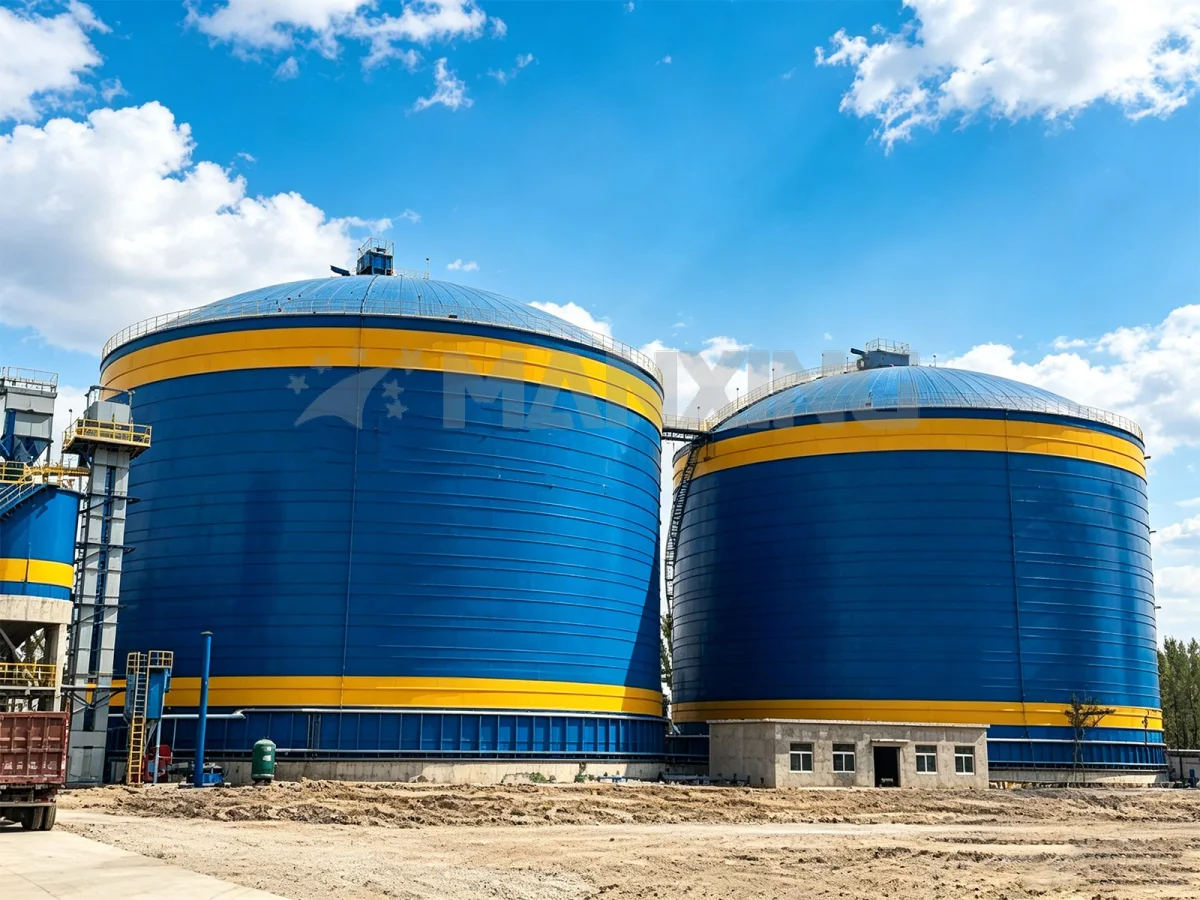
Here's what most buyers miss: a cement silo isn't a tank. It's a structure that handles asymmetric loading, thermal cycling, wind loads, seismic forces, and material that changes bulk density depending on how long it's been sitting. You need an engineering team that understands all of that simultaneously.
1.1 Who Actually Does the Structural Calculations
I've visited factories where the "engineering department" is one guy running a finite-element model he downloaded a license for last month. That's not engineering — that's gambling.
Ask your potential manufacturer: Who signs off on the calculations? What software do they use? Can they show you a full load case analysis per EN 1991-4 (the European standard for silo structures) or the equivalent GB 50009 for Chinese projects?
A serious manufacturer will have in-house structural engineers who've done this hundreds of times. They'll hand you a calculation package with wind load assumptions, seismic zone data, material density inputs, and wall friction coefficients. If they send you a PDF of a catalog page instead, walk away.
1.2 Material Flow Analysis — The Thing Nobody Talks About
Mass flow or funnel flow? That decision affects your entire plant. A funnel flow silo for fly ash will rat-hole and bridge. A mass flow silo for sand might not need that expensive cone geometry.
Good manufacturers run material flow analysis using Jenike's method (ASTM D6128 for wall friction testing). They'll test your actual bulk material — not a generic "cement" assumption — and tell you what cone angle, outlet size, and wall finish you need. I've seen projects where the wrong assumption about wall friction angle (off by just 3 degrees) caused a 4,000-tonne clinker silo to bridge solid within the first month.
Ask for the flow function test data. If they can't produce it, they're guessing.
2. Manufacturing Quality: What the Factory Floor Tells You
Brochures lie. Factory floors don't. I always tell clients: before you sign anything, visit the manufacturing facility. Here's what to look for.
1.2 Plate Preparation and Welding Standards
A 5,000-tonne cement silo might use 12mm to 25mm steel plate depending on the height-to-diameter ratio. The quality of that plate preparation determines whether your silo lasts 25 years or 8.
Check their submerged arc welding (SAW) procedures — that's what you want for vertical seams on the shell. Ask to see their Welding Procedure Specifications (WPS) and Procedure Qualification Records (PQR) per AWS D1.1 or equivalent. I once audited a factory where they were doing manual stick welding on vertical seams for a 30-meter-tall silo. The rejection rate on radiographic testing was 34%. That's not a supplier — that's a liability.
Look at the plate edge preparation. CNC plasma cutting with beveled edges for full-penetration welds? Good. Hand-cut edges with visible warping? Walk away.
2.2 Surface Preparation and Coating Systems
For coal and slag storage, internal corrosion is a real problem. Coal can hold moisture at 8–12% content, and with sulfur compounds present, you're looking at acidic corrosion rates of 0.1–0.3 mm per year on unprotected carbon steel.
A competent manufacturer will blast to Sa 2.5 (ISO 8501-1) and apply a coating system suited to the material. For cement and clinker, a standard epoxy primer at 75–100 µm DFT might be fine. For coal or slag in humid environments, you're looking at glass-flake vinyl ester at 400–600 µm DFT. Ask for the coating specification sheet — not a verbal promise.
3. EPC Capability vs. Supply-Only: The Integration Gap
This is where projects go sideways. A silo doesn't exist in isolation. It connects to your conveyor system, your dust collection, your aeration system, your weighing and your PLC. The question is: who owns the interface?
3.1 Pneumatic Conveying Receiving Points
If your silo receives material via pneumatic conveying (which most modern plants do), the inlet design matters enormously. A 150mm-diameter conveying line running at 0.8–1.2 bar will dump material at velocity into your silo. Without proper inlet baffling and dust settling geometry, you'll overload your filter, blind your bags, and have material streaming out of the vent within weeks.
An EPC contractor who also does the conveying system will coordinate the inlet nozzle size, orientation, and the dust collector capacity as one system. A supply-only silo manufacturer will bolt a flange on top and say "not my problem." Then you spend six months and $80,000–150,000 fixing it after the fact.
3.2 Structural Interfaces: Who Takes the Load
A 10,000-tonne silo full of cement weighs roughly 12,000 tonnes including the steel structure. That load goes into your foundation. But what about the drag forces from the material pushing laterally on the walls? What about the uplift from wind on the roof?
The manufacturer needs to provide accurate load reactions for the foundation designer. I've seen cases where the assumed horizontal thrust was 40% below what EN 1991-4 actually requires for the given material and geometry. The foundation cracked within two years. The silo manufacturer said "we provided the loads you asked for." The foundation designer said "we designed to what we were given." Nobody was technically wrong. The plant still had to spend $200,000 on foundation remediation.
Full EPC contractors carry this responsibility as a single package. That's worth something.
4. Explosion Protection and Safety Systems
If you're storing combustible dust — and cement, fly ash, coal, and most mineral powders are combustible under the right conditions — explosion protection isn't optional. It's regulated.
4.1 What the Standards Actually Require
EN 14491 (dust explosion venting) and NFPA 68 (explosion venting protection) both define the required vent area based on the silo volume, the dust's Kst value, and the reduced explosion pressure (Pred) of the silo body.
For cement dust, Kst values typically run 100–150 bar·m/s (St1 class). For coal dust, you might see 150–200 bar·m/s (St1 to St2). A 3,000 m³ silo storing coal dust might need 2.5–4.0 m² of vent area depending on the Pred rating of the shell.
Here's the problem: some manufacturers undersize the vent area to keep costs down. They'll install a 1.0 m² vent on a silo that needs 3.0 m². When the inspector shows up (and they will), you're shut down until it's fixed. Ask for the explosion vent sizing calculation. It should reference EN 14491 or NFPA 68 with actual Kst data for your material.
4.2 Suppression vs. Venting — When You Need More
If your silo is indoors, or near other equipment, or in a location where a vented flame would endanger personnel, you might need explosion suppression instead of (or in addition to) venting. Suppression systems use pressure detectors that respond within 1–3 milliseconds and inject suppressant at 2–6 bar through nozzles mounted in the silo roof.
These systems cost $50,000–150,000 per silo depending on size. Some manufacturers treat them as an afterthought. A good EPC contractor will specify the right protection strategy during the design phase — not as a change order after the steel is already fabricated.
5. After-Sales Support and Spare Parts Availability
The silo will be on your site for 20–30 years. The manufacturer might not be. Or they might be, but their business model might not support long-term service. This matters more than most buyers realize.
5.1 What Breaks First
In my experience, the first failures in a well-built silo system are almost always in the ancillary equipment, not the shell:
- Aeration pads and fluidizing membranes: These degrade from cyclic loading and material abrasion. Expect replacement every 3–7 years depending on material hardness.
- Dust collector filter media: Standard polyester bags last 18–36 months in a cement application. PTFE membrane bags can go 48–60 months but cost 3–4× more.
- Level indicators: Rotating paddle switches fail. Radar units drift. Plan for calibration and replacement every 2–4 years.
- Slide valves and butterfly valves: The sealing surfaces wear from abrasive material flow. In a slag application, you might need a full valve rebuild every 18 months.
Ask your manufacturer: Do you stock spare parts? What's your lead time for a replacement aeration pad set? Can you send a service technician to site within 72 hours? If the answer to any of those is vague, you're going to have a very expensive stockout situation someday.
5.2 Documentation Handover
A proper handover package should include: as-built drawings, welding inspection reports, material certificates (EN 10204 Type 3.1), coating thickness records, explosion protection device certifications, and a maintenance schedule with torque specs for every bolted connection.
I've commissioned silos where the handover package was a USB drive with a single PDF of the general arrangement drawing. That's not documentation — that's a receipt.
Case Study: 6,000-Tonne Fly Ash Silo — Central Vietnam
A power plant needed a 6,000-tonne fly ash silo with a design discharge rate of 200 tonnes per hour. The initial bid from a supply-only fabricator came in 22% below the EPC contractor's price. The plant went with the cheaper option.
Eight months after commissioning, three problems emerged simultaneously: the fly ash was bridging in the outlet cone (the wall friction angle had been assumed at 22° — actual tested value was 28°), the dust collector was undersized by 40% because the conveying air volume hadn't been coordinated with the silo inlet, and the aeration system was running continuously because the material couldn't fluidize properly through the restricted outlet.
The total cost of remediation — new cone insert, upgraded dust collector, redesigned aeration grid, and two weeks of lost production — came to approximately $340,000. The initial "savings" were $180,000. The plant manager told me later: "We saved money on the purchase and spent double on the fix."
The lesson isn't that supply-only manufacturers are always wrong. It's that the lowest bid rarely accounts for system integration costs. Those costs don't disappear — they just show up later, on your dime.
Frequently Asked Questions
Q: How long does it typically take to fabricate and erect a large industrial silo?
A: For a 3,000–5,000-tonne cement silo using the rolled-and-welded method, expect 8–12 weeks of fabrication and 4–6 weeks of on-site erection. For a larger 10,000+ tonne silo with bolted construction, fabrication might be 10–14 weeks but erection drops to 3–5 weeks because the panels are pre-coated and pre-drilled. Add 4–6 weeks for engineering and procurement before fabrication starts. Total project timeline from contract signing to mechanical completion: typically 16–24 weeks for a single silo.
Q: What's the expected service life of a properly maintained industrial silo?
A: A well-designed, well-built carbon steel silo with appropriate internal coating should give you 25–35 years of service before major shell replacement is needed. The shell itself rarely fails — it's the ancillaries that drive your maintenance cycle. Galvanized bolted silos in corrosive environments (coastal, high-humidity) can see shell thinning of 0.05–0.1 mm per year. At that rate, a 2mm-thick panel reaches its minimum structural thickness in 15–20 years. Plan for it.
Q: Should I choose a welded or bolted silo for my project?
A: It depends on three things: capacity, timeline, and whether you might need to relocate. Welded silos are generally better for capacities above 3,000 tonnes — the structural continuity of the shell handles the hoop stress better. Bolted silos win on speed of erection and are practical up to about 2,500 tonnes. If your project is in a remote area with limited skilled welders on site, bolted construction can save you 30–40% on erection labor costs. For anything above 5,000 tonnes, I'd push for welded every time.
Need a Silo System That Actually Works on Day One?
At Manxing, we've delivered EPC silo projects across 30+ countries — from 500-tonne fly ash silos to 20,000-tonne clinker storage. We handle engineering, fabrication, erection, and commissioning as a single package. No interface gaps. No finger-pointing.
Tell us your material, capacity, and site conditions. We'll send you a preliminary engineering assessment within 5 working days.