


Janssen Equation Applied to Modern Silo Pressure Calculations
The Janssen equation remains the foundational model for predicting vertical and horizontal pressures in bulk solids silos — first published in 1895, still the starting point for every wall-load calculation we do at Manxing. It gives you the asymptotic pressure profile that most finite-element models still calibrate against. But here's the catch: raw Janssen doesn't account for eccentric discharge, dynamic surge loads, or the pressure spikes you get when aeration systems kick in. That's where modern application diverges from textbook theory.
What Janssen Actually Solves
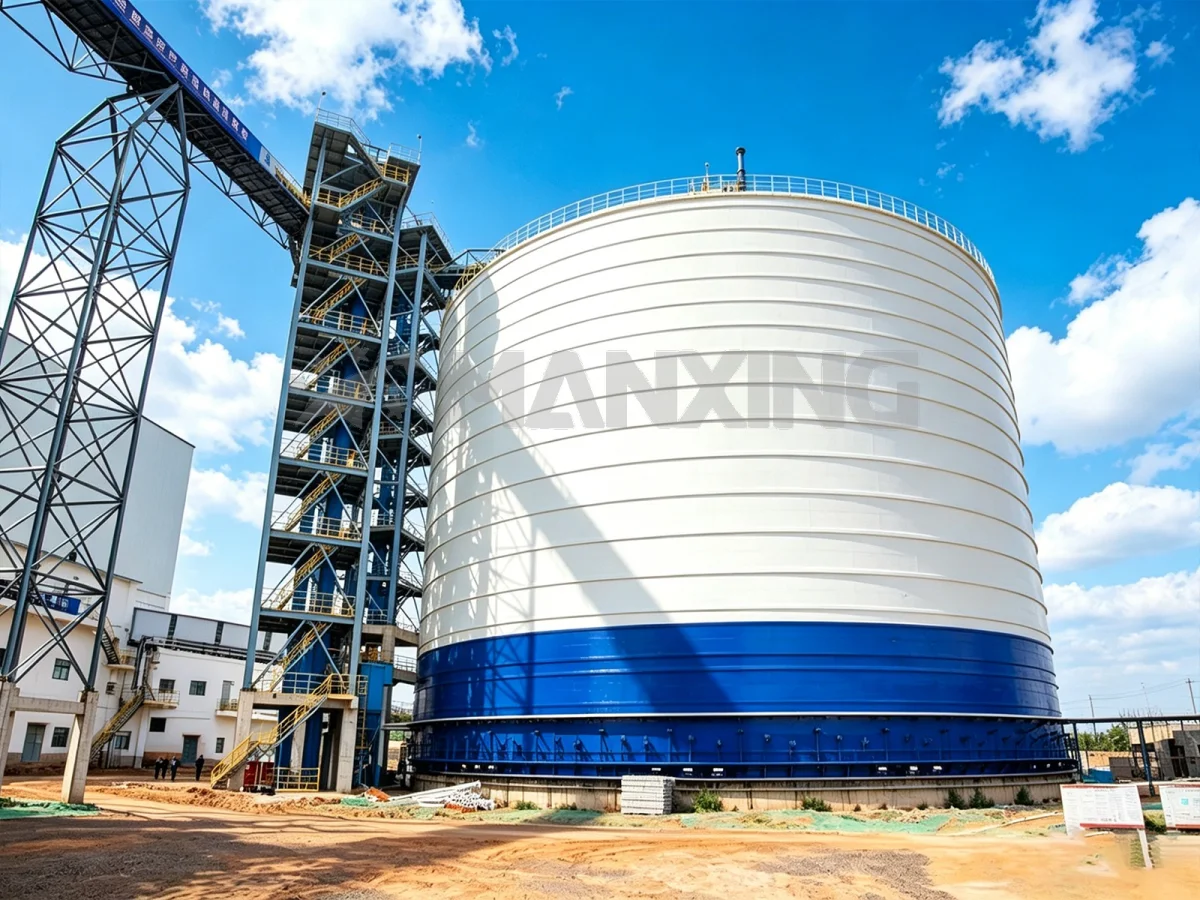
The Core Assumption: Friction Carries the Load
The equation rests on one elegant idea — the weight of stored material is partially supported by wall friction, not just by the bottom footing. As depth increases, pressure at the wall asymptotes toward a maximum value instead of increasing linearly. That's why a 30-meter-tall cement silo doesn't need a base slab rated for 30 meters of hydrostatic head.
The classic form:
P_v = (γ · R) / μ' · K · (1 - e^(-μ'·K·H/R))
Where γ is bulk density, R is hydraulic radius, μ' is wall friction coefficient, K is lateral pressure ratio, and H is fill depth. The exponential term is the whole game — it's what makes silo design possible at scale. Without it, every silo wall would need to be a pressure vessel.
For a typical cement silo — bulk density around 1,200 kg/m³, wall friction coefficient against steel at 0.4 to 0.5, K value of 0.4 to 0.55 — the asymptotic pressure at 25 meters depth lands somewhere around 55 to 70 kPa horizontal. Compare that to hydrostatic: 1,200 × 9.81 × 25 = 294 kPa. The wall friction is doing roughly 75% of the work. That's not a minor correction. That's the difference between a buildable structure and a non-starter.
Where the Equation Breaks Down
Janssen assumes uniform, concentric filling. Static conditions. Constant material properties. A perfectly vertical, rigid wall. If you've stood on a silo site — and I've stood on more than I can count — you know none of those conditions exist in practice.
Eccentric discharge shifts the pressure profile asymmetrically. I watched strain gauges on a 4,000-tonne clinker silo in Indonesia show 40% higher wall stress on one side during offset discharge. Janssen doesn't predict that. You need EN 1991-4 (Eurocode 1, Part 4: Silos and tanks) to handle the patch load cases, and even then, the code's patch load model is a simplification of something messier.
Dynamic effects during filling and emptying create pressure multipliers — 1.5× to 2.0× the Janssen static value during mass flow discharge. Funnel flow is worse in some configurations because of the asymmetric channel. The equation gives you the baseline. The code gives you the load factors. Neither one alone is sufficient.
Modern Application: Janssen as Input, Not Output
Coupling with EN 1991-4 Load Cases
Nobody designs a silo to Janssen alone anymore. The Eurocode framework uses Janssen-derived pressures as the starting point, then applies:
- Patch loads — eccentric discharge modeled as a partial wall pressure over a defined arc (typically 60° to 120° sector)
- Dynamic amplification — discharge pressures multiplied by a factor C (1.0 to 2.0 depending on flow pattern)
- Filling vs. discharge cases — separate load combinations because the pressure distribution differs significantly
For a 10,000-tonne capacity cement silo — say 18 meters diameter, 28 meters straight side — the Janssen horizontal pressure at the wall junction might calculate to 62 kPa. Apply the Eurocode patch load factor of 1.5 for discharge, and you're at 93 kPa on one side. That's the number that drives wall thickness, not the 62.
We've had projects where the client's previous designer used Janssen static pressures without the discharge multiplier. The wall was under-designed by roughly 30%. It didn't fail — the safety factors in the steel grade covered it — but the wall showed visible ovalization at the discharge cone junction. That's not a theoretical concern. That's a 2mm permanent deformation you can measure with a straightedge.
Material Property Sensitivity
The Janssen equation is only as good as your input parameters. And here's where I've seen the most mistakes — people treating bulk density and wall friction as fixed numbers when they're not.
Bulk density of fly ash can vary from 700 kg/m³ (loose, aerated) to 1,100 kg/m³ (compacted, settled). That's a 57% swing. Wall friction against a galvanized steel surface changes with moisture content — I've measured μ' going from 0.35 (dry) to 0.55 (damp) on the same material. The asymptotic pressure changes by a factor of 1.6 depending on which value you plug in.
We always test. Not just look up a table. We run wall friction tests per ASTM D6128 (or the equivalent ISO method) on the actual material the silo will store. On a project in Vietnam storing alumina powder, the supplier's spec sheet said μ' = 0.3. Our test came back at 0.48. That 60% difference changed the wall reinforcement design by two full rebar sizes. The spec sheet was for dry lab conditions. The actual material had 0.3% residual moisture from the calcination process.
Dynamic Pressures: Beyond Static Janssen
Surge Loads During Discharge
When a silo discharges in mass flow, the material accelerates downward as a plug. That acceleration creates a dynamic pressure spike at the wall junction — the transition from cylinder to cone. Janssen doesn't capture this because it assumes static equilibrium.
The dynamic pressure can be estimated as:
P_dyn = P_Janssen × (1 + a/g)
Where a is the material acceleration during discharge. For a high-rate discharge — say 500 tonnes/hour of cement from a 15-meter diameter silo — the acceleration at the cone junction can reach 0.3g to 0.5g. That's a 30% to 50% pressure increase on top of the Janssen value, concentrated at the most highly stressed part of the structure.
This is why the wall-to-cone junction is where we see the most fatigue cracking over a silo's service life. Not the mid-wall. Not the top. The junction. Every time the silo cycles, that joint sees a pressure pulse. After 50,000 cycles — which a plant running two shifts hits in about 8 years — you're in fatigue territory if the detail wasn't designed for it.
Pneumatic Conveying and Internal Pressurization
Here's something Janssen never anticipated: silos that are filled by pneumatic conveying systems operating at 0.3 to 0.5 bar gauge pressure. The internal pressure acts on the full cross-section, not just the walls. For a 12-meter diameter silo, 0.4 bar internal pressure generates a net upward force on the roof of roughly 450 kN. That's 45 tonnes trying to lift the roof off.
We had a call from a plant in Shandong — 2am, baghouse differential pressure had crept to 1,800 Pa and the silo's pressure relief valve was stuck. The roof was visibly bulging. We talked them through isolating the pneumatic line and manually venting through the top hatch. The roof recovered. But the permanent deformation was 15mm at center. That silo needed a roof rebuild six months later.
The lesson: Janssen pressures are lateral. Pneumatic pressures are omnidirectional. You need both in your load case matrix.
Case Study: 8,000-Tonne Fly Ash Silo — Jakarta, Indonesia
Project parameters: 8,000-tonne capacity, 16m diameter × 30m straight side, welded steel construction, mass flow discharge at 350 tonnes/hour. Material: Class F fly ash, bulk density 950 kg/m³ (design basis), wall friction coefficient 0.42 (tested).
Janssen baseline: Horizontal pressure at wall junction = 58 kPa. Vertical pressure at base = 92 kPa.
EN 1991-4 load cases applied:
- Filling (concentric): 1.0 × Janssen = 58 kPa horizontal
- Discharge (eccentric, patch load): 1.5 × Janssen over 90° arc = 87 kPa horizontal on loaded side
- Dynamic amplification at cone junction: 1.3 × Janssen = 75 kPa horizontal
Design outcome: Wall thickness varied from 8mm at top to 14mm at the cone junction, with a 20mm thick transition ring at the wall-to-cone weld. Reinforcement: external stiffeners at 2.4m vertical spacing, designed for the patch load case. Foundation: ring beam rated for 180 kN/m radial load (governed by the eccentric discharge case, not the concentric one).
What we got wrong initially: The first design iteration used a wall friction coefficient of 0.35 from a generic reference table. The actual tested value was 0.42. Higher friction means more load carried by the walls, less transmitted to the base — which sounds good until you realize the wall itself is now carrying more. We had to add two stiffener rings and increase wall thickness by 1mm in the lower third. The client's material test cost $2,400. The redesign cost us three days of engineering time. Worth it.
The silo was commissioned in March 2023. Strain gauge monitoring during the first fill cycle showed wall stresses within 8% of our calculated values. That's about as close as you get in this business.
Common Mistakes in Janssen Application
Using Hydrostatic Pressure Instead of Bulk Density
This one still happens. Someone calculates pressure as ρ × g × h using the particle density (e.g., 3,100 kg/m³ for cement clinker) instead of the bulk density (1,200 kg/m³). The result is 2.6× too high. The silo gets over-designed, which is wasteful but not dangerous. The reverse mistake — using bulk density where you should account for compaction — is the dangerous one.
Ignoring the Silo Aspect Ratio
Janssen was derived for deep silos (H/D > 1.5). For squat silos — H/D < 1.0 — the asymptotic behavior doesn't fully develop, and the pressure profile is closer to hydrostatic. A 6-meter-tall, 8-meter-diameter day bin storing 200 tonnes of sand doesn't behave like a Janssen silo. The friction doesn't have enough height to develop. We've seen designers apply full Janssen to squat bins and under-predict base pressure by 20% to 30%.
EN 1991-4 addresses this with separate rules for slender, intermediate, and squat silos. The classification matters. Get it wrong and your base cone is either over-designed by 40% or under-designed by 25%. Neither is acceptable.
Frequently Asked Questions
Is the Janssen equation still relevant for modern silo design?
Absolutely. It's the theoretical foundation that every modern code builds on. EN 1991-4, ACI 313 (concrete silos), and the Chinese GB 50077 code all use Janssen-derived pressure profiles as their baseline. The equation itself hasn't changed since 1895. What's changed is how we apply load factors, dynamic multipliers, and eccentricity corrections on top of it. Think of Janssen as the skeleton — the codes add the muscle and skin.
How accurate is the Janssen equation compared to actual measurements?
For concentric filling in a well-constructed silo, measured wall pressures typically fall within 10% to 15% of Janssen predictions — assuming you've used correct material properties. During discharge, the deviation grows to 20% to 40% because of dynamic effects the equation doesn't model. That's why we don't design to Janssen alone. We design to Janssen × load factors, and we verify with strain monitoring during commissioning.
Can I use Janssen for non-circular silos?
Yes, with the hydraulic radius substitution. For a rectangular silo, R = (cross-sectional area) / (perimeter). The equation works because it's fundamentally a force balance on a differential slice — the shape enters only through the area-to-perimeter ratio. For a 4m × 4m square silo, R = 1.0m. For a 5.6m diameter circular silo with the same cross-sectional area, R = 1.4m. The circular silo develops lower wall pressure for the same stored volume because of the smaller perimeter-to-area ratio. That's one reason circular silos dominate industrial applications.
Designing a Silo? Let's Get the Pressures Right.
At Manxing, we've delivered EPC silo projects across 30+ countries — cement, clinker, fly ash, coal, slag, and more. Every design starts with tested material properties and a load case matrix that goes well beyond textbook Janssen. We handle engineering, fabrication, and commissioning under one contract.
Contact our engineering team: manxingstorage.com — send us your material specs and capacity requirements. We'll respond with a preliminary pressure analysis within 48 hours.