


Thermal Expansion Design for Industrial Silos: What Every EPC Contractor Gets Wrong
Thermal expansion in industrial silos causes structural failure when temperature differentials exceed 40°C between shell sections — and most designers only check ambient conditions, not material temperatures. The fix isn't complicated: you need sliding anchor bolts, expansion joints at roof junctions, and a shell design that accounts for radial growth of 15–30 mm on a 20-metre diameter silo. Here's how we actually do it.
1. Why Thermal Expansion Breaks Silos (The Physics Nobody Wants to Talk About)
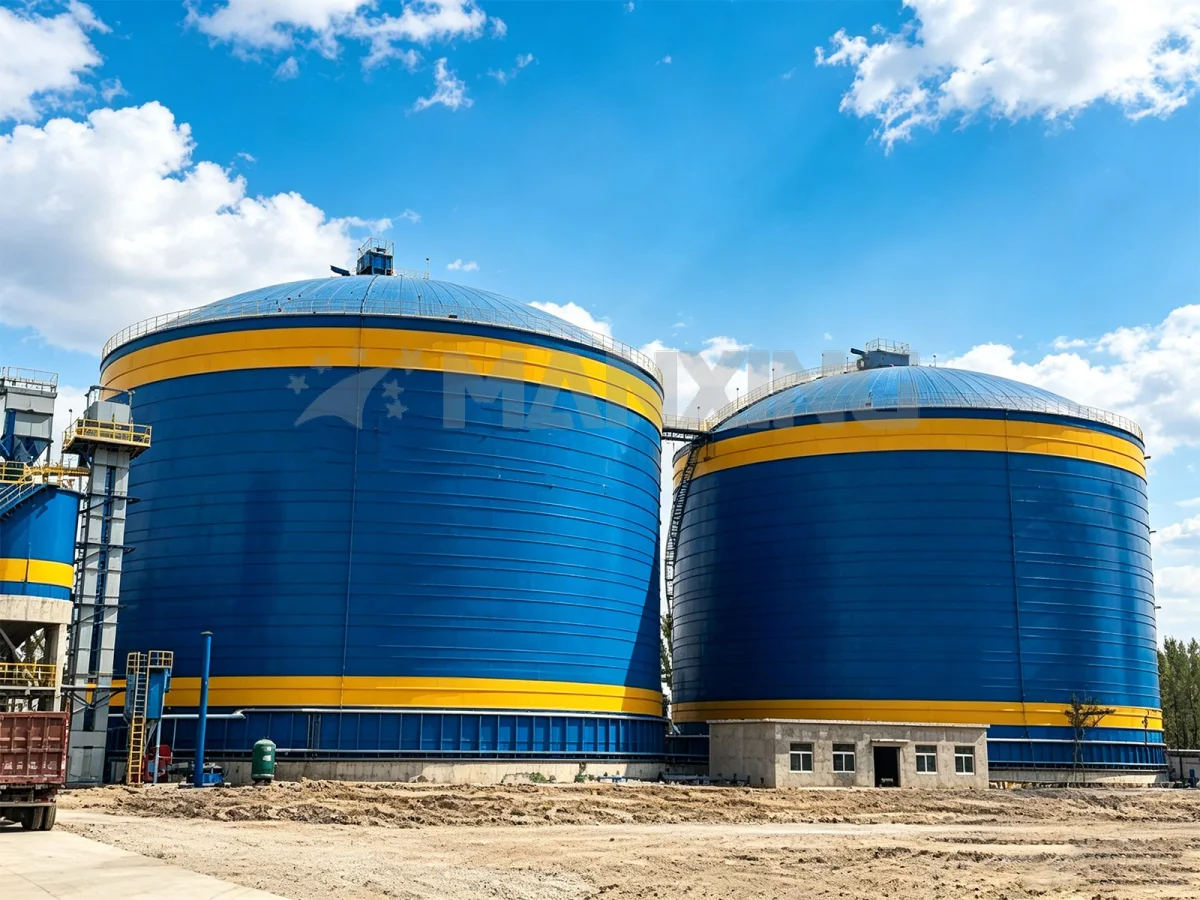
1.1 The Numbers That Matter
Steel expands at roughly 12 × 10⁻⁶ per °C. That sounds trivial until you run it against a real silo. A 30-metre-tall carbon steel shell sitting in direct sun on one side and shade on the other develops a temperature gradient of 35–50°C across its diameter. On a 25-metre diameter silo, that gradient produces a differential radial expansion of 8–15 mm between the hot and cold faces.
Now multiply that by the stiffness of a welded steel shell with 12 mm wall thickness. You're looking at hoop stresses of 80–120 MPa purely from thermal gradient — before you've added a single tonne of cement. I've seen shell buckling that started exactly this way: nobody checked the solar gradient, only the ambient air temperature.
For concrete silos, the coefficient is lower — about 10 × 10⁻⁶ per °C — but the problem is worse because concrete can't yield. It cracks. A 40-metre-tall concrete silo storing clinker at 150°C will see the inner wall expand while the outer face stays cool. The resulting tensile stress on the outer face exceeds 3.5 MPa easily. Standard C30/37 concrete cracks at 2.8 MPa tensile strength. Do the math.
1.2 Where the Damage Actually Happens
Three locations, every time. First: the roof-to-shell junction. The roof structure heats up faster than the shell because it's thinner steel and has no material mass insulating it. On a 20-metre diameter silo, the roof can expand radially by 20 mm while the shell top only moves 8 mm. That 12 mm difference tears roof stiffeners off their welds. I've watched it happen on a fly ash silo in Vietnam — the roof started leaking within 14 months of commissioning.
Second: the anchor bolts. Rigid anchors don't allow the shell base to slide. When the shell expands, it pushes against the concrete foundation with enough force to shear M30 bolts. We replaced 24 anchor bolts on a slag silo in Shandong after two years. The plant manager told me they'd "never had this problem before." They'd never stored material above 80°C before either.
Third: the hopper. The hopper sees the highest material temperatures — clinker at 150–200°C, hot fly ash at 120°C. The hopper wall expands downward and outward, but it's constrained by the supporting structure. The result is plastic deformation at the hopper-to-support junction. Once you get permanent deformation, the hopper geometry changes, flow patterns shift, and you get rat-holing or bridging. The silo doesn't fail catastrophically — it just stops working properly.
2. Design Approaches That Actually Work
2.1 Expansion Joints and Sliding Connections
The roof-to-shell junction needs a sliding connection. The simplest version: a continuous angle ring welded to the shell top, with the roof structure sitting on PTFE slide plates. The roof can slide radially by ±30 mm without transferring load to the shell. PTFE has a friction coefficient of 0.05–0.10 against steel, so the sliding resistance is negligible. We use 3 mm thick PTFE sheets with a stainless steel mating surface. Cost is about $15–25 per linear metre of joint. It's not expensive. It's just often forgotten.
For the shell base, we specify slotted anchor bolt holes. The slot length equals the calculated thermal movement plus 20 mm safety margin. On a 20-metre diameter silo with a 50°C temperature swing, that's 12 mm of radial movement, so we use 35 mm slots. The anchor bolt gets a standard nut and washer, but we don't torque it to full specification — we torque to 50% and use a lock nut instead. The shell can slide. The bolt still holds it down against wind uplift.
Some engineers swear by flexible shell designs — thinner walls that can flex with thermal movement. I don't. A thin shell flexes, yes, but it also fatigues. After 500 thermal cycles (and a silo in the Middle East sees that in two years), you get fatigue cracking at the weld toes. We use EN 1993-4-1 for shell design and keep the shell stiff enough to resist thermal buckling, then provide movement joints at the boundaries. Stiff shell, flexible connections. That's the rule.
2.2 Finite Element Analysis vs. Hand Calculations
For silos under 15 metres diameter and 20 metres height, hand calculations per EN 1991-1-5 (thermal actions) and EN 1993-4-1 (shell structures) are sufficient. You calculate the temperature gradient, apply it as a load case, and check the resulting stresses against yield. It takes a day. It's reliable.
Above those dimensions, or when you're storing material above 100°C, we run a full 3D FEA model with thermal-structural coupling. The model includes the shell, roof, hopper, stiffeners, and foundation. We apply the temperature field as a steady-state thermal load, then solve for the structural response. The output gives us the actual stress distribution — not the simplified hoop stress from hand calcs.
I remember a project in Malaysia where the hand calculation said the shell was fine. The FEA showed a local stress concentration of 280 MPa at a stiffener-to-shell junction — 40% above yield. The stiffener was acting as a thermal bridge, creating a local hot spot. We moved the stiffener 200 mm and the stress dropped to 160 MPa. That's the kind of detail you only catch with FEA. The hand calc would have missed it entirely.
FEA cost for a full silo thermal analysis runs $8,000–15,000 depending on complexity. Compare that to the cost of a field repair: $50,000–100,000 for scaffolding, welding, and lost production. The math works.
3. Material Selection Under Thermal Load
3.1 Steel Grades and Temperature Limits
Standard S235 and S275 carbon steel lose strength above 150°C. At 200°C, S275 retains about 90% of its room-temperature yield strength. At 300°C, it's down to 75%. For silos storing hot clinker or slag, we switch to S355J2 — it holds strength better at temperature and has better toughness.
Above 400°C, you need heat-resistant steel. We've used 16Mo3 (1.5415) for fly ash silos where the material temperature hits 350°C during upset conditions. 16Mo3 is a chromium-molybdenum steel with good creep resistance up to 500°C. It costs about 30% more than S355, but it doesn't lose strength the way carbon steel does.
Stainless steel is rarely justified for the full shell — the cost premium is 3–4× carbon steel. But we use 304L or 316L stainless for the inner liner in concrete silos storing abrasive, hot material. The liner takes the thermal and abrasive load, the concrete takes the structural load. A 6 mm stainless liner inside a 250 mm concrete shell gives you 20+ years of service life. We did this on a alumina silo in Qatar — the plant operator told me after 8 years the liner still looked new.
3.2 Concrete Silos — The Creep Problem
Concrete creeps under sustained load, and creep accelerates with temperature. At 60°C, concrete creep is about 1.5× the room-temperature rate. At 100°C, it's 2.5×. For a concrete silo storing hot material, the long-term deflection can be 2–3× the elastic deflection calculated from standard formulas.
We account for this by increasing the reinforcement ratio by 15–25% in the temperature-affected zone (the bottom 40% of the shell height, where material temperature is highest). We also specify low-heat cement for the shell concrete to minimize thermal cracking during curing. A 40-metre-tall concrete shell pours in 2-metre lifts, and we limit the temperature rise to 20°C above ambient during hydration. That means we pour at night in hot climates — I've been on site at 3am in Saudi Arabia watching concrete trucks arrive because the daytime temperature was 48°C and we couldn't risk a thermal crack.
Post-tensioned concrete silos handle thermal loads better than reinforced concrete because the pre-compression offsets the tensile thermal stress. We use 15.7 mm strand tendons (ASTM A416 Grade 270) with a pre-compression of 3–5 MPa in the hoop direction. That's enough to keep the shell in compression even with a 50°C thermal gradient. The cost premium is about 20% over conventional reinforced concrete, but the service life is 50+ years with minimal maintenance.
4. Real-World Failure Modes and How to Avoid Them
4.1 The Roof-to-Shell Junction
This is the single most common thermal failure point. The roof structure — usually a cone or dome made of 6–8 mm steel plate with radial stiffeners — heats up faster than the shell. On a sunny day in the Middle East, the roof surface temperature hits 70°C while the shell top is at 45°C. The roof expands radially by 18 mm on a 20-metre diameter silo. The shell top expands by 10 mm. The 8 mm differential has to go somewhere.
If the roof is rigidly welded to the shell, the differential movement creates a bending moment at the junction. The shell top deforms outward, the roof stiffeners buckle, or the weld cracks. We've seen all three. The fix is a sliding roof connection with PTFE bearings, plus a flexible seal (usually EPDM rubber) to keep rain and dust out. The seal accommodates ±40 mm of movement and lasts 10–15 years before replacement.
On a cement silo project in Indonesia, the original design had a rigid roof connection. Within 18 months, the roof-to-shell weld cracked along 30% of the circumference. Rainwater entered, contaminated 500 tonnes of cement, and the plant had to shut down for a week to repair. The repair cost $45,000. A sliding connection would have cost $3,000 at design stage. That's the kind of ratio that keeps me up at night.
4.2 Foundation Anchorage Under Thermal Cycling
Anchor bolts fail in fatigue, not in static load. A silo that cycles between empty and full, or between cold and hot material, sees thermal movement at the base every cycle. Over 10 years, that's 3,000+ cycles. Standard anchor bolts (Grade 8.8, M30) have a fatigue limit of about 50 MPa stress range in the threaded section. If the thermal movement creates a stress range above that, the bolts crack.
We specify anchor bolts with rolled threads (not cut threads) because rolled threads have a 30% higher fatigue strength. We also use heavy hex nuts with a minimum thread engagement of 1.5× bolt diameter. And we use slotted holes in the shell base ring — 35 mm slots for a 20-metre diameter silo — so the shell can slide without loading the bolts in shear.
The foundation itself needs attention too. The top 300 mm of the concrete foundation sees the highest thermal gradient. We specify a minimum reinforcement ratio of 0.3% in the top surface to control cracking. In hot climates, we sometimes apply a 50 mm layer of insulating concrete (vermiculite-based) on top of the foundation to reduce the temperature differential. It costs $2,000–4,000 per silo and eliminates the thermal cracking problem entirely.
5. Standards and Code Requirements
5.1 Eurocode and EN 1991-1-5
EN 1991-1-5 (Thermal Actions) is the European standard for thermal design of structures. It gives you the methodology for calculating temperature profiles and thermal effects. For silos, the key clause is Section 6 — thermal actions for cylindrical shells. It specifies that you must consider the temperature difference between the inner and outer surfaces of the shell, not just the uniform temperature change.
EN 1993-4-1 (Silos) references EN 1991-1-5 and adds specific requirements for shell design under thermal load. Clause 6.3.2.2 says you must check the shell for thermal buckling when the temperature gradient exceeds 20°C. The buckling check uses the temperature gradient as an imperfection-equivalent load. It's a simplified approach, but it works for standard geometries.
For non-standard geometries — conical hoppers, eccentric discharges, silos with internal structures — EN 1993-4-1 requires a numerical analysis. That's where FEA comes in. The standard doesn't prescribe the analysis method, but it does require that you verify the model against known solutions. We always run a validation case on a simple cylinder before applying the model to the actual silo geometry.
5.2 DIN 1055-5 and GB 50009
DIN 1055-5 (German standard for thermal actions) is more conservative than EN 1991-1-5. It assumes a higher temperature gradient — 50°C across the shell wall for uninsulated steel silos in direct sun. If you're designing for a German client or a project with German insurance requirements, you need to use DIN 1055-5. The resulting shell stresses are about 20% higher than EN 1991-1-5, which means thicker walls or more stiffeners.
GB 50009 (Chinese load code for building structures) includes thermal action provisions in Section 9.3. It's less detailed than EN 1991-1-5 — it gives a uniform temperature change but doesn't address thermal gradients across the shell. For Chinese projects, we use GB 50009 for the overall load combination but supplement it with EN 1991-1-5 for the thermal gradient check. The Chinese code is a minimum requirement, not a complete thermal design methodology.
We've also worked with ASME B31.3 for silos that are classified as pressure vessels (pneumatic conveying receivers with operating pressures above 0.5 bar). ASME B31.3 Section 301.3 covers thermal expansion stress and requires that the expansion stress range be limited to the allowable stress range from Appendix A. It's a fatigue-based approach — similar in concept to the anchor bolt fatigue check, but applied to the shell itself.
Case Study: 3,000-Tonne Clinker Silo — Shandong, China
A cement plant in Shandong commissioned a 3,000-tonne clinker silo with a 22-metre diameter and 38-metre height. The clinker temperature at discharge was 180°C. The original design used rigid anchor bolts and a welded roof-to-shell connection. After 18 months of operation, the plant reported three problems: anchor bolt cracking (6 of 32 bolts), roof-to-shell weld leakage, and shell bulging at the 12-metre elevation (the level where hot clinker accumulated during filling).
Our investigation found that the thermal gradient across the shell at the 12-metre level was 65°C — the inner wall was at 150°C from contact with hot clinker, the outer wall was at 85°C from solar radiation. The resulting thermal stress was 145 MPa, exceeding the yield strength of the S275 shell plate. The shell had yielded locally, creating a permanent bulge of 40 mm.
The retrofit included: (1) replacing all 32 anchor bolts with rolled-thread Grade 10.9 bolts in 40 mm slotted holes, (2) cutting the roof-to-shell weld and installing a sliding connection with PTFE bearings, (3) adding external stiffeners at the 12-metre level to reinforce the bulged section, and (4) applying a 25 mm thick ceramic-fibre insulation panel to the outer shell above the 12-metre level to reduce the solar gradient. Total retrofit cost: $78,000. The silo has operated without issues for 4 years since.
FAQ
Q: How much does thermal expansion actually move a silo shell?
For a 20-metre diameter carbon steel silo with a 50°C temperature change, the radial expansion is about 12 mm. The vertical expansion on a 30-metre-tall shell is about 18 mm. These numbers seem small, but they create significant stress when the structure is constrained. The key is not the absolute movement — it's the differential movement between connected components (roof vs. shell, shell vs. foundation).
Q: Do I need to worry about thermal expansion for a silo storing ambient-temperature material?
Yes, if the silo is outdoors and exposed to solar radiation. A steel shell in direct sun develops a 30–50°C temperature gradient between the sun-facing and shaded sides, even if the stored material is at ambient temperature. This gradient causes shell ovality and stress in the roof junction. For indoor silos with no solar exposure and material within 20°C of ambient, thermal effects are usually negligible — but you should still check the anchor bolt detail.
Q: What's the cost premium for a thermal-expansion-ready silo design?
Sliding roof connections add $3,000–8,000 to the silo cost (depending on diameter). Slotted anchor bolt holes add $1,000–2,000. FEA analysis adds $8,000–15,000 to the engineering cost. Total premium is roughly 3–5% of the silo's structural cost. Compare that to a field retrofit: $50,000–100,000 for anchor bolt replacement, roof repair, and production downtime. The design-stage investment pays for itself many times over.
Get Your Thermal Design Right the First Time
At Manxing, we've designed and commissioned silos across 30+ countries — from 500-tonne fly ash silos in Southeast Asia to 10,000-tonne clinker silos in the Middle East. Every design includes thermal expansion analysis as standard, not as an afterthought. We use FEA for large or high-temperature silos, and we specify sliding connections and slotted anchors on every outdoor steel silo we build.
Contact our engineering team for a thermal expansion review of your next silo project. We'll run the numbers, identify the risk points, and give you a design that won't crack, buckle, or leak in the first two years. That's not a promise — it's a calculation.